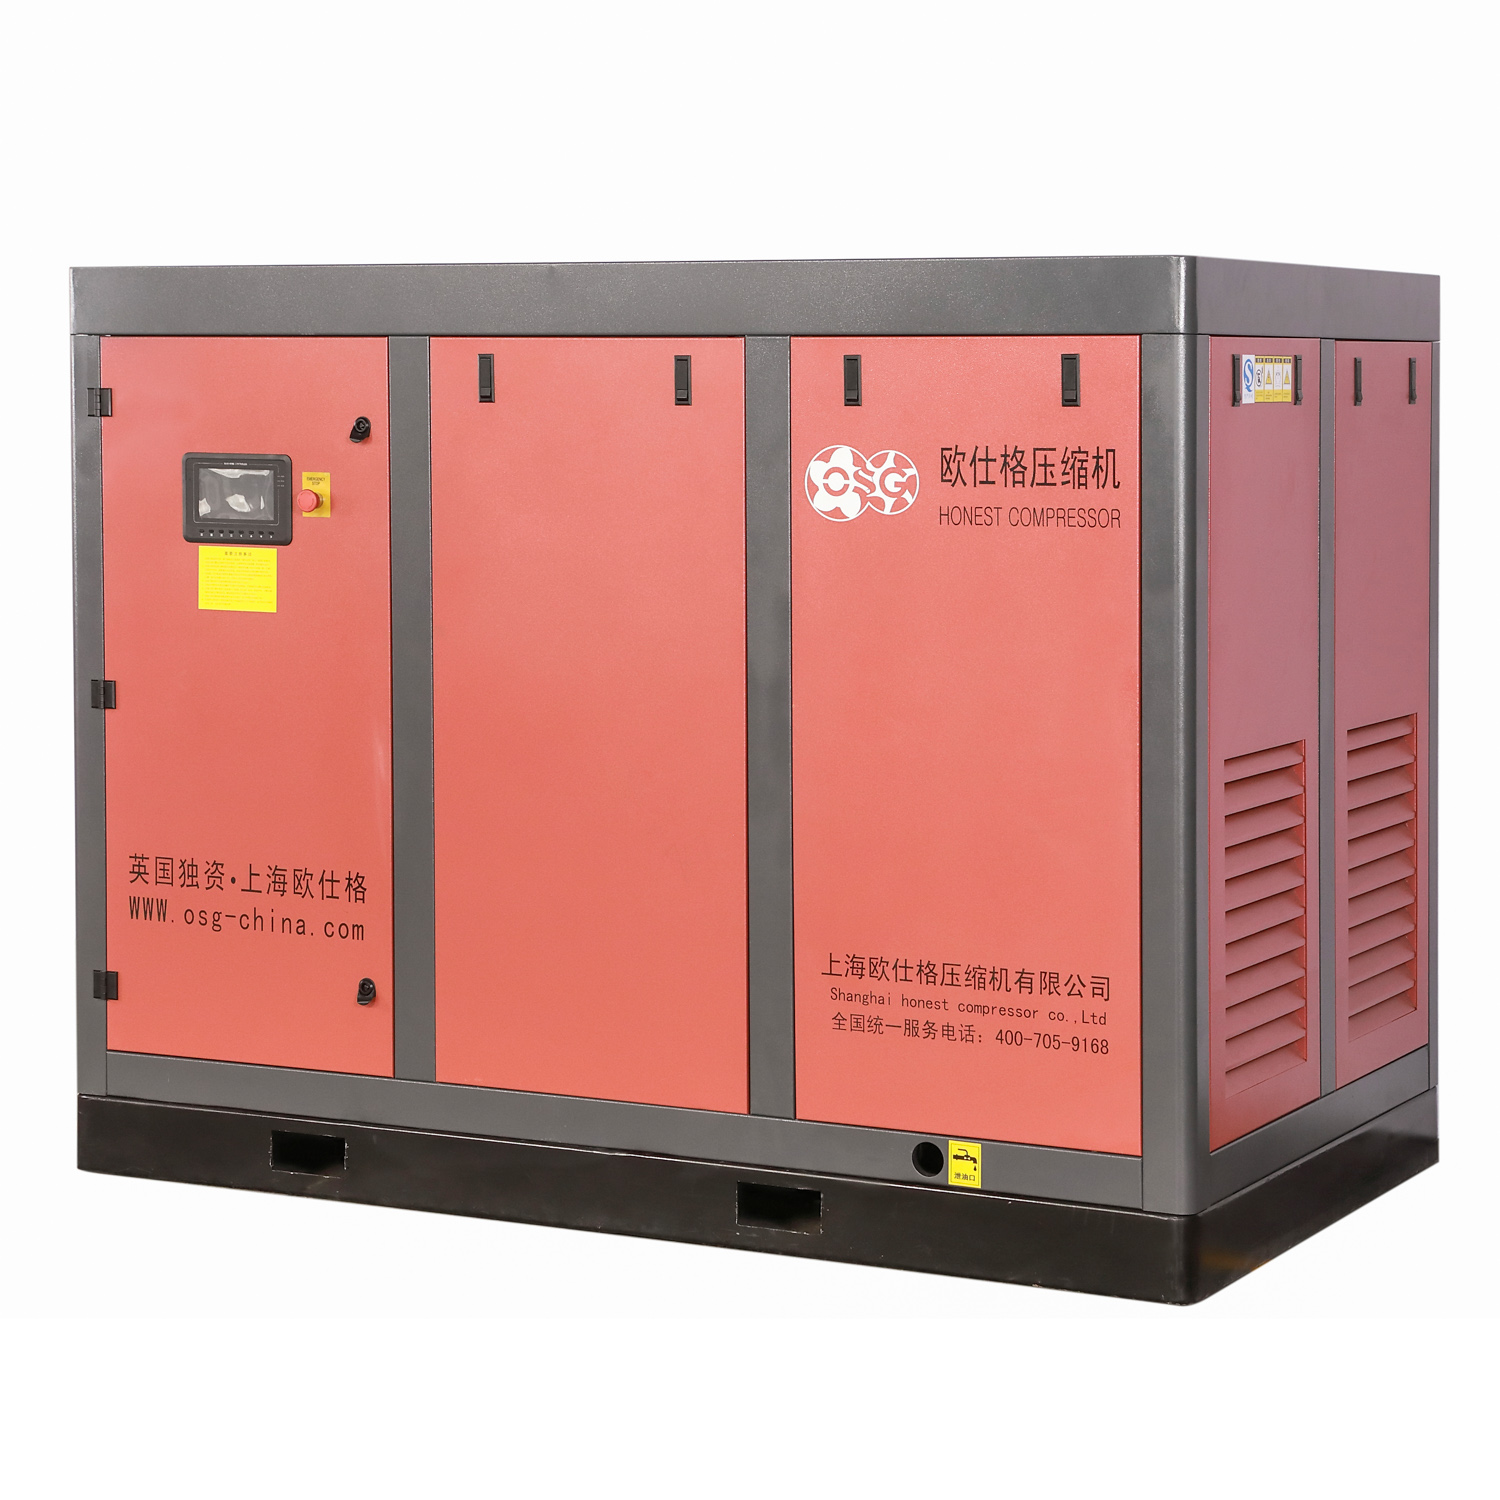
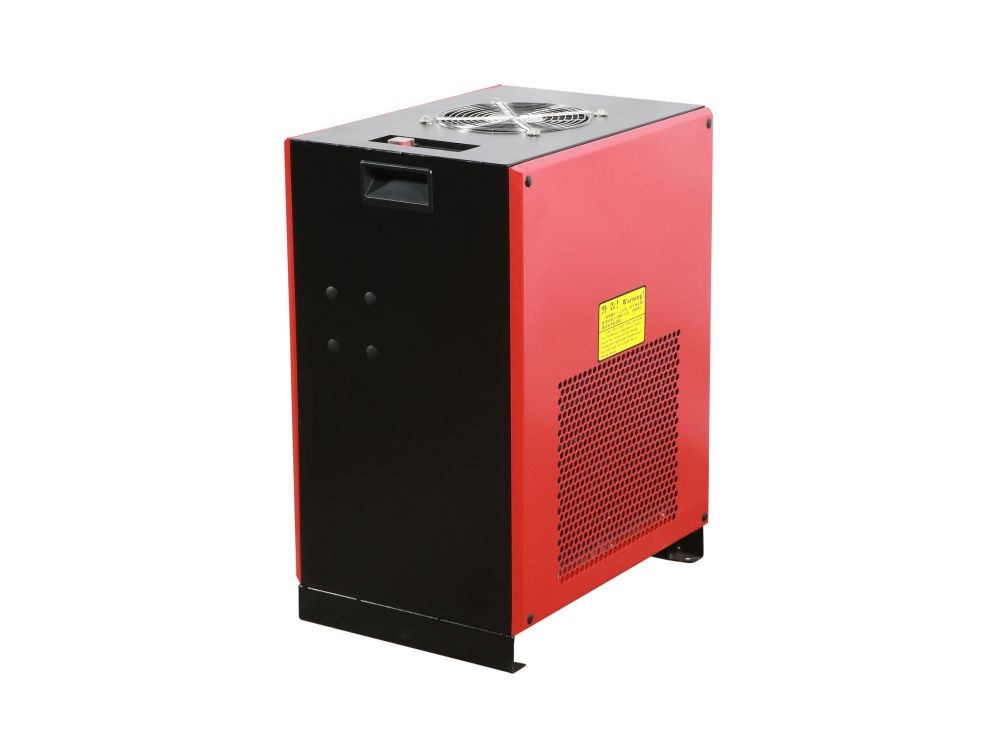
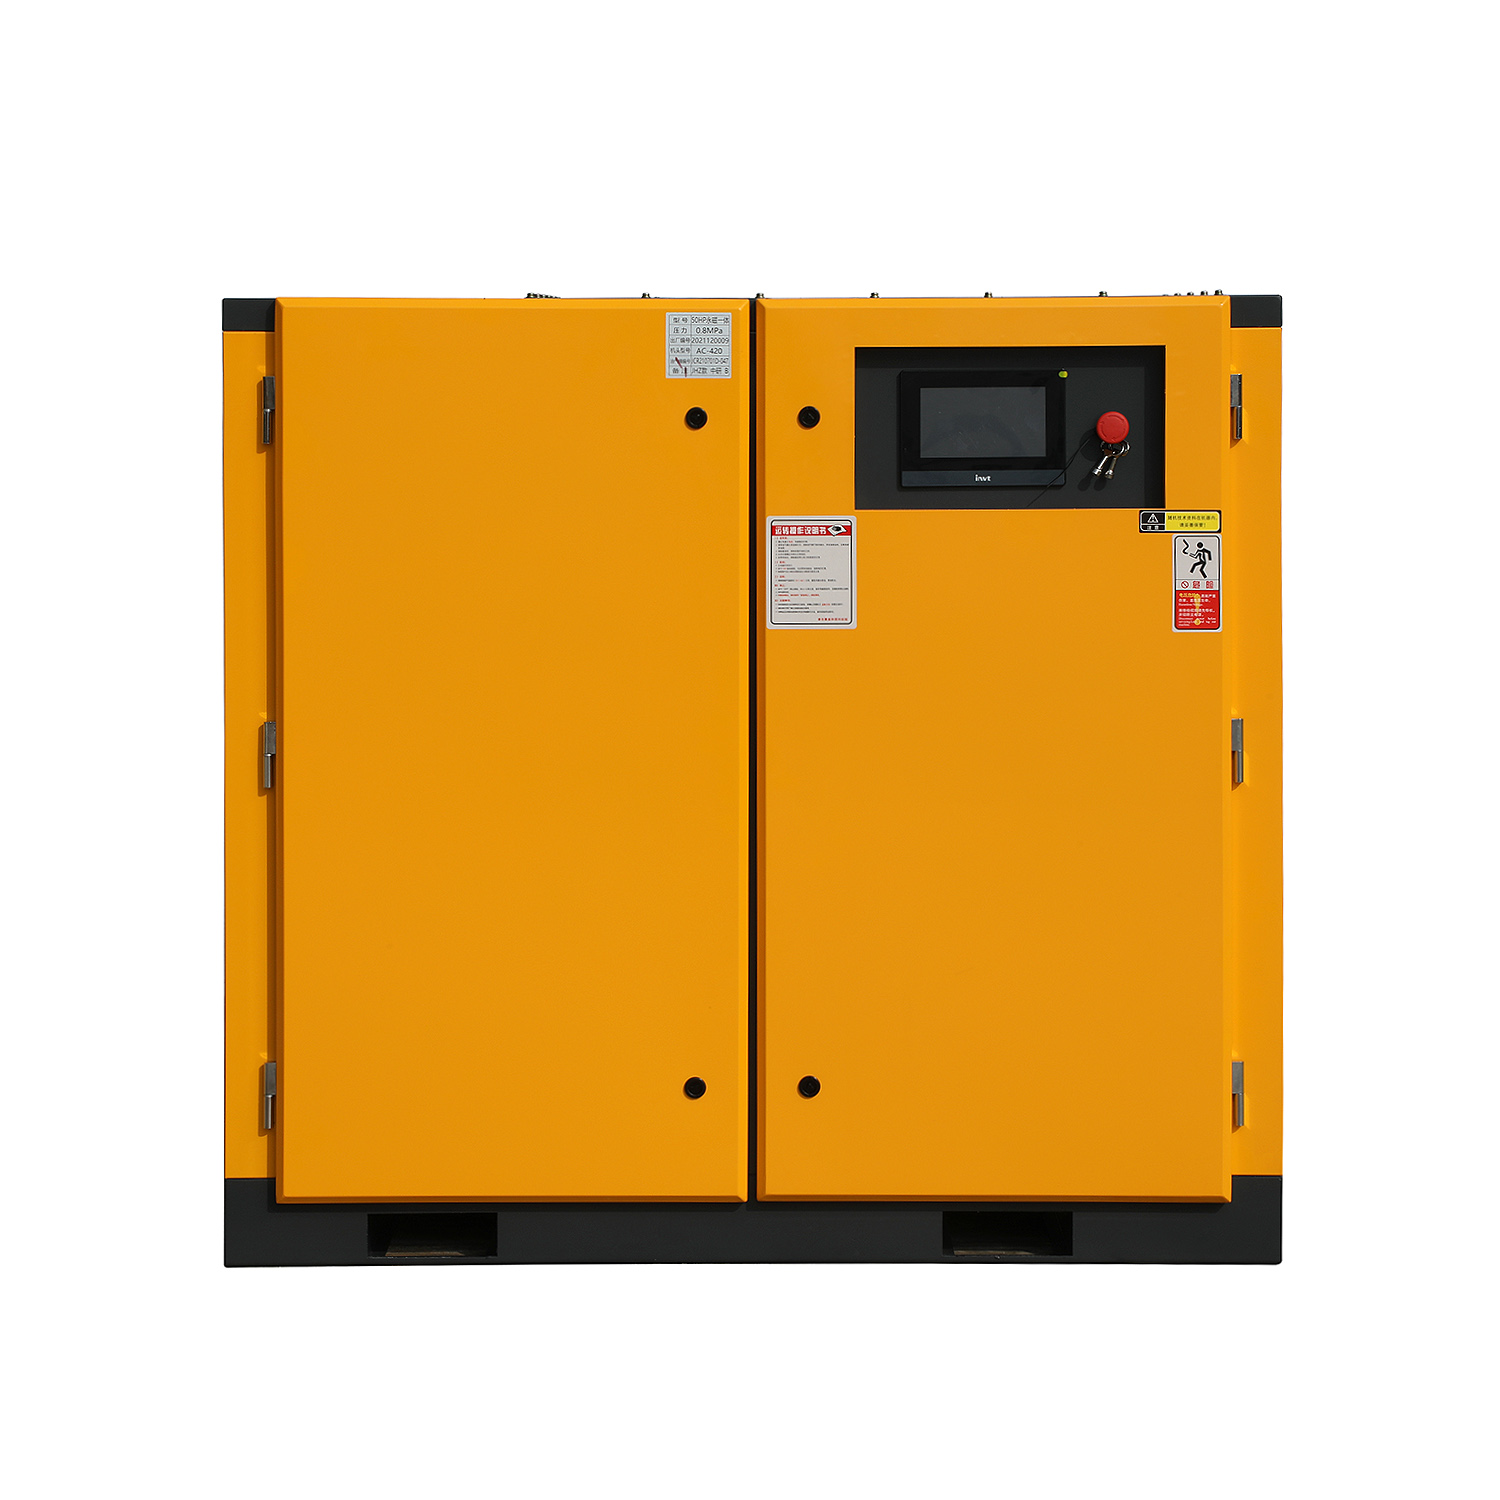
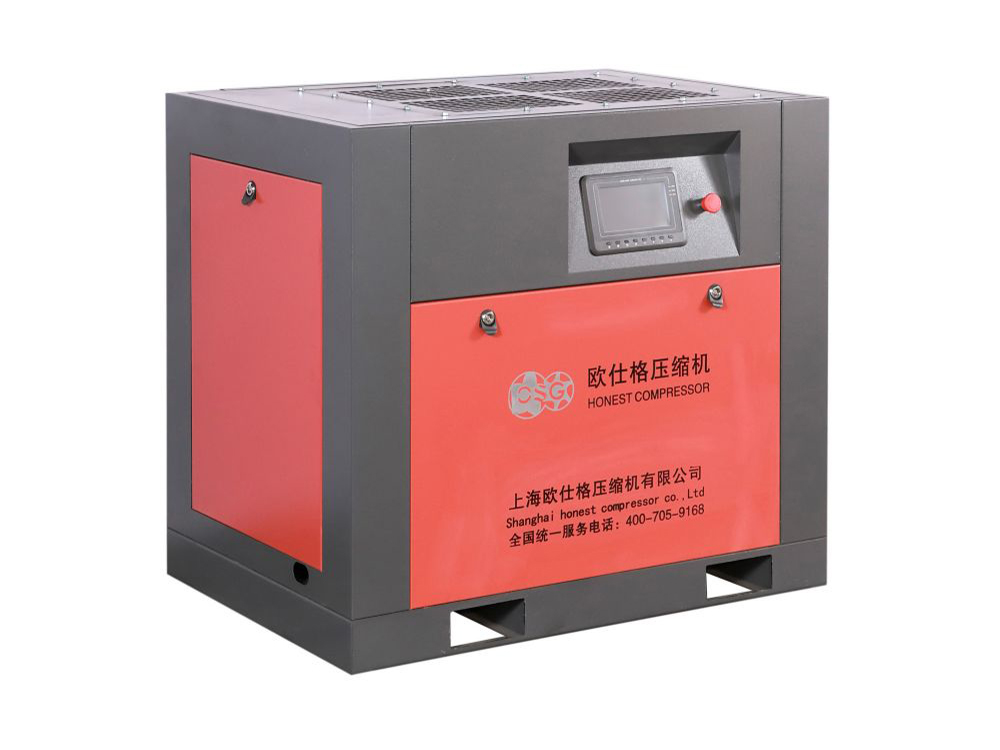
Featured Compression Systems for Chemical & Industrial Operations
High-efficiency rotary screw equipment engineered for optimal gas flow, pressure stability, and corrosion-resistant air distribution in modern chemical manufacturing.
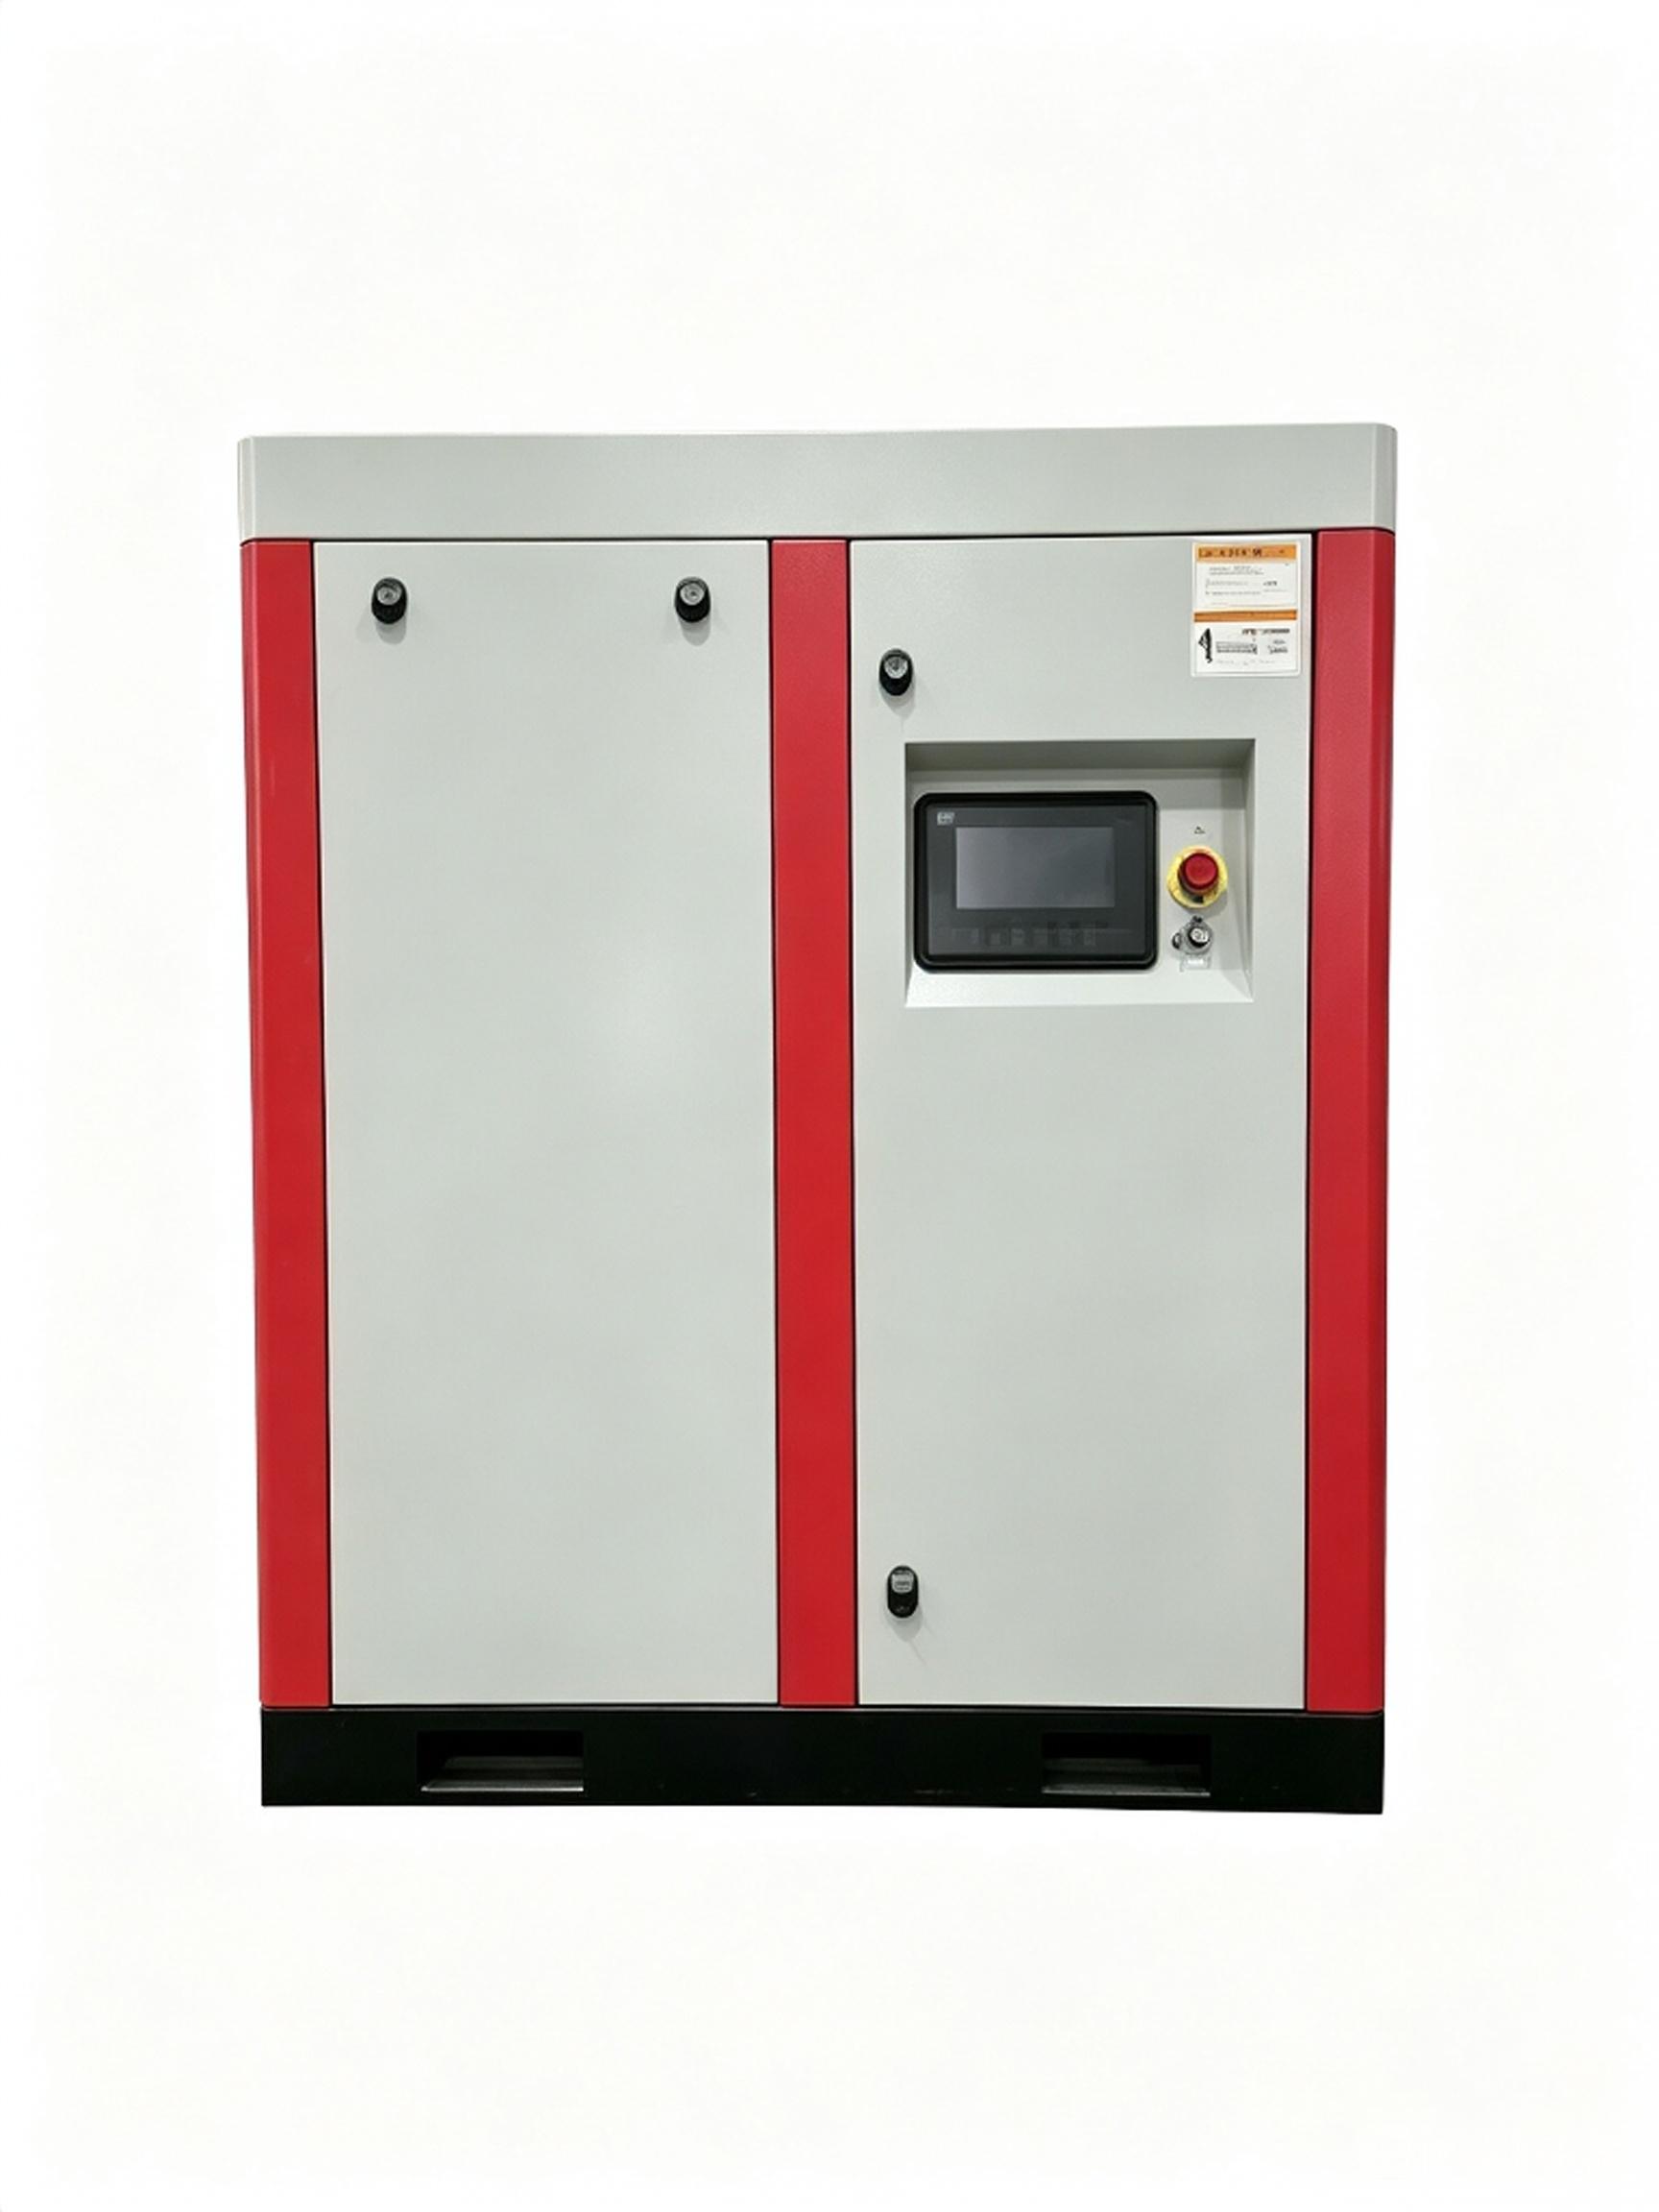
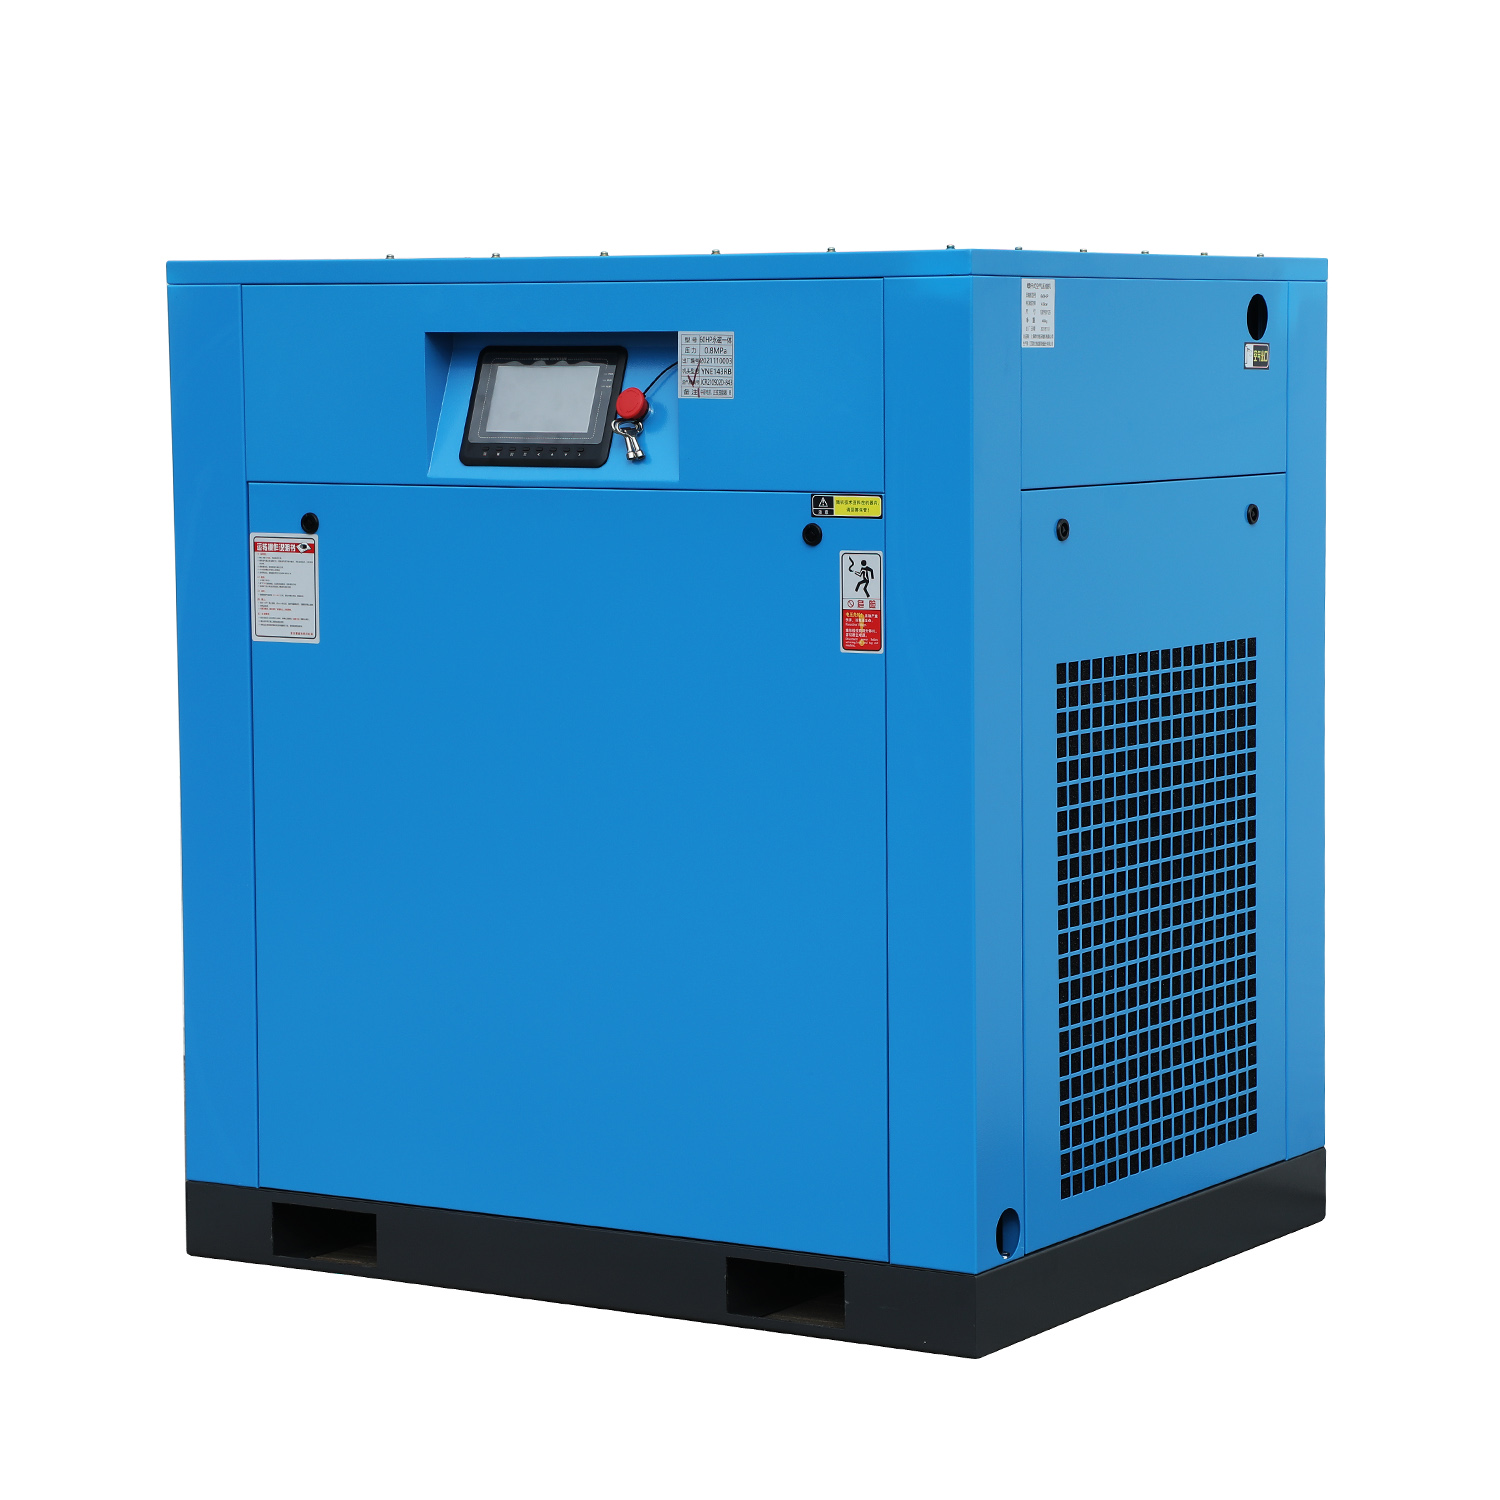
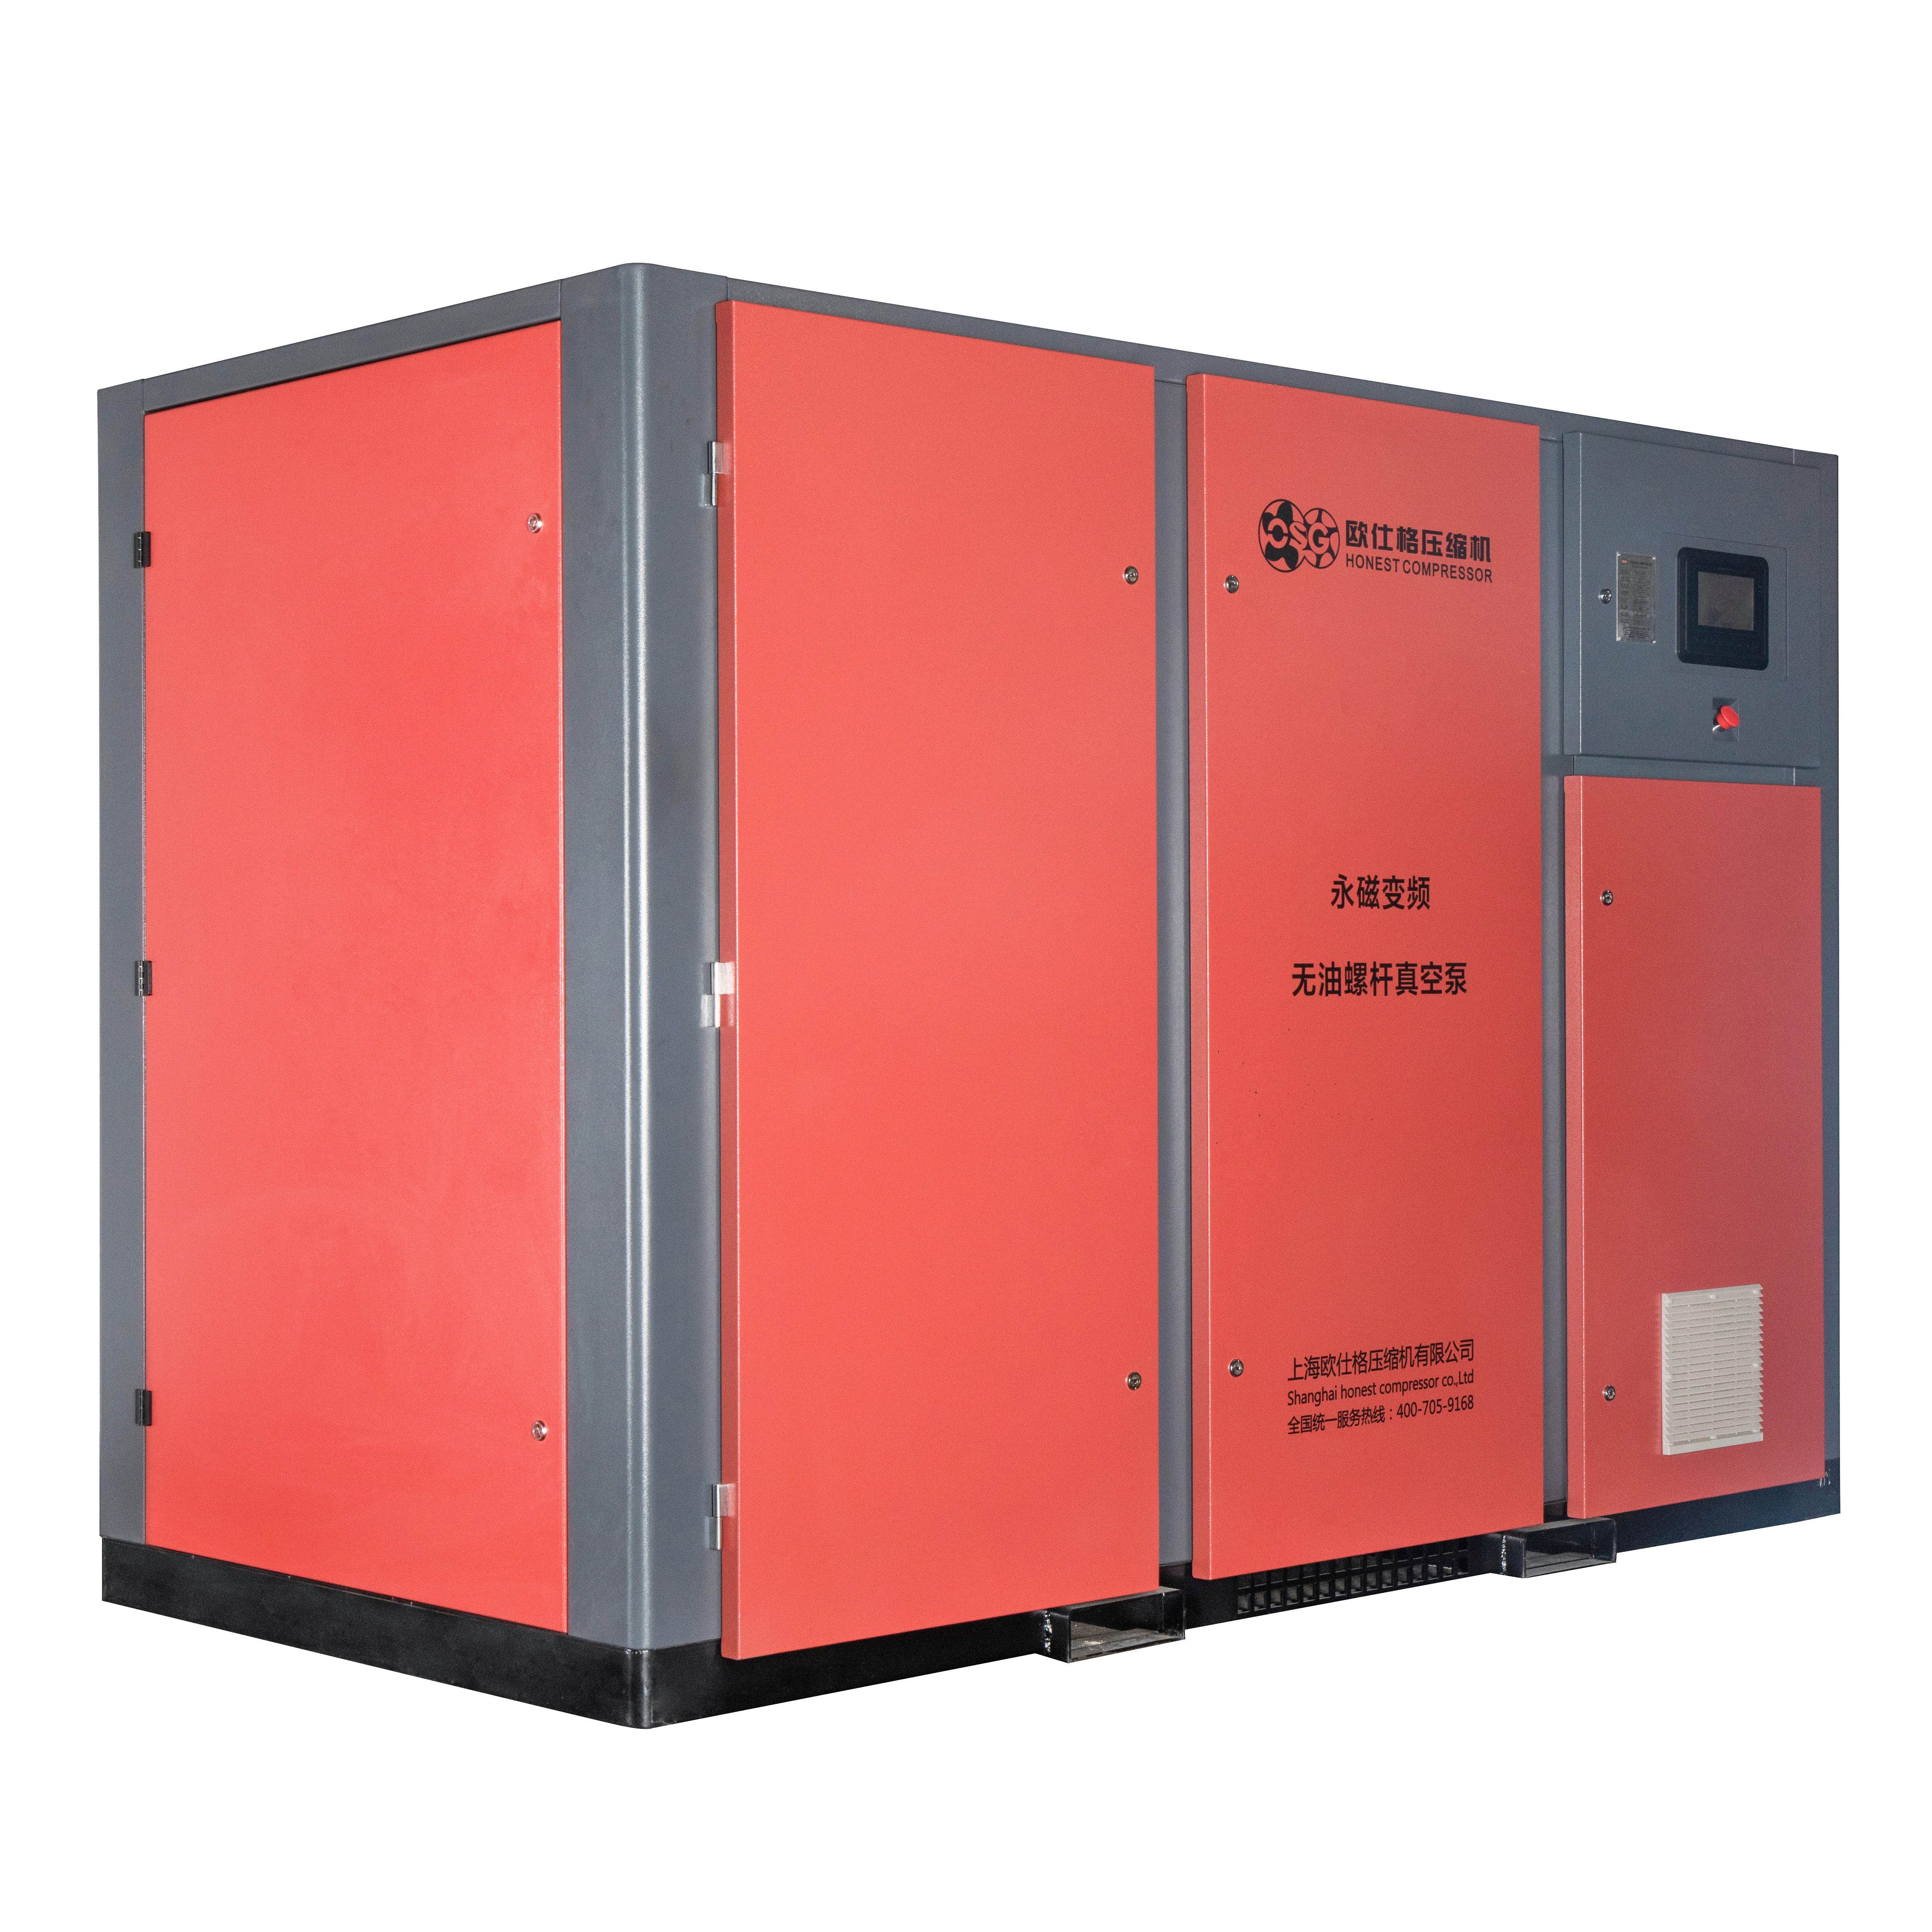
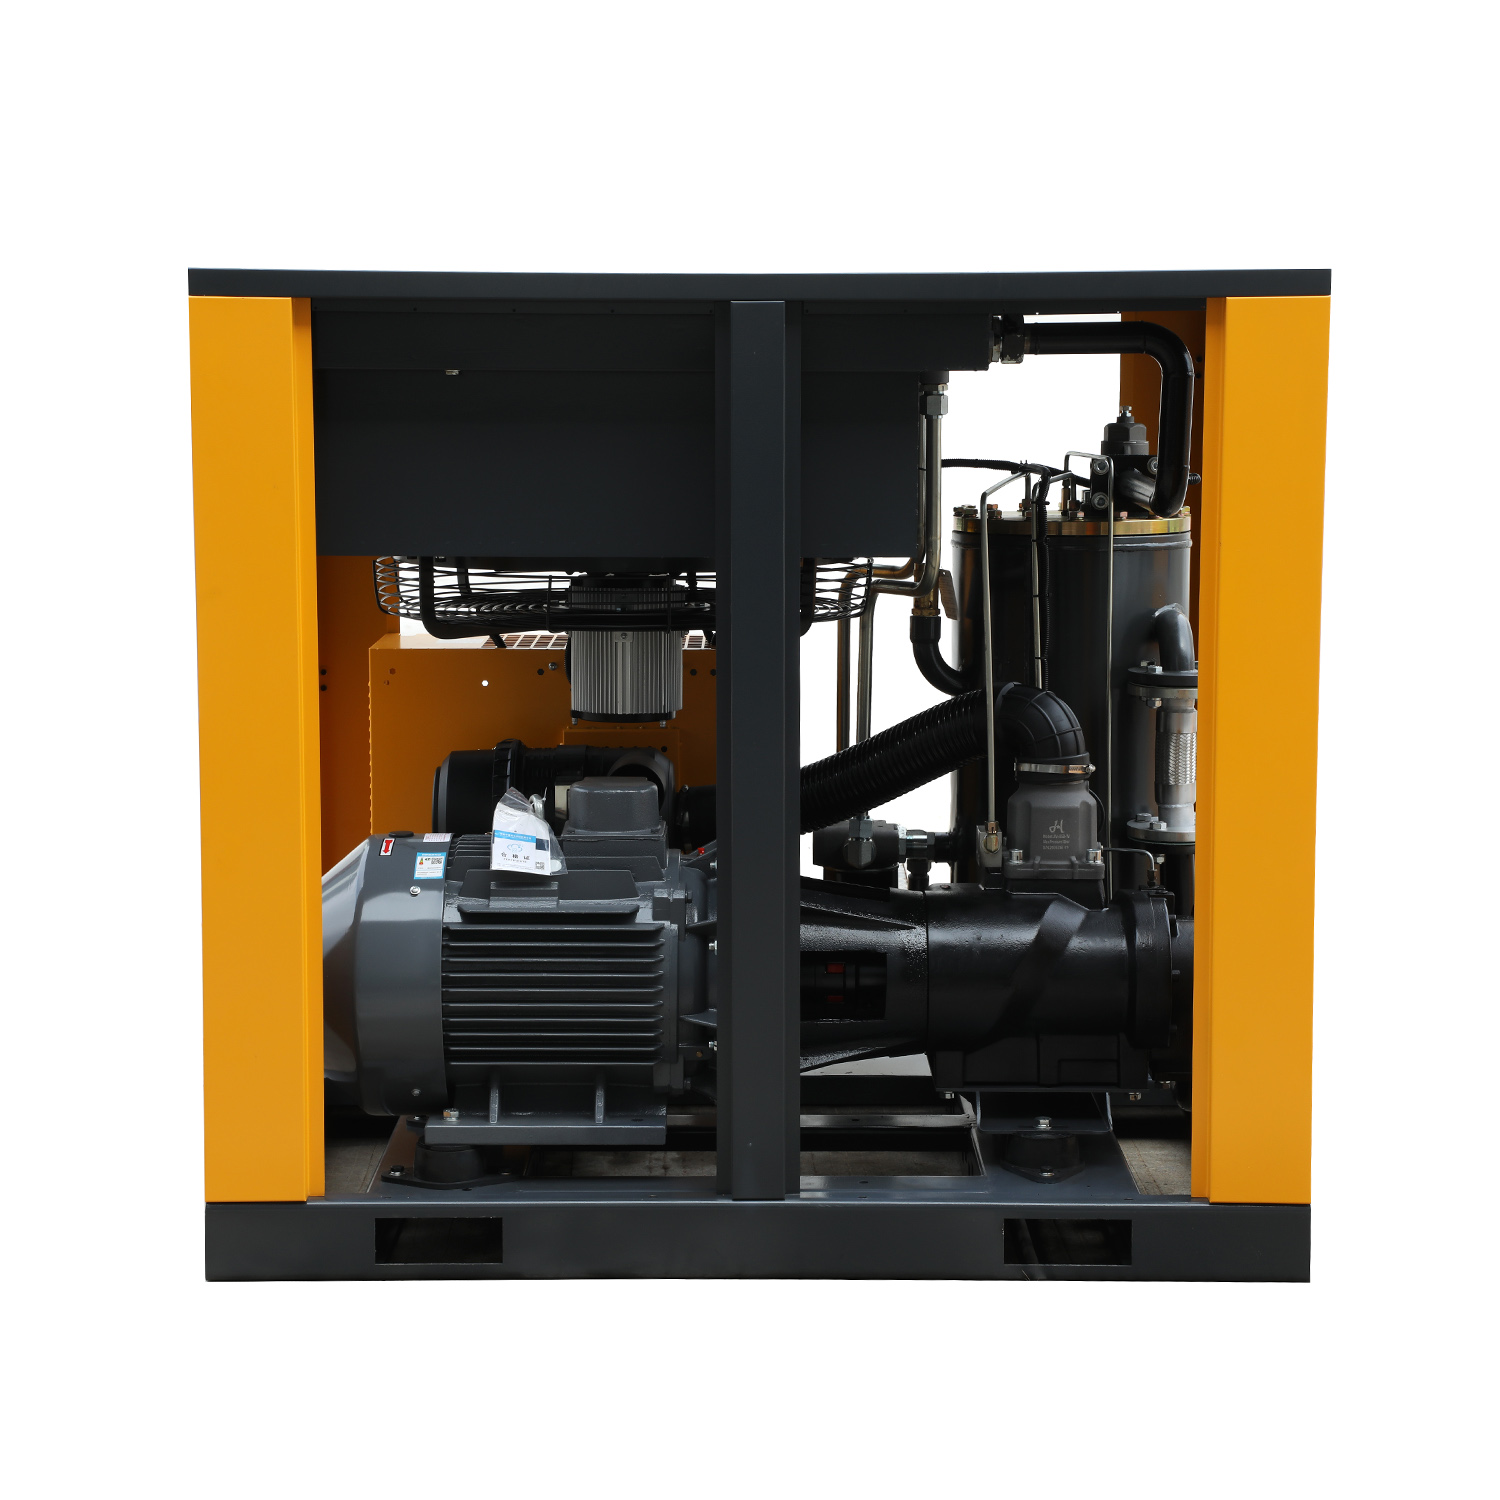
The Vital Role of Oil-Flooded Screw Compressors in Modern Chemical Plants
The chemical and petrochemical processing industry operates under some of the most rigorous operational, environmental, and safety demands in global manufacturing. Compressed air in a chemical production plant is not merely a utility—it is a critical feedstock dynamic, a safety mechanism, and an actuation vector. Within this landscape, the oil flood screw air compressor (also known as oil-injected rotary screw compressor) serves as the unyielding backbone for medium-to-large scale continuous chemical facilities.
Unlike standard commercial manufacturing environments, chemical facilities subject their air compression infrastructure to aggressive atmospheric conditions: acidic vapors, ambient dust, volatile organic compounds (VOCs), fluctuating ambient temperatures, and strict 8,000+ hour yearly run cycles without unplanned downtime. The oil-flooded rotary screw mechanism is uniquely suited to these arduous environments. The controlled injection of specialized synthetic lubricant into the compression chamber performs four indispensable simultaneous functions: positive sealing across the male-female rotor clearances, continuous hydrodynamic lubrication of high-load anti-friction bearings, mechanical damping against vibration, and isothermal heat extraction directly at the point of gas compression.
Technical Advantages & Thermodynamic Superiority in Chemical Synthesis
In petrochemical plants, chlor-alkali units, fine chemical synthesis, and polymer processing factories, energy consumption represents over 70% of the total life-cycle cost of compressed air systems. Oil-flooded screw air compressors achieve higher thermodynamic efficiency through near-isothermal compression. As air is drawn through the heavy-duty inlet filtration stage into the asymmetric twin rotors, the injected lubricant creates an impenetrable hydraulic seal between the rotor lobes and the housing wall. This minimizes internal back-leakage, allowing single-stage compression ratios to exceed 10:1 with outstanding specific power metrics.
Injected fluid acts as an immediate thermal heat sink, keeping air temperatures well below critical polymerization and oxidation thresholds throughout high-pressure duty cycles.
Continuous oil film envelops internal screw profiles, shielding high-tensile alloy rotors against ambient atmospheric chemical moisture, sulfurous traces, and corrosive degradation.
Variable frequency drives dynamically match compressed air delivery with variable batch reactor demands, eliminating idle energy losses and reducing peak startup surges.
Comprehensive Chemical Application Scenarios
Oil-flooded rotary screw air compressors are integrated across a diverse spectrum of unit operations throughout modern organic and inorganic chemical complexes:
1. Pneumatic Conveying of Granular Polymers & Chemical Powders
From high-density polyethylene (HDPE) pellets and PVC resins to titanium dioxide and soda ash, pneumatic conveying systems require reliable, pulse-free air volume. Oil-flooded screw compressors provide continuous pressure curves necessary for dense-phase and dilute-phase air displacement without pulsation, protecting fragile chemical extrusions from pipeline clogging and product attrition.
2. Process Valve Actuation & Plant Safety Automation (ISA-7.0.01 Compliance)
A petrochemical refinery may feature tens of thousands of emergency shutdown valves (ESDs), control diaphragms, and pneumatic positioners. A momentary loss of pneumatic actuation pressure can trip reactors or trigger hazardous containment failures. Oil-flooded compressor installations, equipped with high-efficiency cyclone separators, multi-stage coalescing oil filters, and desiccant dryers, ensure an unbroken supply of pristine, dry instrument air complying with ISO 8573-1 Class 1/2 standard requirements.
3. Reactor Agitation, Sparging & Oxidation Medium
In direct chemical synthesis—such as the production of terephthalic acid, cyclohexanone oxidation, or biological fermentation tanks—compressed air serves as an oxygen carrier. The steady pressure stability of twin-screw compression prevents fluid back-siphonage and guarantees consistent stoichiometry in pressurized reactor columns.
4. Nitrogen Generation & Tank Blanketing Feed Air
To prevent volatile organic solvents from forming explosive vapor mixtures with atmospheric oxygen, chemical storage tanks and centrifuges require high-purity nitrogen blanketing. Oil-flooded screw compressors deliver high-pressure feed air directly into Pressure Swing Adsorption (PSA) or membrane nitrogen separation skids, delivering dependable purge pressures round the clock.
5. Filter Press Dewatering & Slurry Cake Blowing
In specialty chemical pigment manufacturing and wastewater treatment units, heavy membrane filter presses demand rapid, high-volume air surges to squeeze moisture from hazardous chemical cakes. Screw compressors provide sustained flow without the mechanical fatigue typical of reciprocating units under heavy load cycling.
| Process Application | Operational Pressure | Typical Capacity Range | Primary Engineering Objective |
|---|---|---|---|
| Instrument & Actuation Air | 6.0 - 8.5 bar | 2.0 - 45.0 m³/min | Zero dew-point drop, high reliability, fail-safe valve positioning |
| Pneumatic Powder Conveying | 2.5 - 4.5 bar (Low Pressure) | 10.0 - 75.0 m³/min | High flow volume, anti-pulsation, low specific power consumption |
| PSA Nitrogen Separation Skids | 7.5 - 13.0 bar | 5.0 - 60.0 m³/min | Continuous inlet pressure stability for high-purity N2 output |
| Tank Blanketing & Purging | 5.0 - 7.0 bar | 1.5 - 25.0 m³/min | Explosion risk mitigation, atmospheric moisture displacement |
| Chemical Slurry Cake Drying | 7.0 - 10.0 bar | 8.0 - 50.0 m³/min | Rapid pressurization, high moisture displacement efficiency |
Lubricant Chemistry, Separation Technology & Environmental Safety
In chemical production, selecting the appropriate lubricant within an oil-flooded compressor is paramount. Standard mineral oils can degrade when exposed to trace acidic gases or reactive hydrocarbons drawn from ambient air. Leading chemical installations utilize advanced fully synthetic polyalphaolefin (PAO), polyolester (POE), or polyalkylene glycol (PAG) formulations that offer superior thermal stability, extended 8,000-hour oxidation resistance, and hydrolytic stability.
Modern separation systems feature triple-stage separation architecture: a high-efficiency centrifugal cyclonic chamber, a gravitational settling reservoir, and a pleated micro-fiber deep-bed coalescing filter element. This advanced filtration train ensures that residual oil carryover is maintained below 2-3 ppm (w/w) before reaching secondary downstream treatment (adsorption filters and catalytic converters), thereby protecting downstream catalysts, molecular sieves, and chemical batches from cross-contamination.
Energy Efficiency, Heat Recovery & Smart AI Integration in Chemical Facilities
With global chemical plants under strict carbon-reduction mandates and escalating power tariffs, energy efficiency is a primary engineering benchmark. Two significant developments have transformed oil-flooded screw compressors:
- Integrated Waste Heat Recovery (WHR): Up to 85% to 90% of the electrical energy consumed by an oil-flooded compressor is converted into thermal heat within the circulating oil. Modern chemical installations integrate plate heat exchangers into the oil circuit to generate hot water (up to 85°C) for chemical pre-heating, boiler feedwater makeup, or administrative facility heating, delivering significant primary energy savings.
- AI-Driven IoT Monitoring & Predictive Maintenance: Intelligent controllers embedded with vibration sensors, bearing temperature probes, and lubricant differential pressure sensors interface with plant DCS (Distributed Control Systems) via Modbus, Profibus, or Industrial Ethernet. Predictive algorithms forecast filter saturation, detect bearing fatigue before mechanical seizure, and modulate variable-speed drives (VSD) to track batch process demands without wasting unloaded energy.
Shanghai Honest Compressor Co., Ltd.
Global British-owned engineering heritage delivering world-class twin-screw compressed air systems and industrial gas equipment.
Shanghai Honest Compressor Co., Ltd. is a British-owned enterprise founded in early 2004. The modern manufacturing base is situated at NO. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, China. As a premier large-scale manufacturing enterprise specializing in the R&D and production of advanced twin-screw air compressors in China, Honest Compressor has established itself as an authoritative turnkey supplier of comprehensive industrial air and gas system solutions.
We supply diverse industrial categories including piston air compressors (low, medium, high pressure, and oil-free units), complete screw air compressor systems ranging from 3kW to 480kW, gas separation skids, refrigerant compressors, refrigerated air dryers, precision coalescing filters, and advanced ceramic membrane filtration systems, alongside extensive genuine consumables and engineering components.
We fully implement strict management throughout the entire manufacturing process, strictly monitor product quality and environmental protection, and the company has passed ISO9001:2015 Quality Management System certification. In technological R&D, our machines actively integrate structural advantages from international benchmarks while incorporating our proprietary convenient maintenance architecture. Following stringent evaluation by the National Compressor Inspection Center, our energy consumption metrics consistently outperform national energy-saving standards.
With an extensive capacity spectrum spanning 0.5 m³/min to 75 m³/min in both air-cooled and water-cooled formats, we provide permanent magnet variable frequency compressors, oil-free units, diesel/electric mobile compressors, and turnkey compressor station design, EPC installation, technical operator training, and lifetime overhaul hosting.
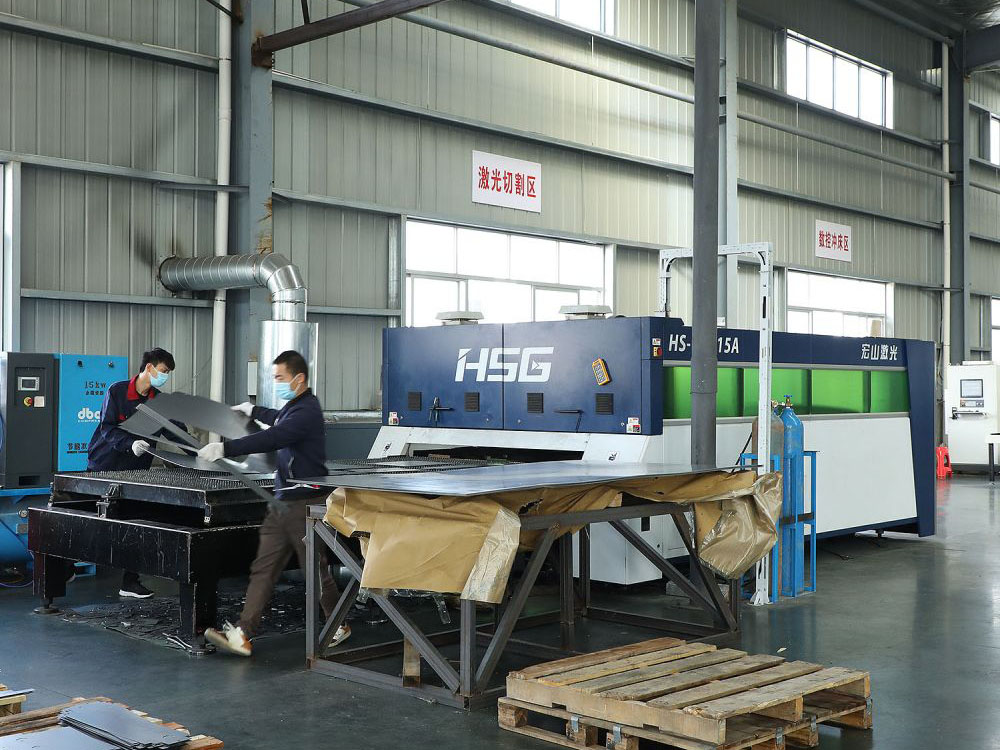
High-Precision Rotor Machining & Assembly Workshop, Jiading District, Shanghai
Comprehensive Chemical-Grade Compression & Purification Equipment
Explore our full line of rotary screw compressors, vacuum solutions, and air treatment systems engineered for maximum chemical reliability.