Featured Conveying Air Solutions
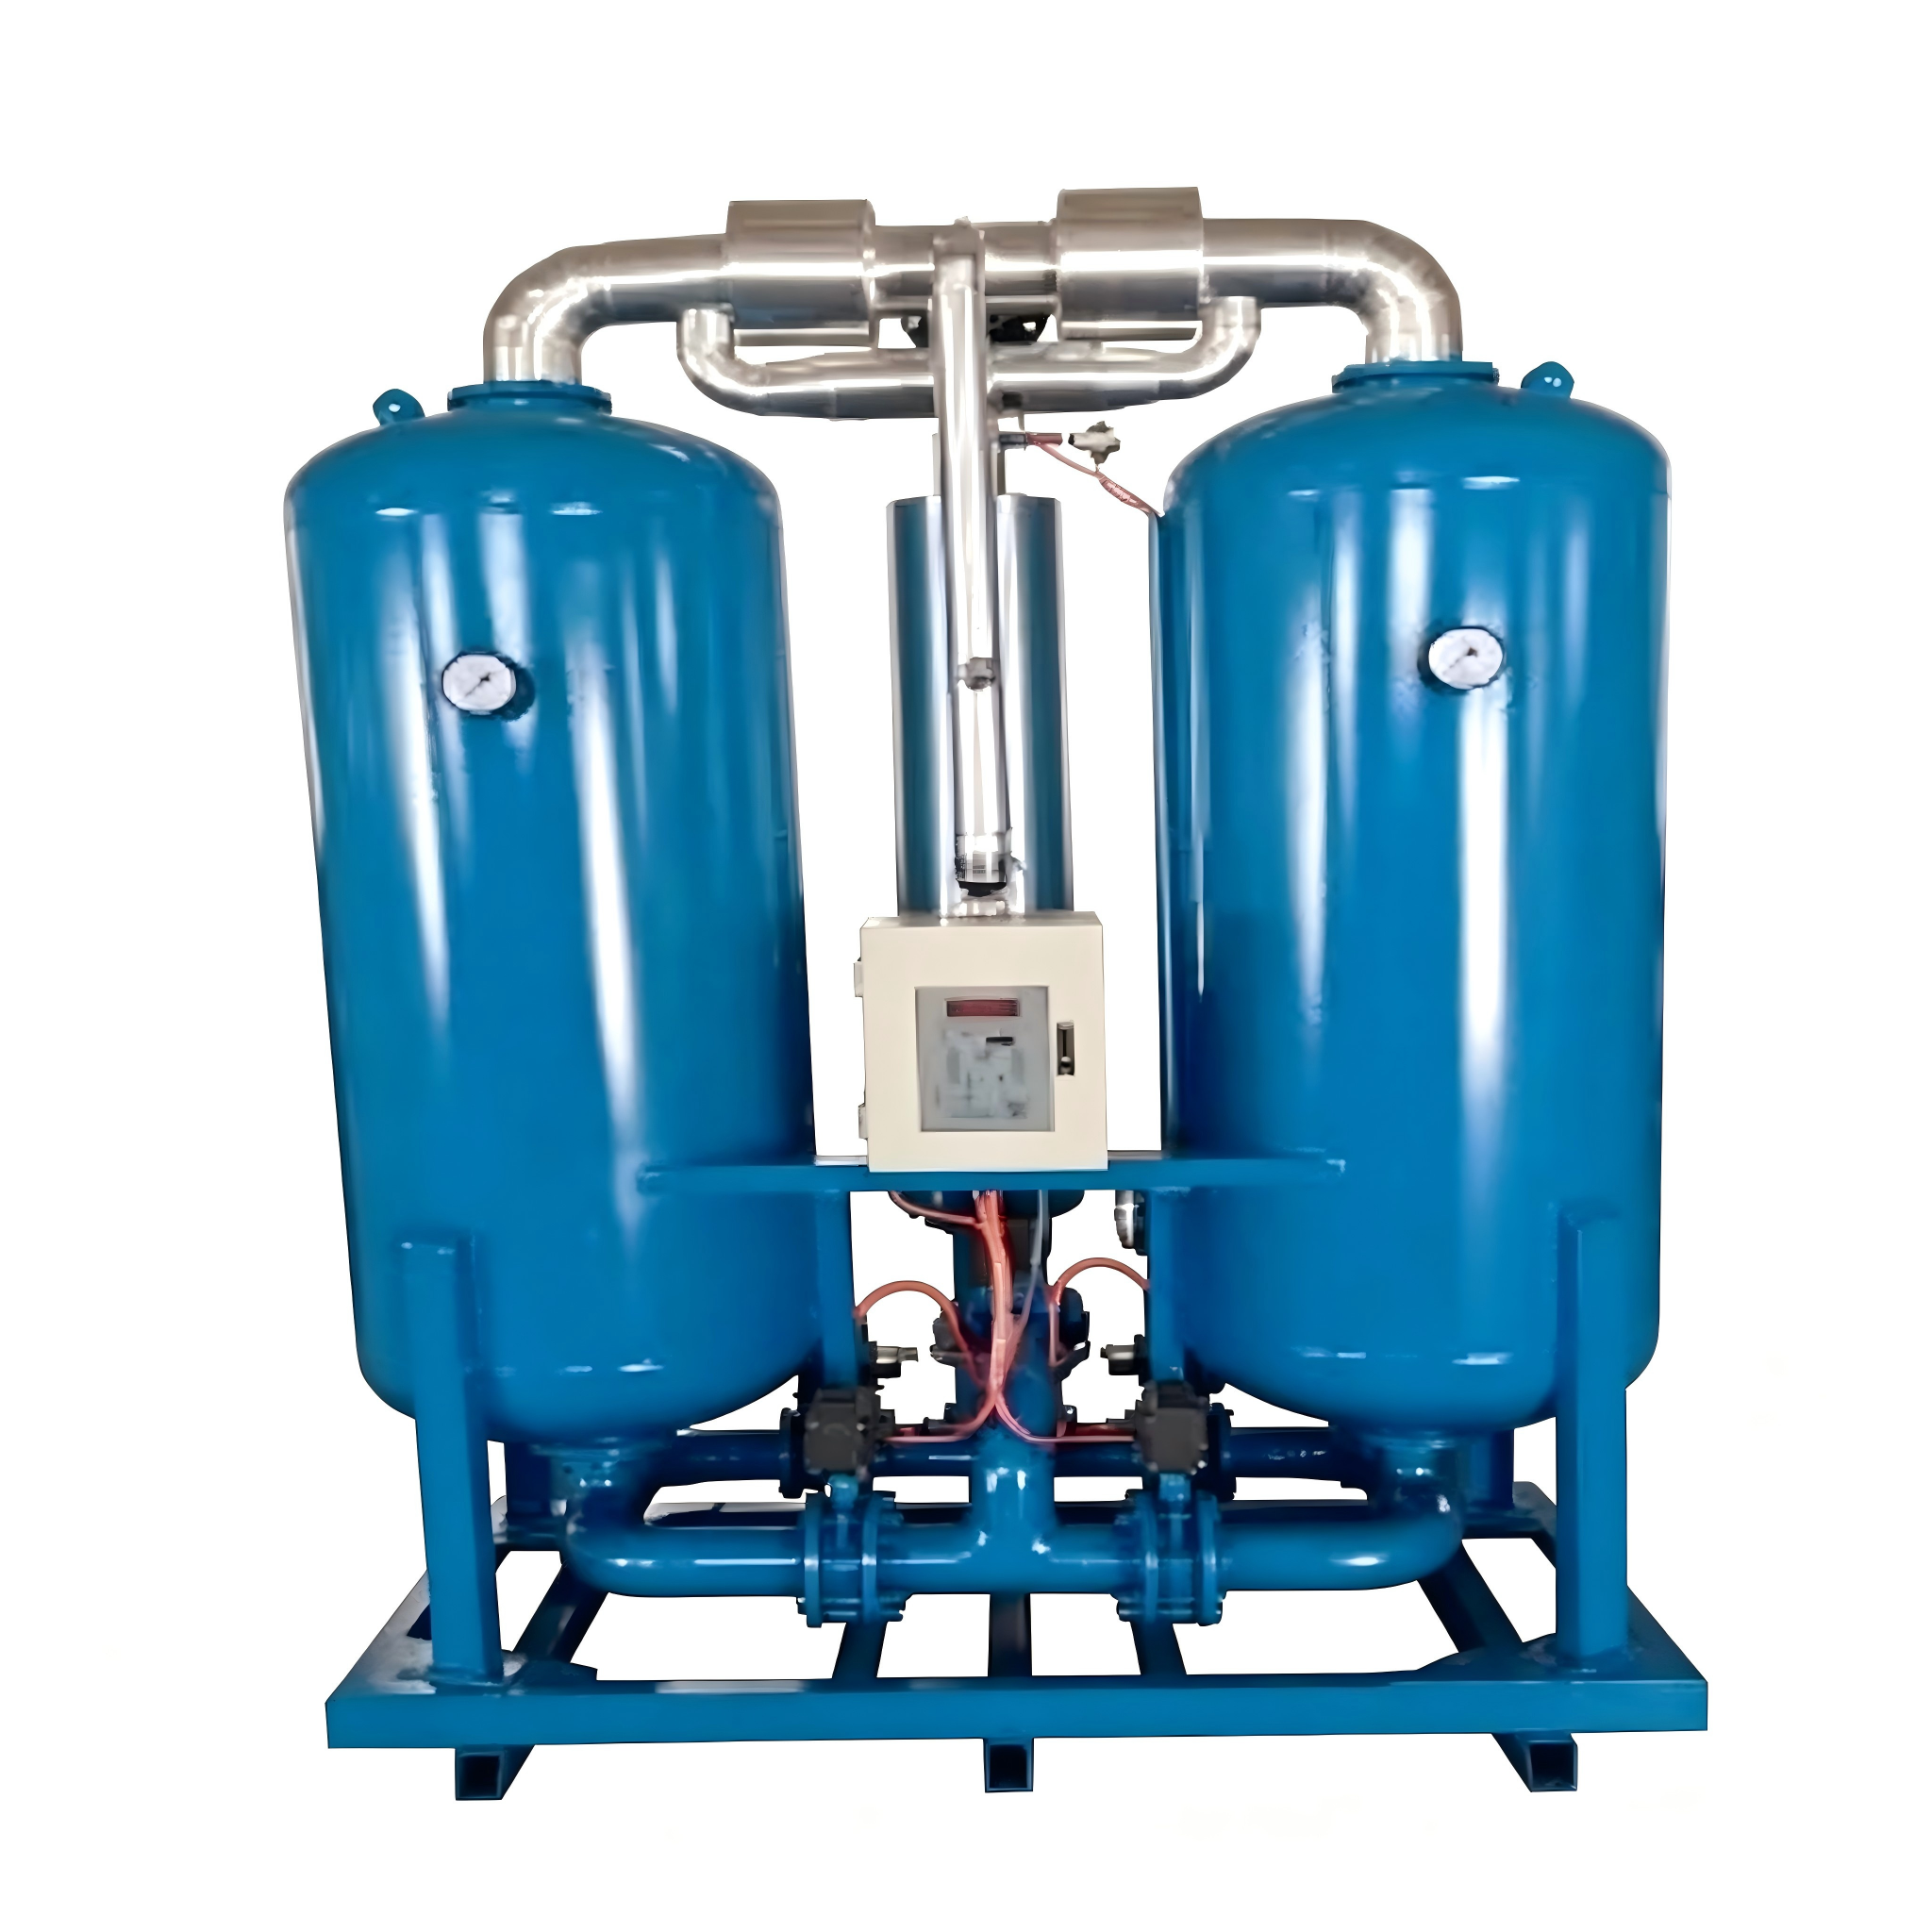
Precision-matched low pressure air compressor packages, refrigerated dryers, and VSD systems configured specifically for dilute and dense phase powder transfer.
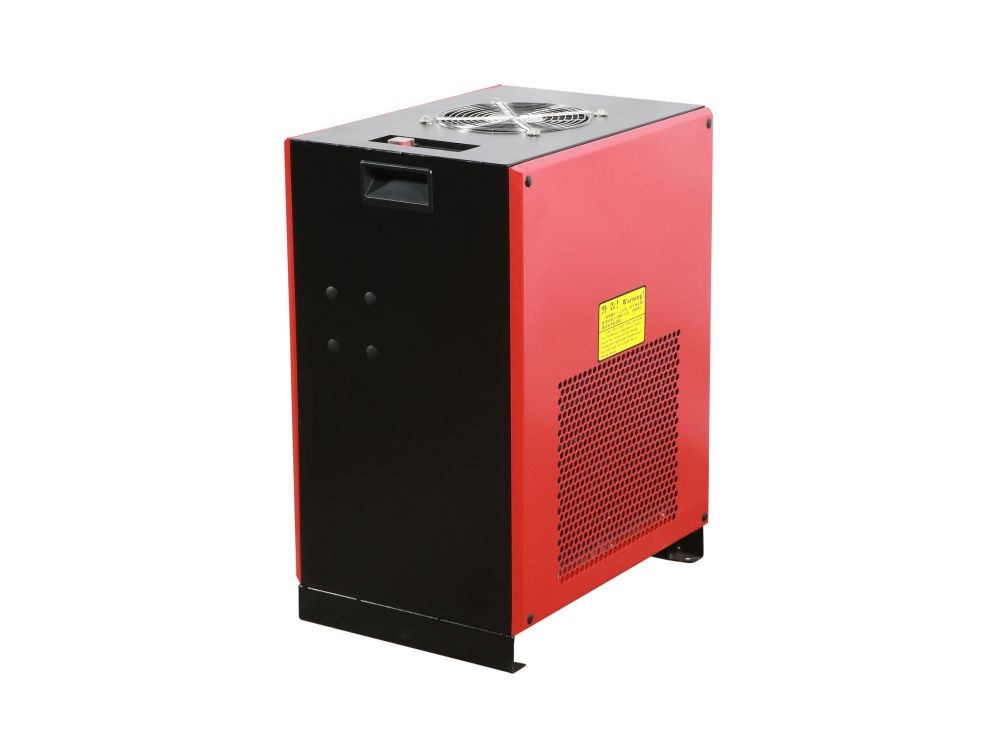
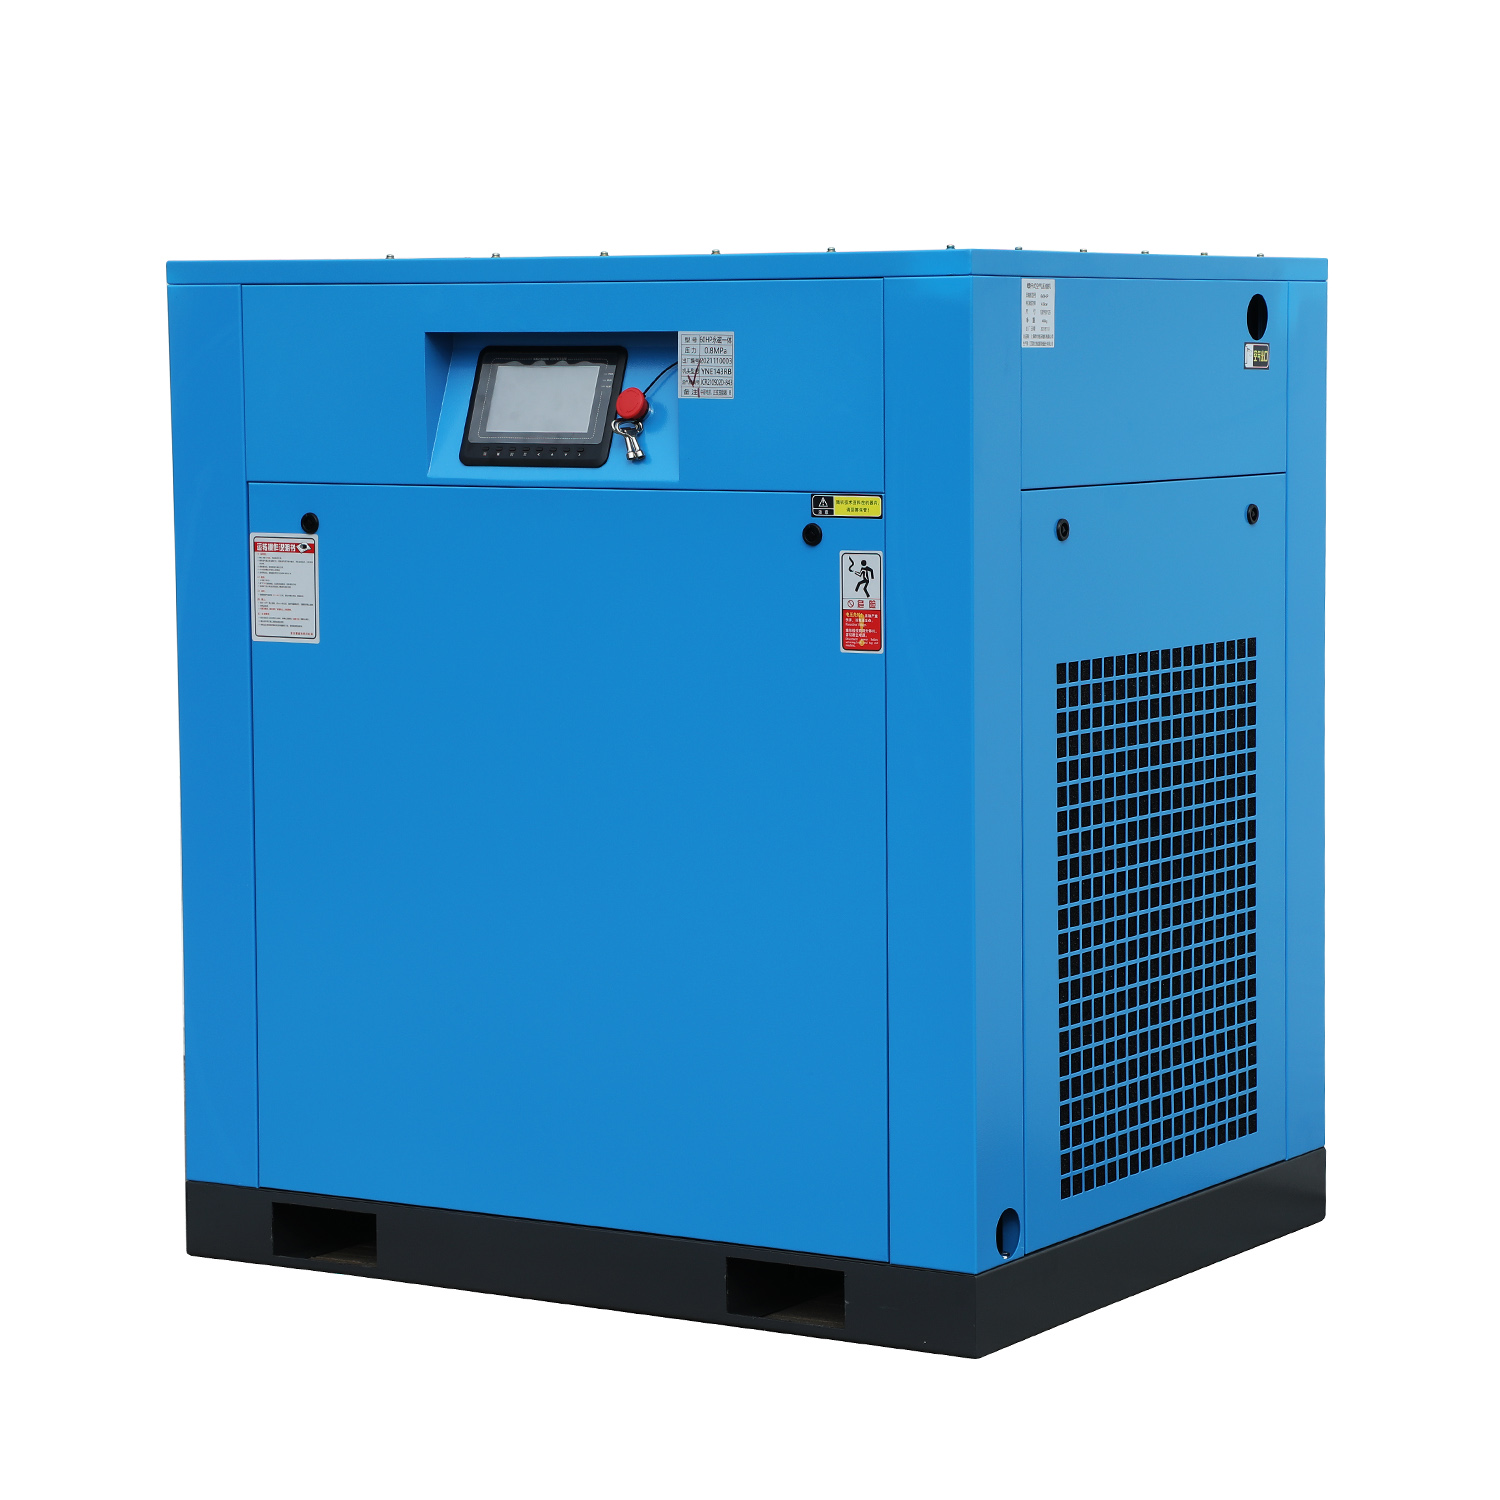
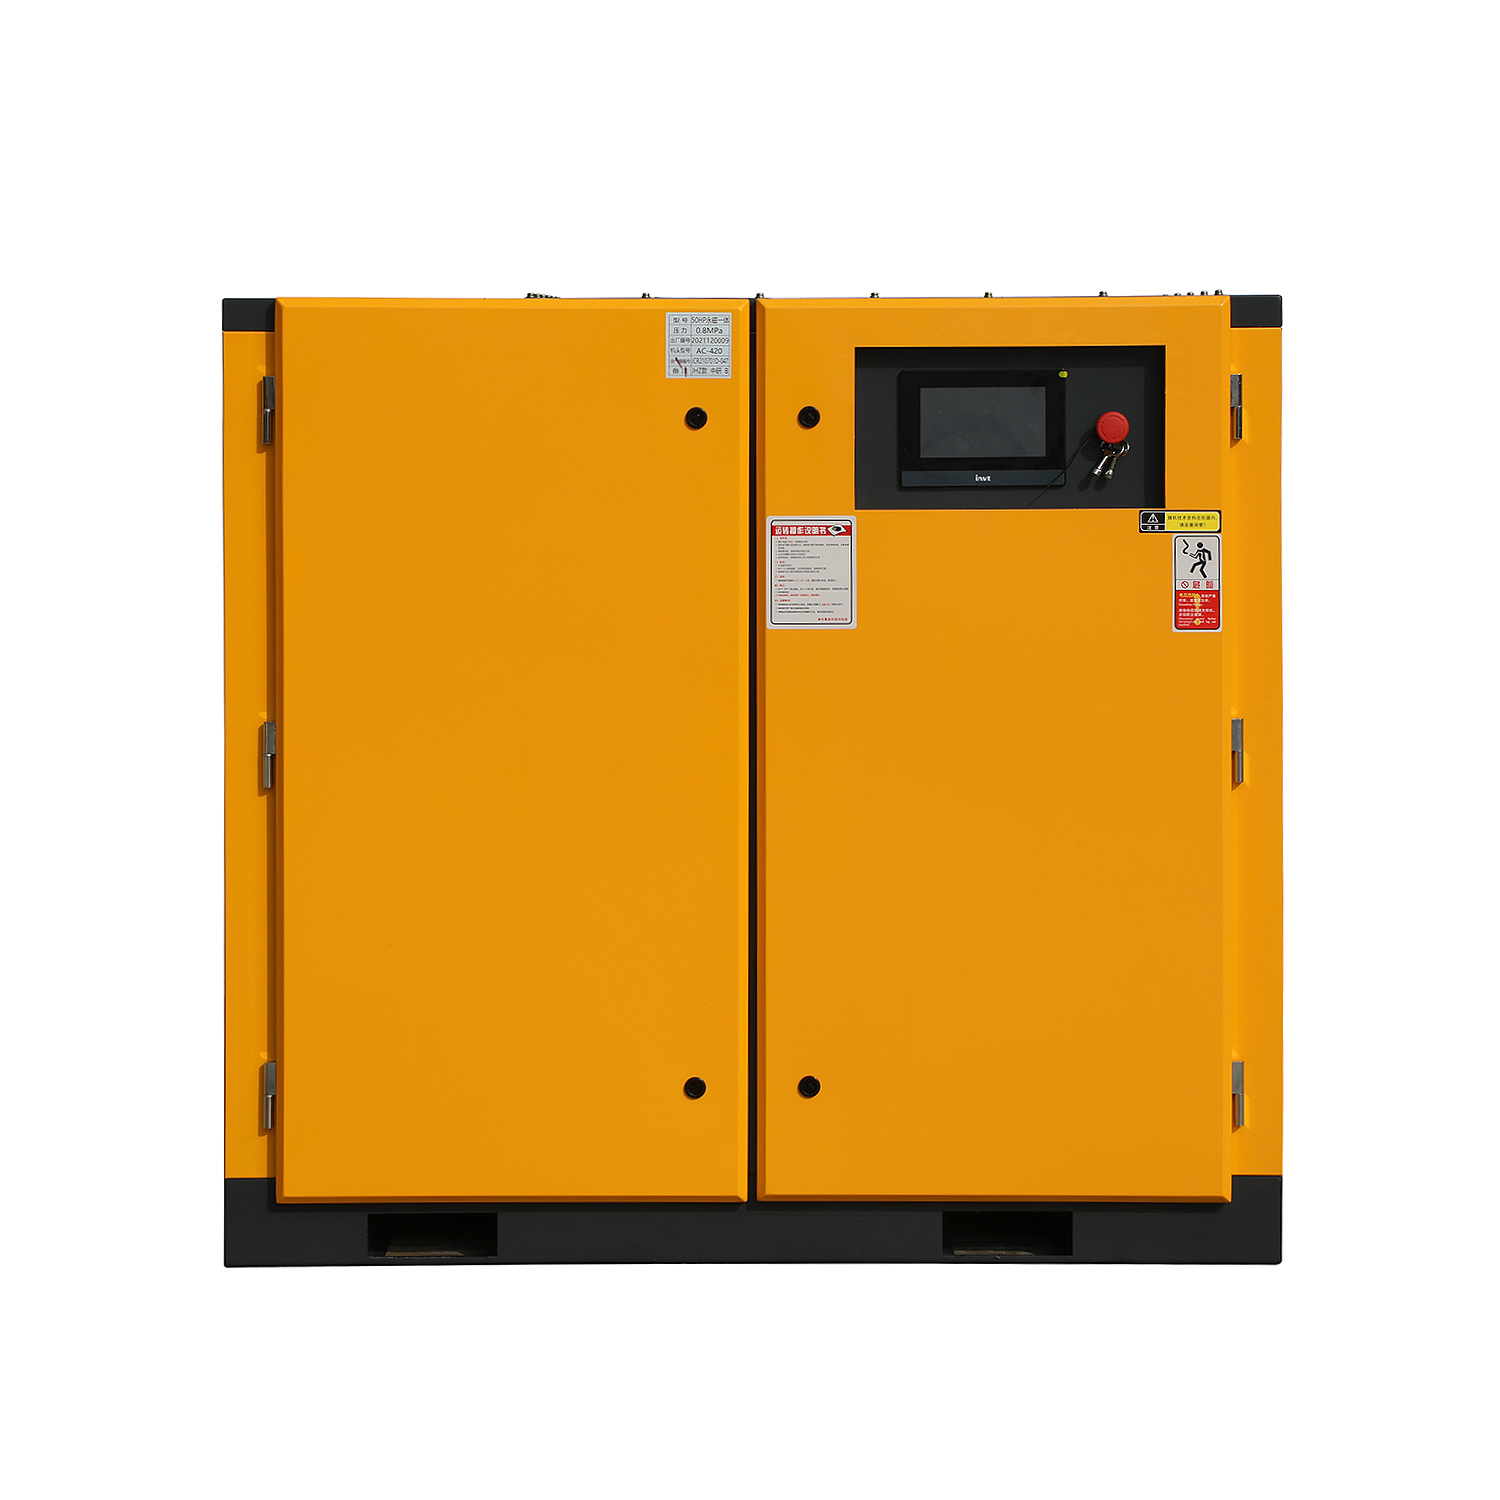
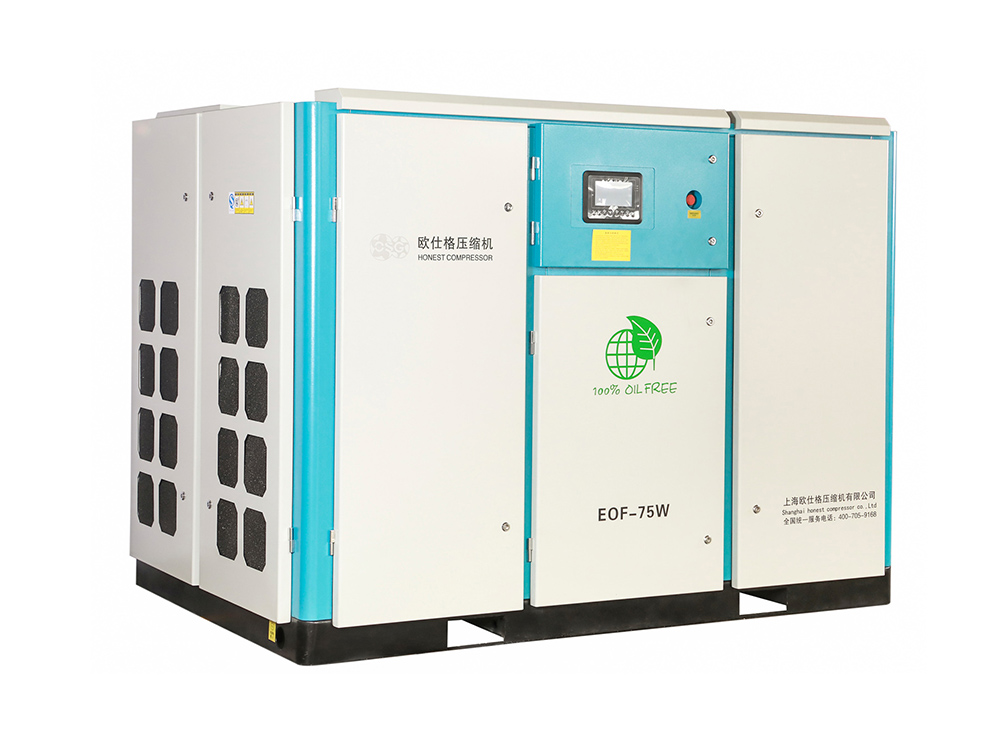
The Paradigm Shift in Pneumatic Powder Handling
Discover why modern manufacturing facilities are replacing legacy Roots blowers and high-pressure throttled systems with dedicated low pressure rotary screw air compressors.
Direct Pressure Matching
Standard compressors generate 0.7–0.8 MPa that must be de-pressurized to 0.2–0.4 MPa for conveying, wasting up to 45% of power. Low pressure screw units compress directly to process pressure.
Internal Compression Efficiency
Unlike traditional Roots blowers that operate via external back-compression with significant thermodynamic loss, screw airends compress air internally along the helical rotor profile.
Pulsation-Free Continuous Flow
Smooth volumetric displacement prevents pressure spikes, reducing pipe line vibration, elbow abrasion, and particle degradation during dilute and dense phase powder transfer.
In contemporary powder processing, cement manufacturing, chemical batching, and grain logistics, pneumatic conveying systems serve as the vascular backbone of material transfer. Historically, plant operators faced a costly compromise: deploy multi-lobe Roots blowers that struggle when back-pressure rises above 0.1 MPa (1.0 bar), or employ conventional 0.8 MPa screw air compressors equipped with pressure reduction valves. Throttling high-pressure air directly burns surplus kilowatt-hours without adding process value.
The arrival of dedicated Low Pressure Screw Compressors (0.15 MPa to 0.50 MPa / 1.5 to 5.0 bar) has revolutionized bulk handling aerodynamics. By engineering asymmetric rotor profiles specifically optimized for low volumetric compression ratios, these units provide steady, pulsation-free volume flow rates spanning from 0.5 m³/min to over 75 m³/min. This targeted aerodynamic design guarantees minimal specific power consumption (kW/m³/min), thermal stability, and robust dust-tight continuous operation under demanding 24/7 industrial environments.
Pneumatic Conveying Modes & Deep Sector Applications
Analyzing system pressures, air velocities, and thermodynamic behavior across lean-phase, dilute-phase, and dense-phase powder conveying systems.
1. Dilute Phase Pneumatic Conveying (Velocity: 15–30 m/s | Pressure: 0.15–0.25 MPa)
In dilute or lean phase conveying, solid particles remain fully suspended in the conveying air stream. This mode relies on high air volume and moderate pressure to transport non-abrasive, non-fragile bulk materials over medium distances. Low pressure screw compressors deliver continuous mass flow without pulsation, avoiding material settlement ("salting out") at pipe elbows and horizontal runs. Key applications include grain handling, flour milling, plastic resin pellet feeding, and wood pulp injection.
2. Dense Phase & Plug Flow Conveying (Velocity: 3–12 m/s | Pressure: 0.25–0.50 MPa)
Dense phase conveying moves materials along the pipeline in compact slugs, dunes, or fluidized plugs at low speed. Operating pressures typically range between 0.25 MPa and 0.45 MPa. Because the material-to-air mass ratio is high, pressure drops across the pipeline can fluctuate quickly. The high volumetric stiffness of a rotary screw compressor ensures that flow rate does not collapse under fluctuating back-pressure—preventing disastrous pipeline blockages in cement terminals, fly ash collection, glass batching, and foundry sand circuits.
3. Specialized High-Purity & Temperature-Sensitive Bulk Logistics
For pharmaceutical powders, baby formula, carbon black, and new-energy lithium battery cathode materials (e.g., LFP, NCM), contamination from lubricating oil or excessive heat can ruin an entire production lot. Using Oil-Free Low Pressure Screw Compressors paired with air-cooled refrigeration dryers guarantees ISO 8573-1 Class 0 oil-free air with discharge dew points between 2°C and 10°C, preserving chemical purity and preventing hygroscopic caking.
Comparative Engineering Matrix
| Conveying Technology | Standard Operating Pressure | Specific Energy Efficiency | Noise & Vibration Level | Clogging Resistance |
|---|---|---|---|---|
| Low Pressure Screw Compressor | 0.15 – 0.50 MPa (Customized) | Ultra High (Targeted Isobaric Curve) | 62 – 72 dB(A) Smooth Enclosed | Superior (Stable Displaced Volume) |
| Roots Rotary Blower | 0.03 – 0.10 MPa (Limited) | Moderate (Drops rapidly above 0.08 MPa) | 85 – 105 dB(A) High Pulsation | Poor (Slip rate rises under high back-pressure) |
| Standard Compressor + Reducer | 0.70 – 0.85 MPa (Over-compressed) | Very Poor (40-50% Throttling Loss) | 68 – 75 dB(A) Enclosed | Moderate (Depends on regulator response) |
Company Profile & Engineering Strengths
British engineering lineage combined with advanced large-scale production facilities in Shanghai, China.
Shanghai Honest Compressor Co., Ltd. is a British-owned enterprise founded in early 2004. Our modern production headquarters is located at NO. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, China. As a premier large-scale manufacturing enterprise specializing in twin-screw air compressors in China, we stand as an authoritative provider of full-scope industrial air system solutions.
Our comprehensive product portfolio encompasses diverse piston air compressors (low pressure, medium pressure, high pressure, oil-free), rotary screw compressor systems (3kW to 480kW, covering flow rates of 0.5 m³/min to 75 m³/min in air-cooled and water-cooled configurations), gas separation equipment, refrigerant compressors, cold dryers, micro-heat regeneration desiccant dryers, line filters, and advanced ceramic membrane filtration systems.
We fully implement strict management throughout the entire manufacturing process, meticulously monitoring build quality and ecological footprint. The company is certified under the ISO9001:2015 Quality Management System. Rigorously tested by the National Compressor Inspection Center, our energy consumption data consistently outperforms national energy-saving benchmarks.
We maintain active technology R&D aligned with market shifts and pneumatic conveying demands, offering complete turn-key compressor station design, manufacturing, operator training, and lifetime overhaul hosting. For instant customer support, we maintain nationwide branch service networks and a toll-free hotline at 400-705-9168.
AI-Driven Permanent Magnet VFD Integration
Dynamic frequency conversion algorithms adjust volumetric output in real time to match instantaneous pipeline pneumatic load demands.
Real-Time Pressure Sensing
High-speed pressure transmitters sample pneumatic transport line resistance at 50Hz, dynamically varying motor RPM to prevent pipeline choke points before they occur.
IE4/IE5 Permanent Magnet Motors
Ultra-efficient permanent magnet motors retain peak efficiency even during partial 25%–50% load operations, eliminating unloaded idle losses during silo switching.
IoT Remote Station Diagnostics
Cloud-linked telemetry monitors oil temperature, filter differential pressure, and specific energy in real time, delivering automated maintenance alerts.
Pneumatic Conveying Compressor FAQs
Common technical queries regarding compressor sizing, pressure selection, and moisture control for bulk powder conveying.
Q1: Why should I select a 0.3 MPa screw compressor instead of an 0.8 MPa compressor with a pressure reducer?
Compressing air to 0.8 MPa consumes energy to overcome high internal compression resistance. When air passes through a pressure reducing valve down to 0.3 MPa, that excess compression work is lost as heat. Direct low pressure compression consumes only the exact energy needed, saving 30%–40% in electricity.
Q2: How does compressed air moisture affect powder conveying pipelines?
Moisture causes hygroscopic powders (cement, sugar, milk powder, fly ash) to agglomerate, causing rotary valves to bind and pipes to plug. Integrating refrigerated dryers (2–10°C dew point) or desiccant dryers ensures completely dry transfer medium.
Q3: Can low pressure screw compressors handle fluctuating conveying distances?
Yes. With Permanent Magnet Variable Frequency Drive (PM VFD) technology, our low pressure units dynamically modulate motor speed to deliver constant pressure regardless of pipeline length or silo changes.
Q4: What maintenance interval is expected for low pressure screw units?
Because operating pressures are lower (0.2–0.5 MPa), rotor bearing loads and operating temperatures are substantially reduced compared to standard units, extending rotor bearing lifespans beyond 60,000 operational hours.
Pneumatic System Compressors & Air Treatment
Explore our complete range of low pressure, variable speed, oil-free air compressors and purification systems engineered for bulk material conveying.