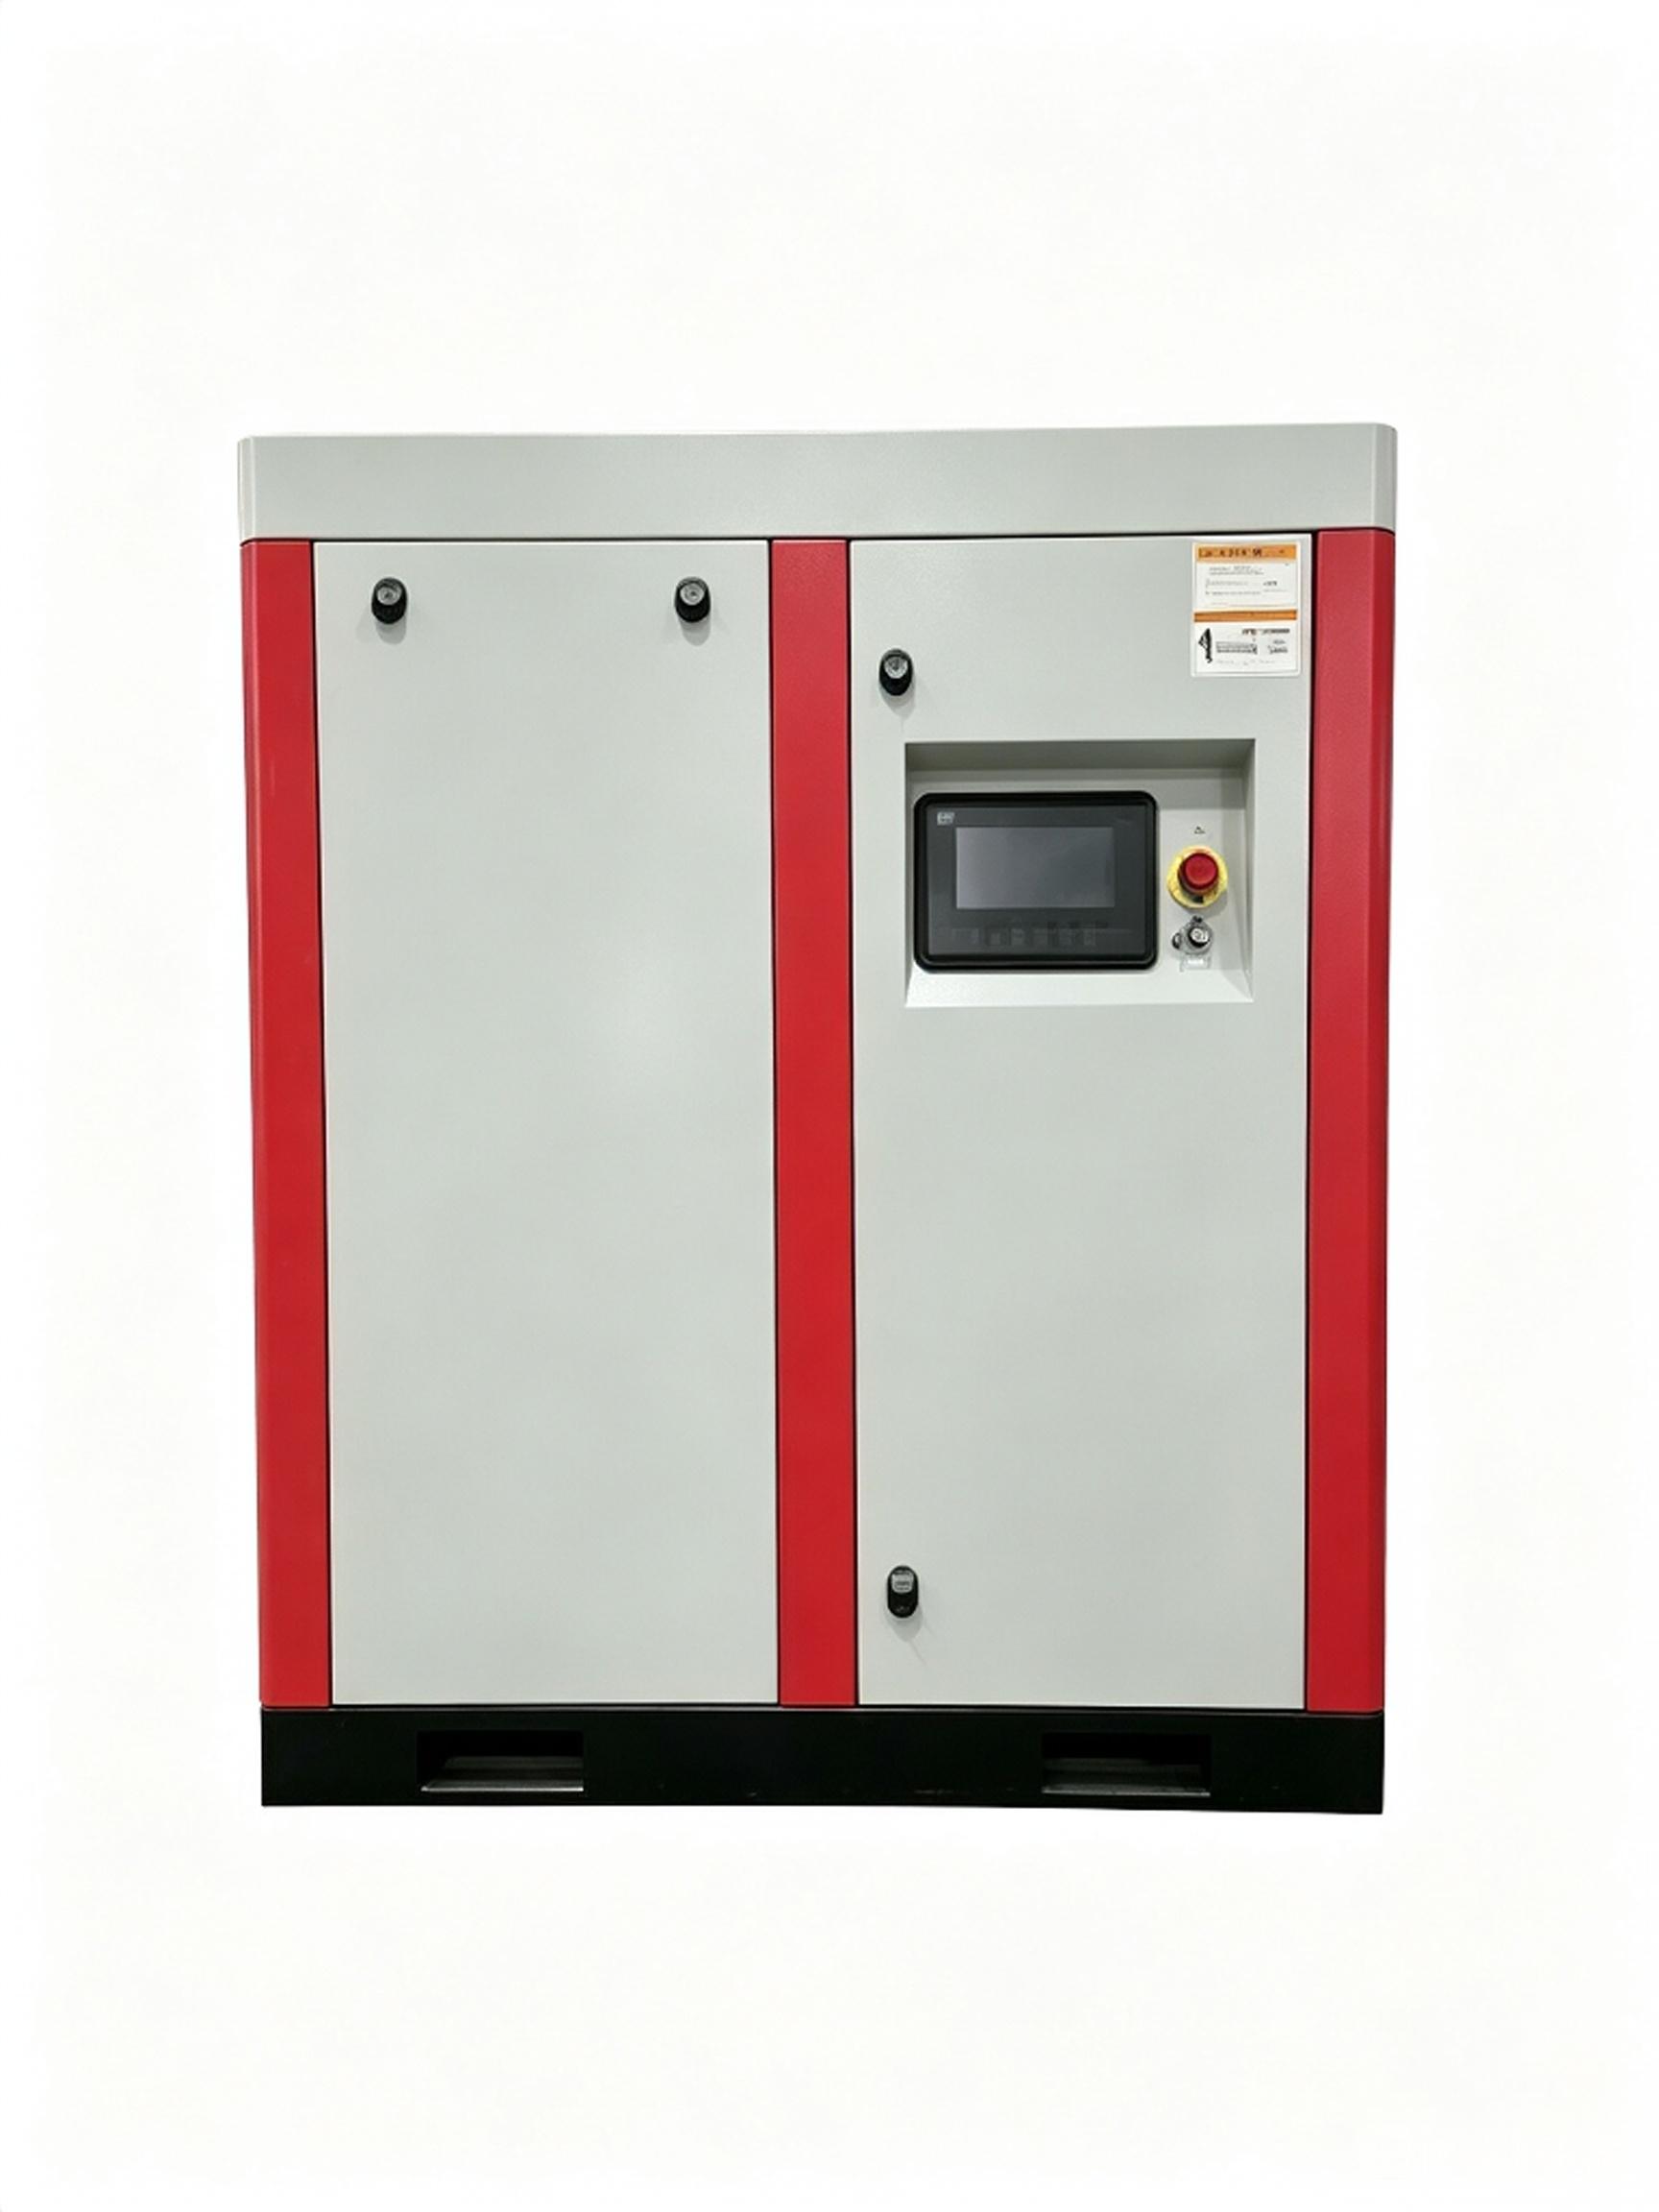
Engineered Compressors for Pneumatic Conveying Systems
Explore high-durability rotary screw compressor units specifically configured to maintain stable pressure gradients, pulse-free mass flow rates, and high energy efficiency during continuous bulk solids transfer.
1. Industrial Evolution of Rotary Screw Gas Compressors in Pneumatic Conveying
Pneumatic conveying systems represent the lifeline of modern bulk solid material handling across manufacturing, energy production, metallurgy, food processing, pharmaceuticals, and petrochemicals. The transport of dry bulk materials—ranging from non-abrasive flour, starches, and plastic pellets to severe abrasive compounds such as cement clinker, fly ash, silica sand, and lithium iron phosphate (LiFePO4)—depends entirely on the continuous aerodynamic force generated by pressurized gas or air streams.
Historically, industrial processing plants depended heavily on positive displacement Roots blowers or reciprocating piston compressors for material movement. While Roots blowers perform acceptably at low pressures (typically below 1.0 bar / 14.5 psi), their mechanical profile suffers from severe internal backflow leakage, low volumetric efficiency, steep thermal escalation, and extreme acoustic noise. Conversely, traditional reciprocating piston compressors create cyclic pulsation patterns in conveying pipelines, precipitating line vibration, accelerated pipe bend erosion, and unstable solids-to-gas loading ratios.
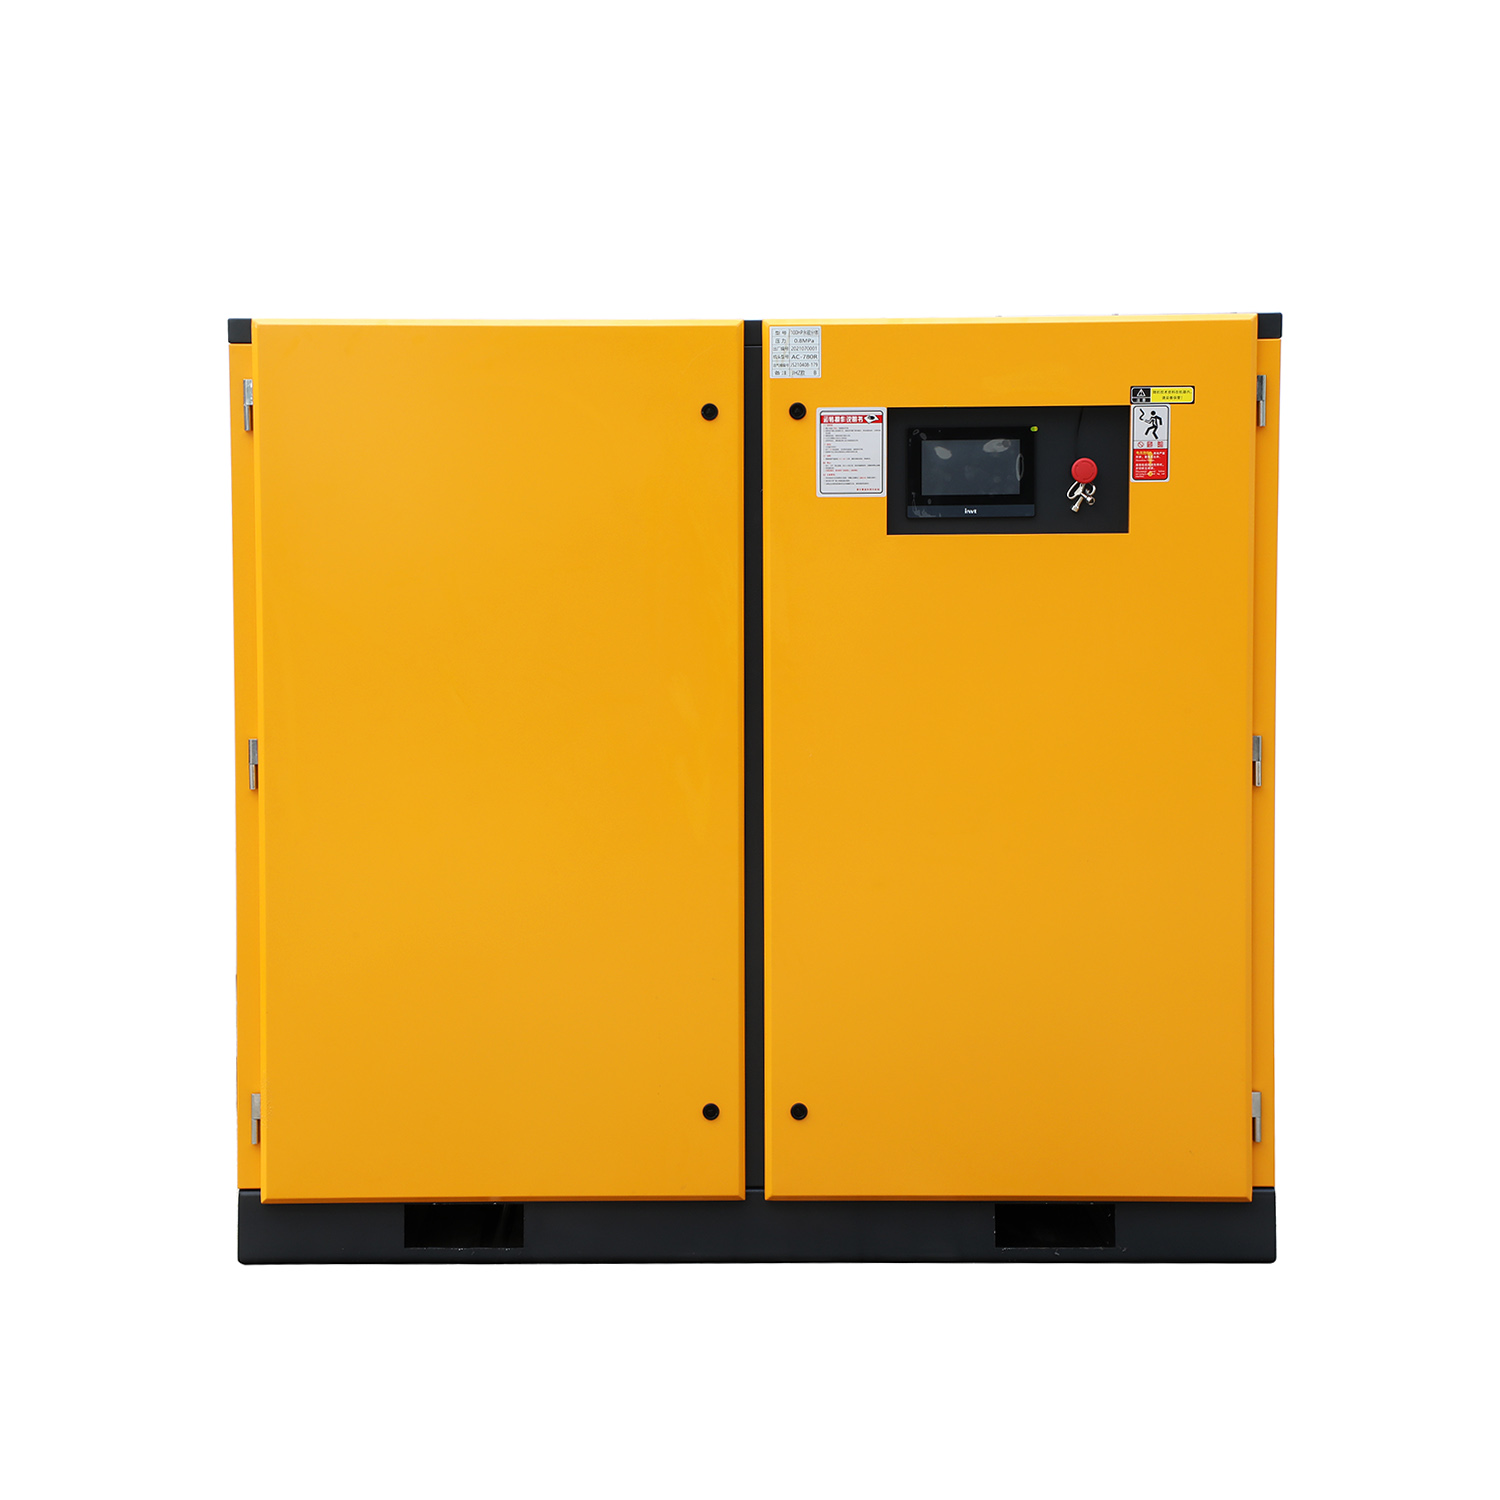
The industrial emergence of the rotary screw gas compressor revolutionized pneumatic conveying engineering. Operating via twin helical intermeshing rotors (male and female) that progressively reduce gas volume through continuous axial displacement, rotary screw machinery eliminates pulsation entirely. Rotary screw compressors deliver constant, pulsation-free volume flow across a comprehensive pressure spectrum (typically ranging from 1.5 bar up to 13 bar), bridging the operational gap between low-pressure blowers and high-pressure process gas compressors with outstanding specific energy efficiency.
Continuous Pulse-Free Gas Dynamics
Helical twin-screw rotation produces smooth, laminar gas discharge directly into conveying lines. The absence of pressure pulsations prevents line surging, protects delicate granular products against degradation, and minimizes mechanical fatigue on pipeline bends and diverter valves.
Superior Energy Efficiency & VSD Control
Permanent Magnet Variable Speed Drive (PM-VSD) integration matches instantaneous compressed gas delivery to dynamic system resistance. Plants operating variable feed rates achieve up to 35% reduction in specific power consumption (kWh/ton moved).
2. Deep Scenario Analysis: Dilute Phase vs. Dense Phase Conveying Mechanics
Selecting the correct rotary screw gas compressor requires comprehensive comprehension of fluidization mechanics, saltation velocities, and solids loading ratios (SLR). Pneumatic conveying regimes generally diverge into two primary methodologies:
| Conveying Phase | Operating Pressure | Gas Velocity | Solids Loading (kg/kg) | Optimal Screw Compressor Configuration |
|---|---|---|---|---|
| Dilute / Lean Phase (Suspension) | 0.5 to 2.5 bar (g) | 15 – 35 m/s | < 15 kg/kg | Direct-Drive Low-Pressure Rotary Screw Air Compressor with integrated aftercooler |
| Dense Phase (Slug / Plug Flow) | 2.5 to 7.0+ bar (g) | 3 – 12 m/s | 15 – 100+ kg/kg | Two-Stage High-Efficiency Screw Compressor with PM-VSD Motor & Refrigerant Dryer |
| Closed-Loop Inert Gas (N2/CO2) | 1.5 to 10.0 bar (g) | 5 – 22 m/s | Variable | Explosion-Proof Hermetic Gas Screw Compressor with Ceramic Membrane Filtration |
Dense Phase Pressure Vessel (Blow Pot) Systems
Dense phase conveying transfers heavy, abrasive, or fragile powders at low velocity in concentrated slugs or plugs along pipeline trajectories. Because velocities remain low (below saltation velocity), abrasive wear on stainless steel or basalt-lined piping is reduced by over 80%, and particle attrition is virtually eliminated. However, overcoming the high static resistance of compact powder columns demands continuous operating pressures between 2.5 bar and 6.0 bar.
Here, single-stage or two-stage rotary screw compressors excel. They maintain constant volumetric displacement even when pipeline resistance surges during plug transitions, preventing line blockages that commonly trip centrifugal blowers. Integrated variable frequency drives automatically modulate compressor rpm to stabilize pressure differentials across rotary airlock valves and venturi injectors.
Lean / Dilute Phase Continuous Velocity Transfer
Dilute phase conveying relies on high-velocity gas streams to entrain particles and hold them in suspension throughout the pneumatic conveying line. Operating primarily at lower gauge pressures (1.0 to 2.5 bar) but requiring high cubic flow rates (CFM / m³/min), rotary screw compressors equipped with specialized low-pressure airends deliver massive airflow with substantially lower thermal discharge compared to over-revved Roots packages.
3. Critical Gas Conditioning for Sensitive Pneumatic Conveying Lines
A compressed gas supply for powder conveyance cannot be treated merely as raw plant air. Gas quality directly dictates operational reliability, powder preservation, and silo safety:
Thermodynamic Dew Point Management: Atmospheric moisture compressed into pipelines condenses into liquid water, causing hygroscopic powders (such as cement, sugar, quicklime, and polymers) to cake, agglomerate, and weld pipelines shut. High-performance screw compressor stations incorporate integrated refrigerated or desiccant air drying units, driving pressure dew points down to -40°C (-40°F) for fail-safe winter operation.
Oil Aerosol Elimination: In food-grade milk powders, baby formula processing, medical APIs, and high-purity chemical manufacturing, even trace oil aerosols cause batch contamination. Water-lubricated oil-free rotary screw compressors and oil-less screw packages certified to ISO 8573-1 Class 0 ensure 100% hydrocarbon-free propellant gas.
Inert Gas Recycling (Nitrogen Conveying): When handling volatile combustible dusts (such as powdered coal, sulfur, fine aluminum powder, or organic resins), conveying systems must operate in closed-loop configurations using pure Nitrogen ($N_2$) or Carbon Dioxide ($CO_2$) to suppress oxidation and eliminate explosion hazards. Specialized explosion-proof rotary screw gas compressors feature hermetic mechanical seals, nitrogen purged buffer zones, and ATEX/IECEx certified drive enclosures.
Company Profile & Engineering Heritage
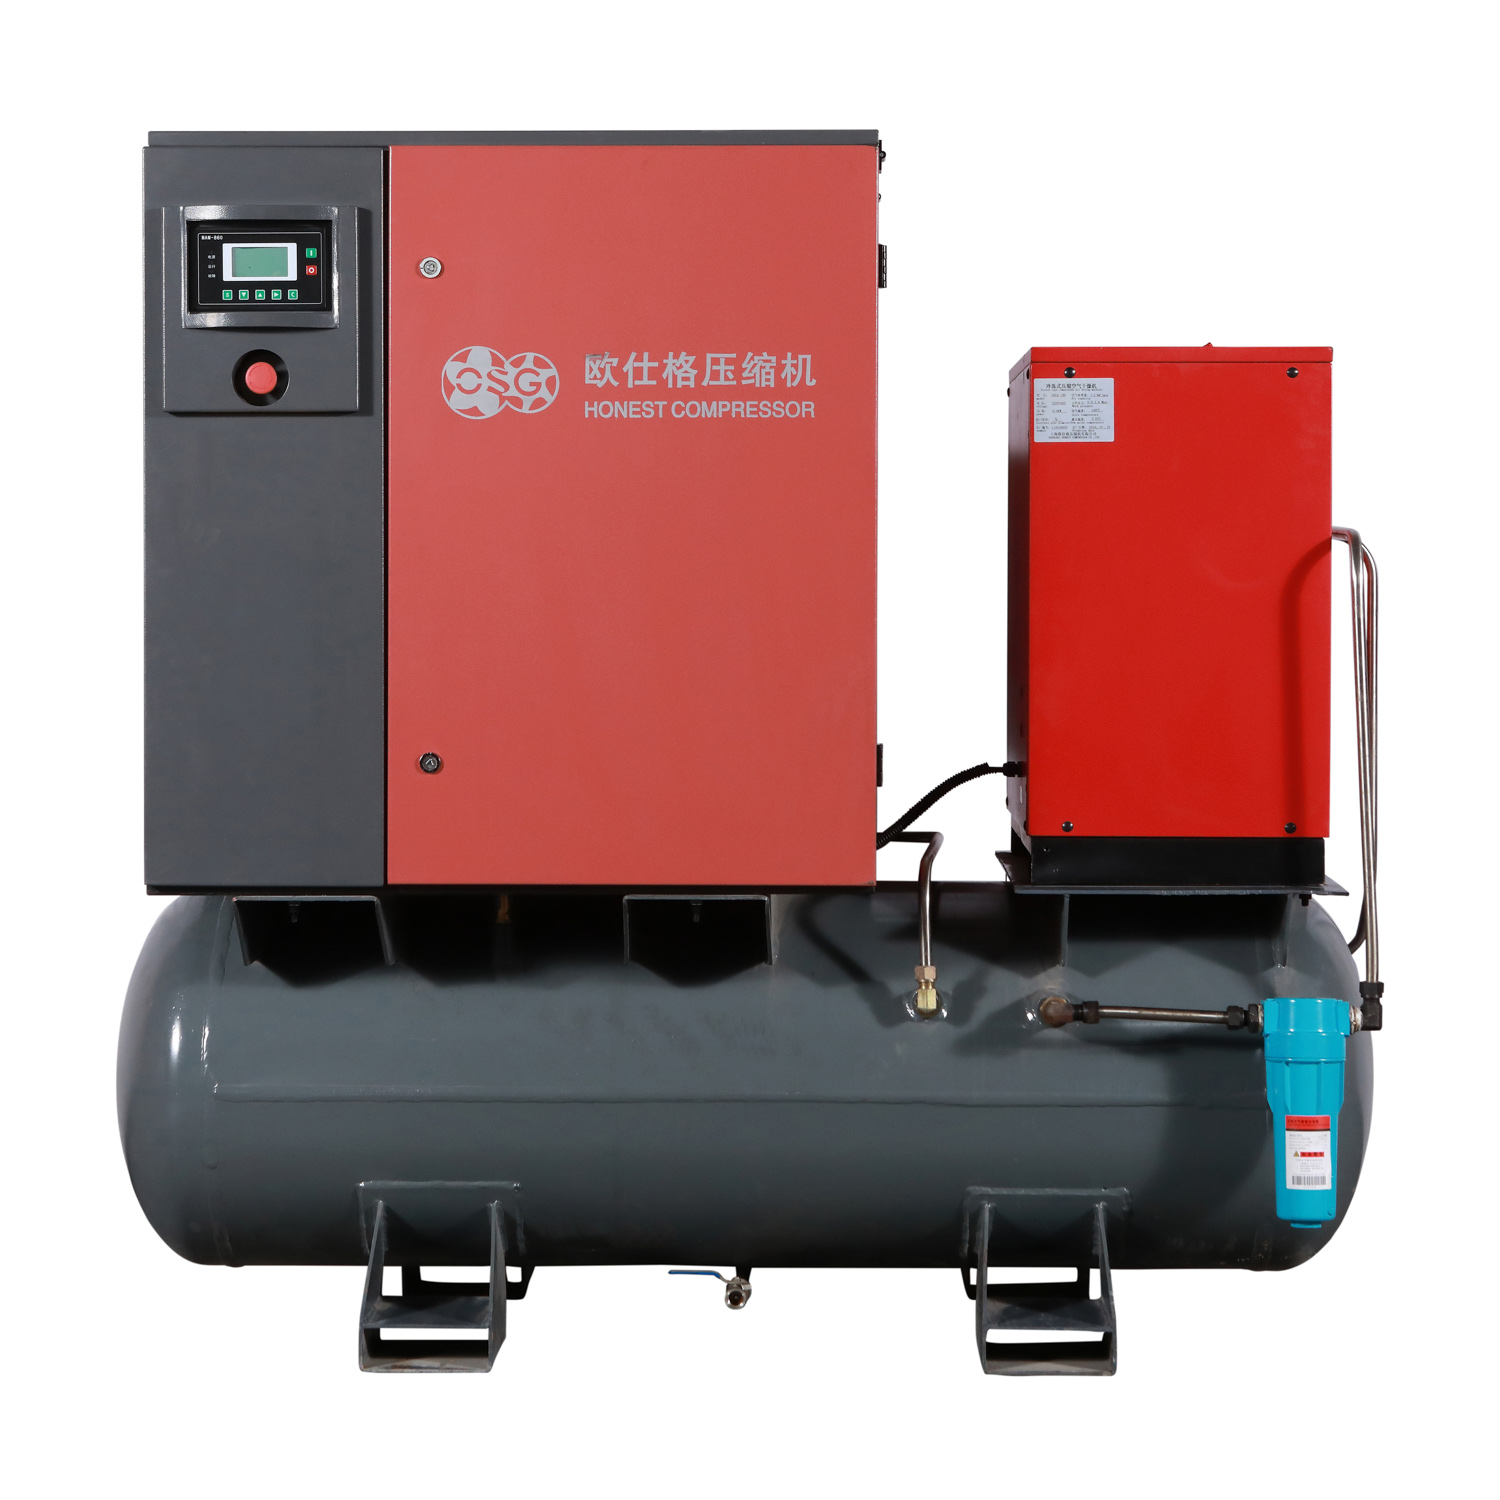
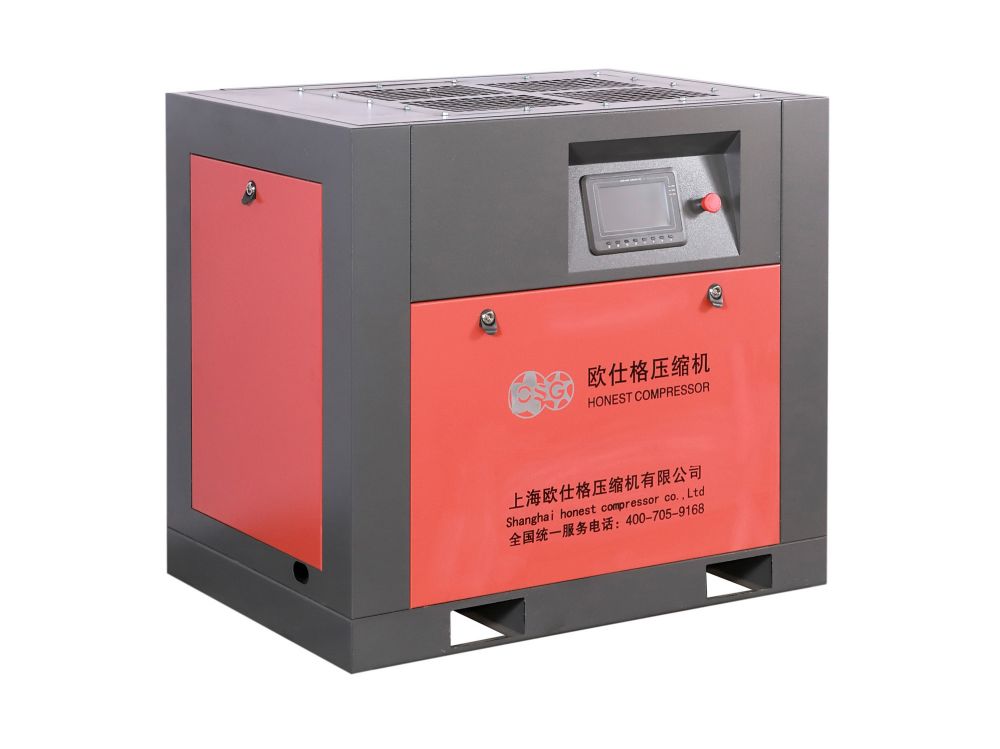
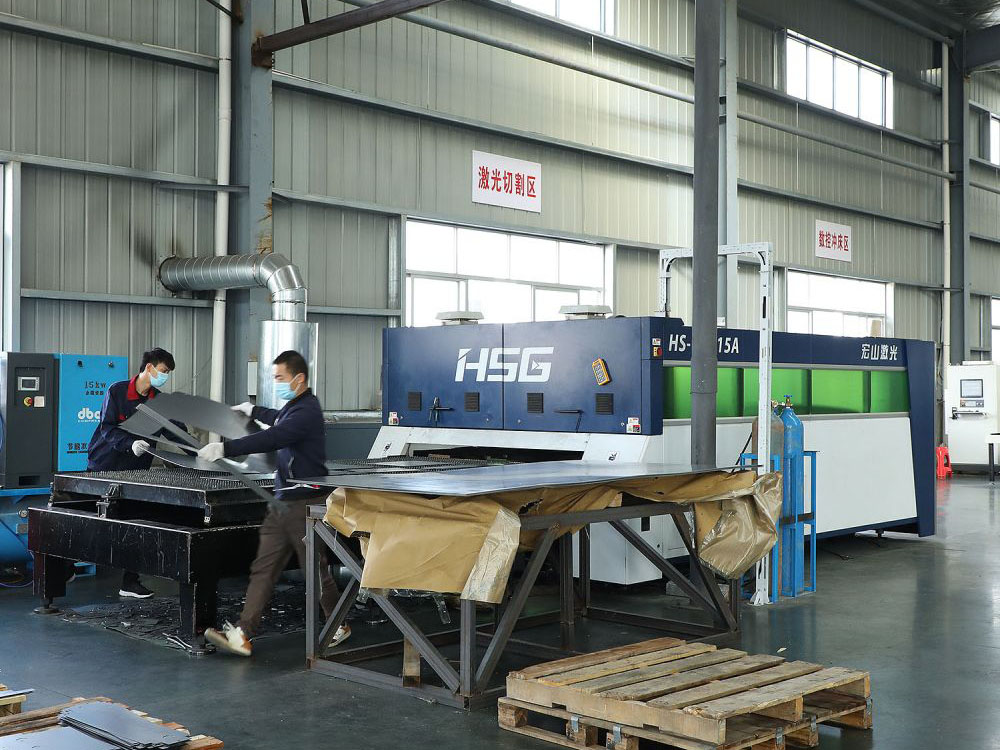
Shanghai Honest Compressor Co., Ltd. is a British-owned enterprise. It was founded in early 2004. The production address is located at NO. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, China. It is a large-scale manufacturing enterprise specializing in the production of twin-screw air compressors in China. At the same time It is also an important supplier of air system solutions.
We provide various types of piston air compressors (low pressure, medium pressure, high pressure, oil-free air compressors), screw air compressor systems (3KW-480KW various screw air compressors, gas separation equipment, refrigerant Compressors, cold dryers, filters, ceramic membrane filtration systems) and various equipment accessories and consumables.
We fully implement strict management throughout the entire manufacturing process, strictly monitor product quality and environmental protection, and the company has passed ISO9001:2015 quality management system certification.
We pay attention to market trends in technology research and development, close to the needs of users, actively absorb the advantages of domestic and foreign brand performance structures, and integrate our own features of convenient maintenance, so that the air compressors we produce have more perfect structures, better performance, and energy saving and consumption reduction. Obviously, after the test of the National Compressor Inspection Center, the energy consumption data is superior to the national energy-saving standard, and can provide users with various series of 3kW--480kW, air-cooled and water-cooled screw air compressors with a flow rate of 0.5m³/min-75m³/min.
4. Emerging Trends in Gas Compression for Automated Bulk Logistics
The industrial world is experiencing a paradigm shift toward Industry 4.0 intelligent automation, energy decarbonization, and zero-loss material processing. Rotary screw gas compressors designed for pneumatic conveying systems are rapidly evolving with transformative advancements:
1. AI-Driven Smart Pipeline Telemetry: Modern rotary screw stations utilize high-frequency IoT pressure transducers at multiple line nodes. When line choking or line density shifts are detected upstream, the compressor's AI algorithm modulates rotor RPM instantaneously to adjust mass flow, clearing dense material bridges before a line plugging emergency occurs.
2. Direct-Drive Permanent Magnet Motor Technology: Eliminating drive belts, pulleys, and secondary gearboxes reduces mechanical transmission losses to less than 0.2%. IE4 and IE5 super-premium efficiency permanent magnet synchronous motors run at high torque densities across broad frequency spans, delivering uncompromised efficiency during both peak silo unloading cycles and idle standby periods.
3. Waste Heat Recovery Integration (WHR): Up to 94% of the electrical energy consumed by a continuous pneumatic conveying screw compressor is converted into thermal energy. Modern plant designs capture this heat through dedicated oil-to-water heat exchangers to preheat boiler makeup water, provide administrative HVAC, or dry incoming hygroscopic powders prior to conveying.
Full Range Rotary Screw Solutions For Pneumatic Conveying
Explore our comprehensive line of rotary screw air and gas compressors, oil-free vacuum pumps, explosion-proof units, and two-stage energy-saving systems manufactured for heavy-duty industrial processing.