

Featured Clean Air Compressors for Food & Beverage Production
Engineered specifically to fulfill rigorous hygiene, zero-oil contamination requirements, and continuous duty cycles across food processing and aseptic bottling lines.
The Modern Imperative of Compressed Air in Food & Beverage Manufacturing
In modern food, dairy, brewery, and beverage manufacturing, compressed air is universally recognized as the essential "Fourth Utility" following electricity, water, and natural gas. However, unlike standard heavy industrial sectors where mechanical drive power is the sole objective, compressed air within food and beverage operations often comes into direct or indirect physical contact with ingestible products, primary containers, and sterile packaging membranes.
Global food safety frameworks—including FDA Code of Federal Regulations Title 21, HACCP (Hazard Analysis and Critical Control Points), Safe Quality Food (SQF) Institute codes, and the ISO 22000 standard—mandate rigorous contaminant risk mitigation. Trace oil aerosols, atmospheric particulate ingestion, condensed moisture, and microbiological colonies inside compressed air systems can cause instant product recalls, catastrophic spoilage, and irreversible brand devaluation.
Zero Tolerance for Contamination
Mineral oils and synthetic hydrocarbons cannot be fully eliminated by downstream coalescing filters if mechanical oil seals degrade over time. Modern food processing plants are accelerating the transition to 100% oil-free screw compression systems to guarantee zero cross-contamination.
Stringent Moisture & Microbial Suppression
Relative humidity above 20% in compressed air distribution lines creates a breeding incubator for molds, fungi, and bacterial pathogens like Listeria and Salmonella. Integrated refrigeration dryers and ceramic membrane systems secure pressure dew points down to -40°C.
Deep-Dive Application Scenarios Across Food & Beverage Processing
From pneumatic ingredient conveyance to high-speed aseptic bottling, explore how intelligent compressed air engineering supports every critical stage of production.
High-Pressure PET Bottle Blow Molding
In carbonated soft drink, mineral water, and edible oil packaging, PET preforms are expanded at high speeds utilizing pressurized air between 25 bar and 40 bar. Oil-free, moisture-depleted compressed air ensures mechanical wall uniformity, crystal transparency, and zero chemical taint on the inner container walls.
Pneumatic Powder & Bulk Grain Conveying
Transferring bulk powdered milk, baking flour, granulated sugar, and spices via dilute or dense phase pneumatic conveying prevents atmospheric exposure and human handling contamination. Explosion-proof permanent magnet compressors provide consistent pressure while eliminating dust-ignition risks in combustible flour environments.
Modified Atmosphere Packaging (MAP)
Preserving snack freshness, meat preservation, and ready-to-eat salad shelf-life requires flushing packages with high-purity food-grade Nitrogen (N2). Compressed air systems feed Pressure Swing Adsorption (PSA) nitrogen generators, where oil-free input prevents adsorption sieve poisoning.
Aseptic Filling, Capping & Can Seaming
Modern ultra-clean dairy and fruit juice bottling machines utilize sterile air blankets to create positive pressure zones inside isolator cabinets, preventing ambient pathogen intrusion during liquid dispensing, capping, and thermo-sealing operations at cycle speeds exceeding 60,000 units/hour.
High-Speed Optical Sorting & Pick-and-Place
High-speed optical sorters utilize precision solenoid air ejectors firing milliseconds apart to remove defective coffee beans, discolored rice, or foreign objects from vibrating feed belts. Ultra-responsive pneumatic actuators demand stable pressure supply and particulate-free air to prevent valve sticking.
Fermentation Aeration & CIP System Purging
In commercial brewing, yeast cultivation, citric acid, and amino acid fermentation, massive volumes of sterile compressed air supply vital dissolved oxygen to microbial cultures. Additionally, high-velocity air purges thoroughly clear sanitary piping following caustic Clean-in-Place (CIP) wash cycles.
Technological Evolution: Smart AI Controls & Sustainable Energy Recovery
Transforming traditional compressor utility rooms into intelligent, energy-optimized air generation ecosystems designed for Industry 4.0 food manufacturing.
AI-Enabled Smart Pressure Control & Predictive Maintenance
Electricity accounts for up to 75% to 80% of an industrial air compressor's Total Cost of Ownership (TCO) over a 10-year lifespan. Operating compressed air systems at just 1 bar (14.5 psi) higher than necessary increases overall electrical power consumption by approximately 7% to 8%.
Our integrated permanent magnet variable frequency drives (PM-VFD) combine real-time load tracking algorithms with high-efficiency IE4/IE5 synchronous motors. By matching motor RPM precisely to fluctuating pneumatic demands across day/night shifts, food processors eliminate idle unload losses, smoothing plant electrical spikes and slashing overall kilowatt consumption by 30% to 45%.
Furthermore, AI-driven IoT sensors continuously monitor vibration spectra, bearing temperatures, oil filter differential pressures, and moisture levels, scheduling condition-based predictive maintenance long before any unplanned production downtime can occur.
Thermal Energy Recovery in Beverage & Dairy Processing
In standard rotary screw compression, roughly 90% to 94% of the electrical input energy is converted into heat. In food and beverage processing, where substantial thermal energy is constantly consumed for boiler feed-water preheating, pasteurization, wash-down sanitation, and space heating, this excess heat represents an immense optimization opportunity.
Equipped with specialized stainless-steel plate heat exchangers and dual-circuit fluid loops, our industrial compressor systems recover up to 80% of thermal heat energy as 70°C to 85°C sanitary hot water, directly reducing a facility’s steam boiler workload and carbon footprint.
Company Profile & Global Manufacturing Capabilities
Shanghai Honest Compressor Co., Ltd. – Delivering World-Class Twin-Screw Compressor Systems and Comprehensive Air System Solutions.
British-Owned Precision Engineering & Heritage
Shanghai Honest Compressor Co., Ltd. is a British-owned enterprise. It was founded in early 2004. The production address is located at NO. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, China. It is a large-scale manufacturing enterprise specializing in the production of twin-screw air compressors in China. At the same time, it is also an important supplier of complete air system solutions.
We provide various types of piston air compressors (low pressure, medium pressure, high pressure, oil-free air compressors), screw air compressor systems (3KW-480KW various screw air compressors, gas separation equipment, refrigerant compressors, cold dryers, filters, ceramic membrane filtration systems) and various equipment accessories and consumables.
We fully implement strict management throughout the entire manufacturing process, strictly monitor product quality and environmental protection, and the company has passed ISO9001:2015 quality management system certification.
Exceeding National Energy-Saving Standards
We pay close attention to market trends in technology research and development, stay close to the needs of users, actively absorb the advantages of domestic and foreign brand performance structures, and integrate our own features of convenient maintenance. The air compressors we produce feature more perfect structures, better performance, and significant energy saving and consumption reduction. Tested by the National Compressor Inspection Center, our energy consumption data is superior to the national energy-saving standard.
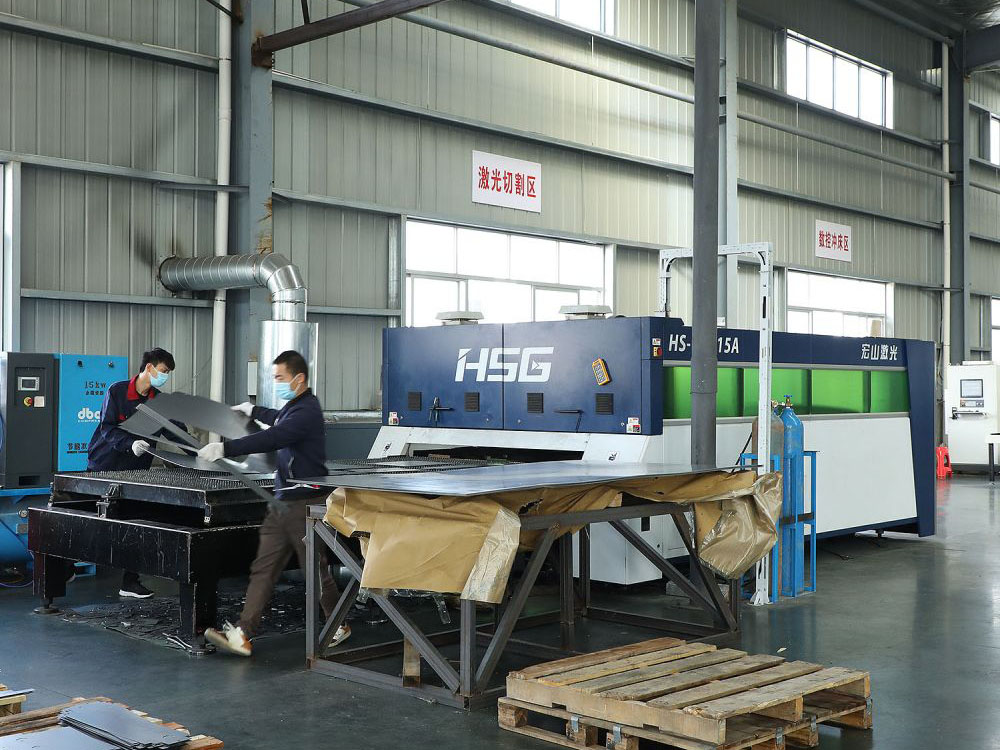
We provide users with various series of 3kW–480kW, air-cooled and water-cooled screw air compressors with a flow rate of 0.5m³/min–75m³/min. There are multiple models and categories of machines for users to choose from, as well as permanent magnet variable frequency air compressors, oil-free machines, mobile air compressors, etc. We provide a complete set of construction plans for air compressor stations including design and manufacturing, user training, support, and hosting complete service items such as overhauls.
Comprehensive Industrial Air Equipment for Food & Beverage Facilities
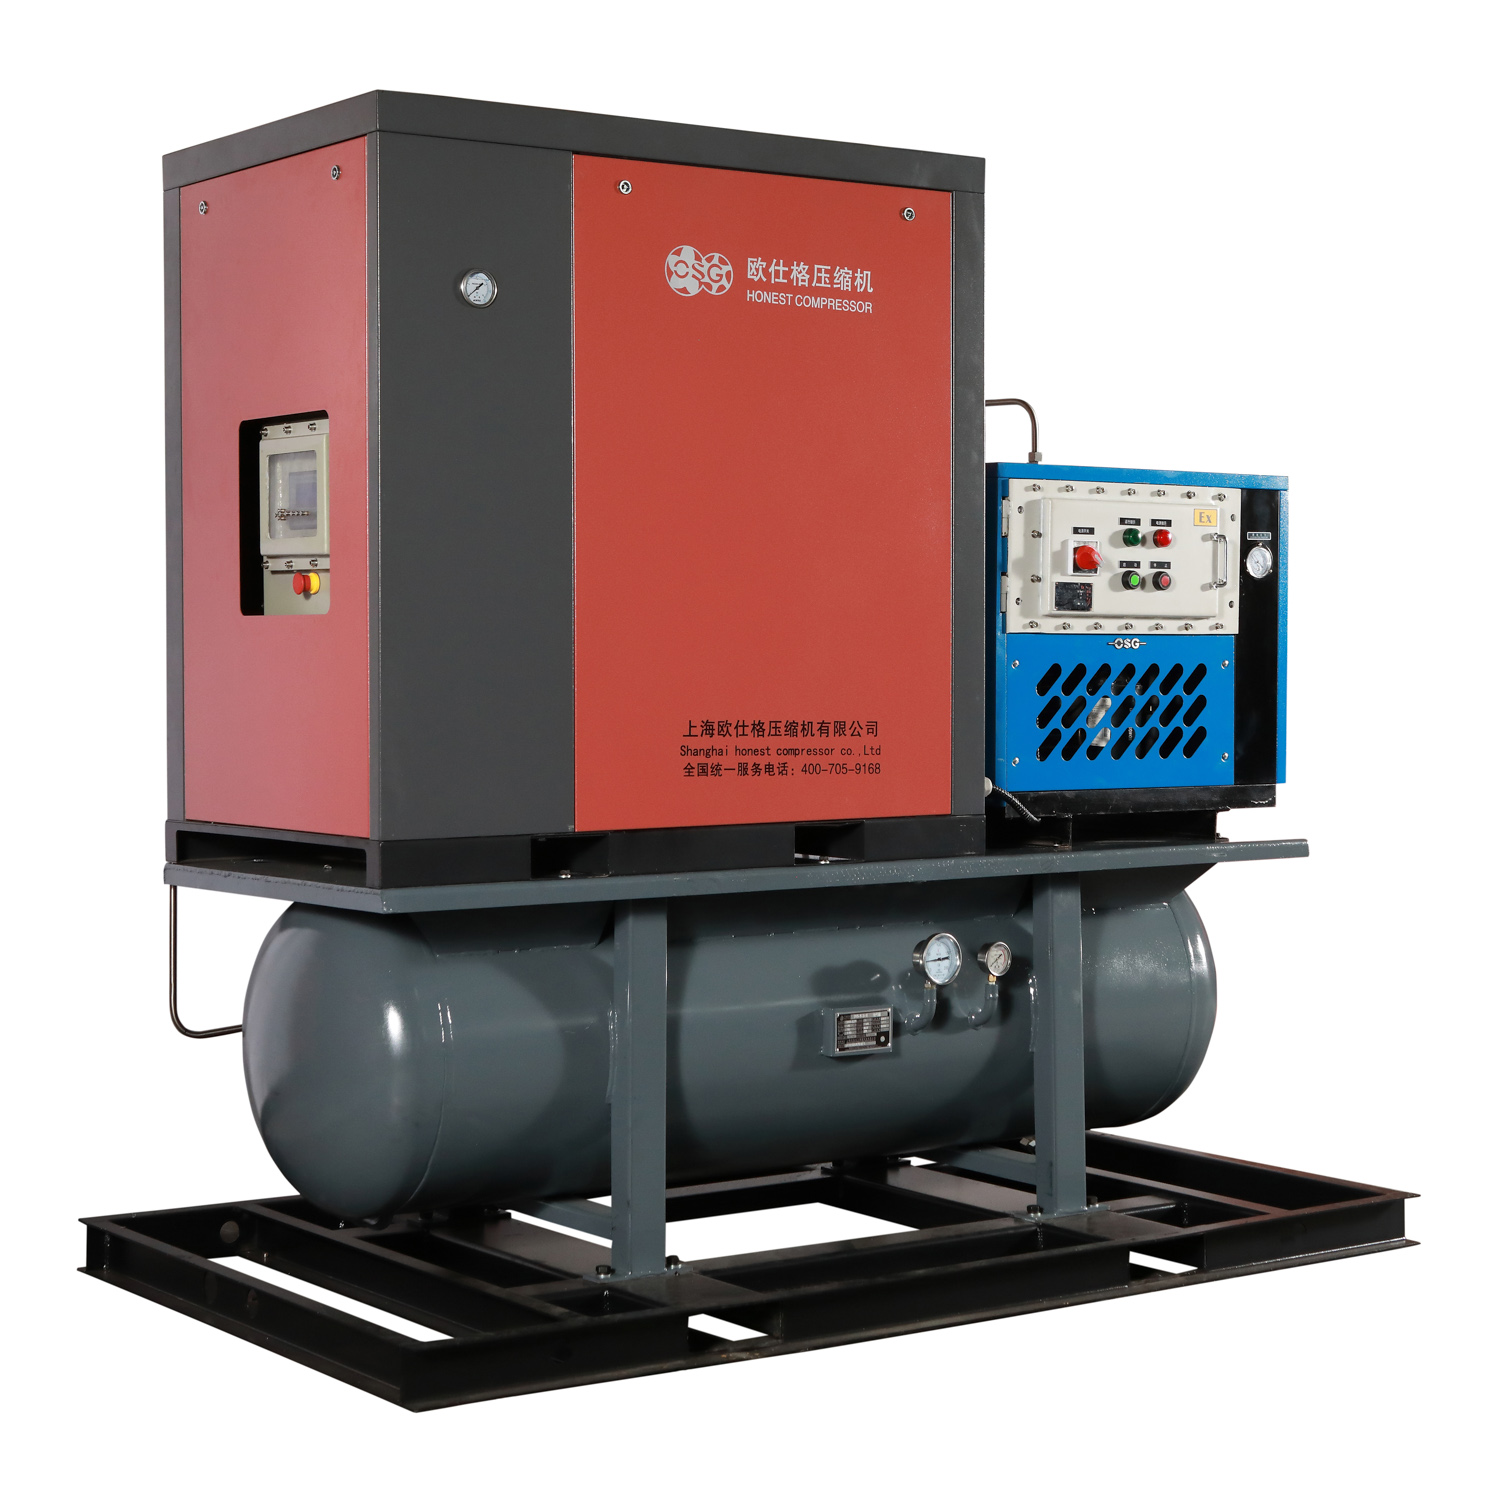
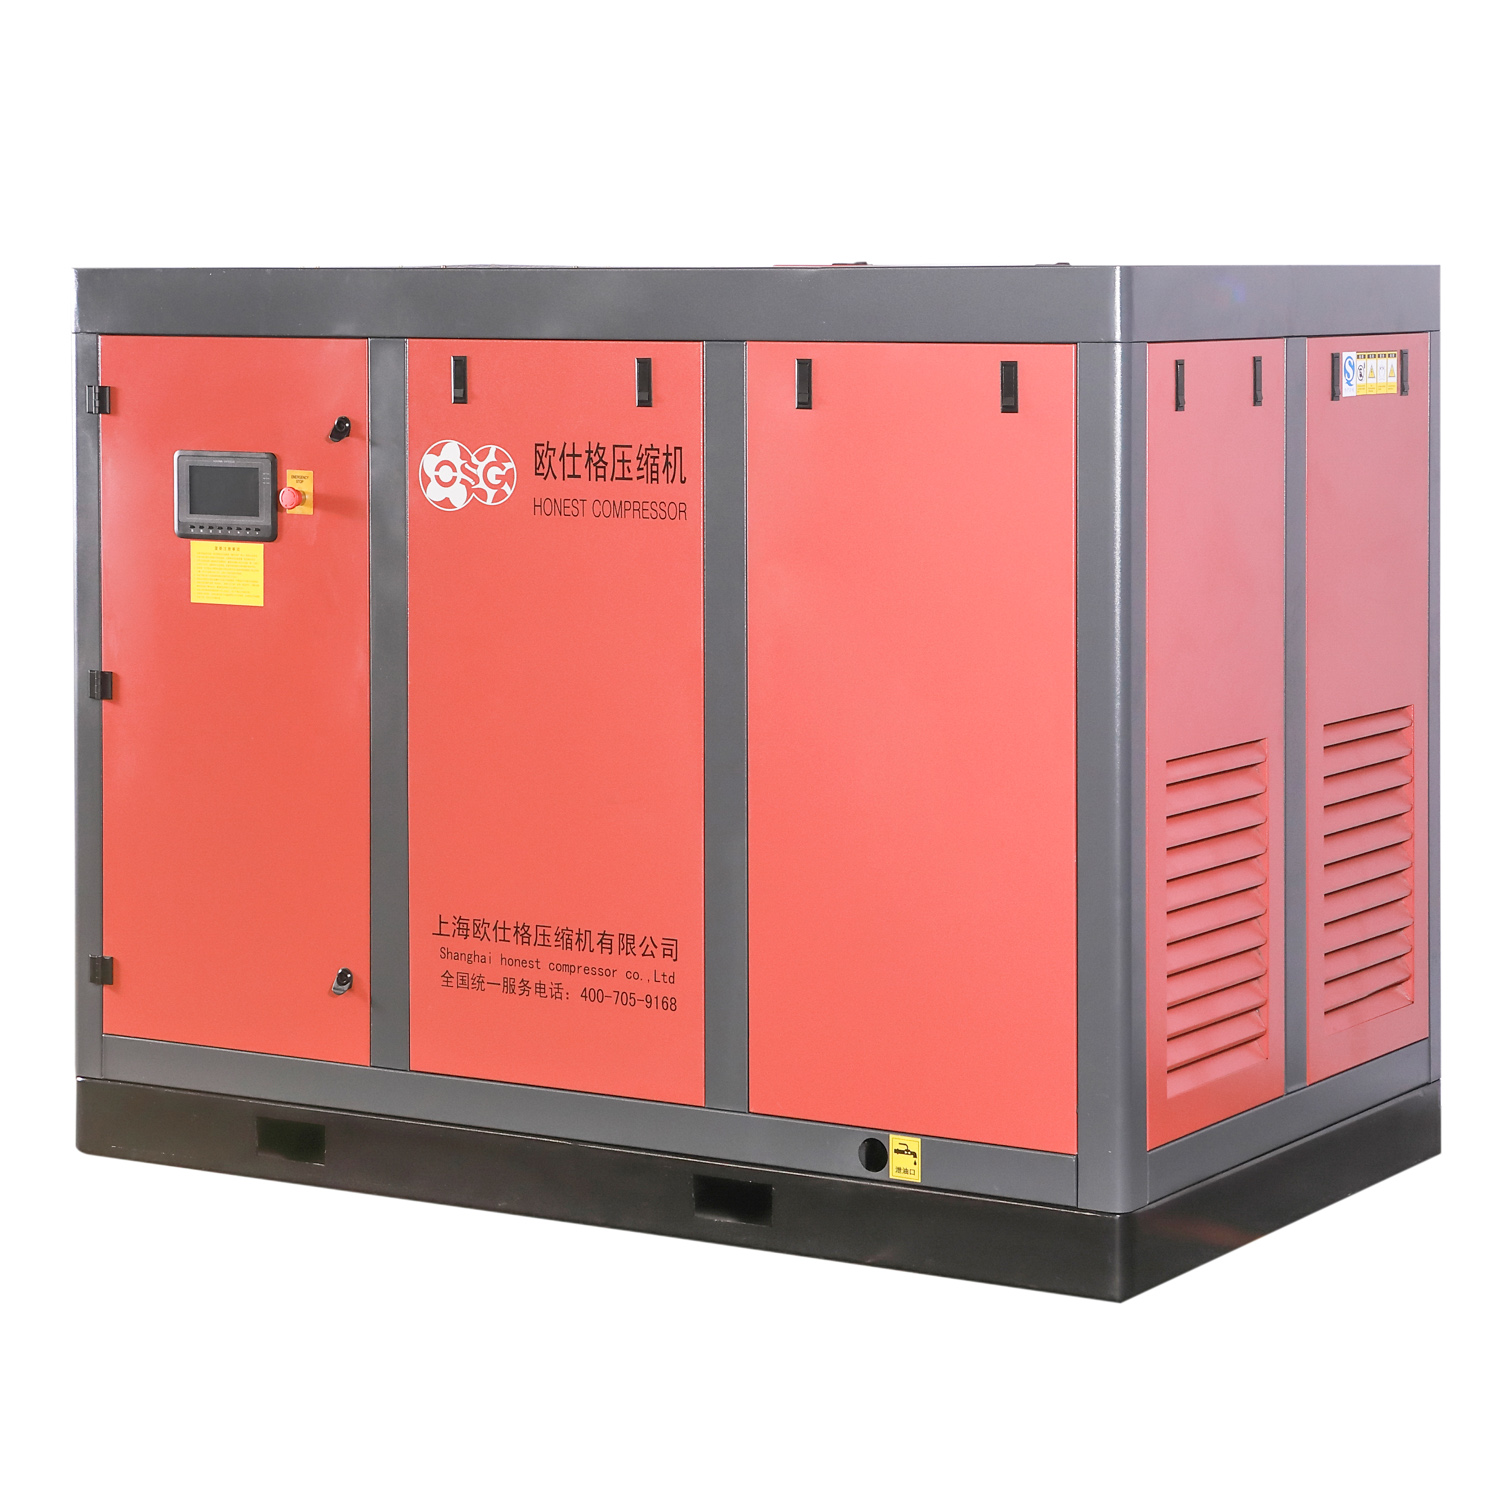
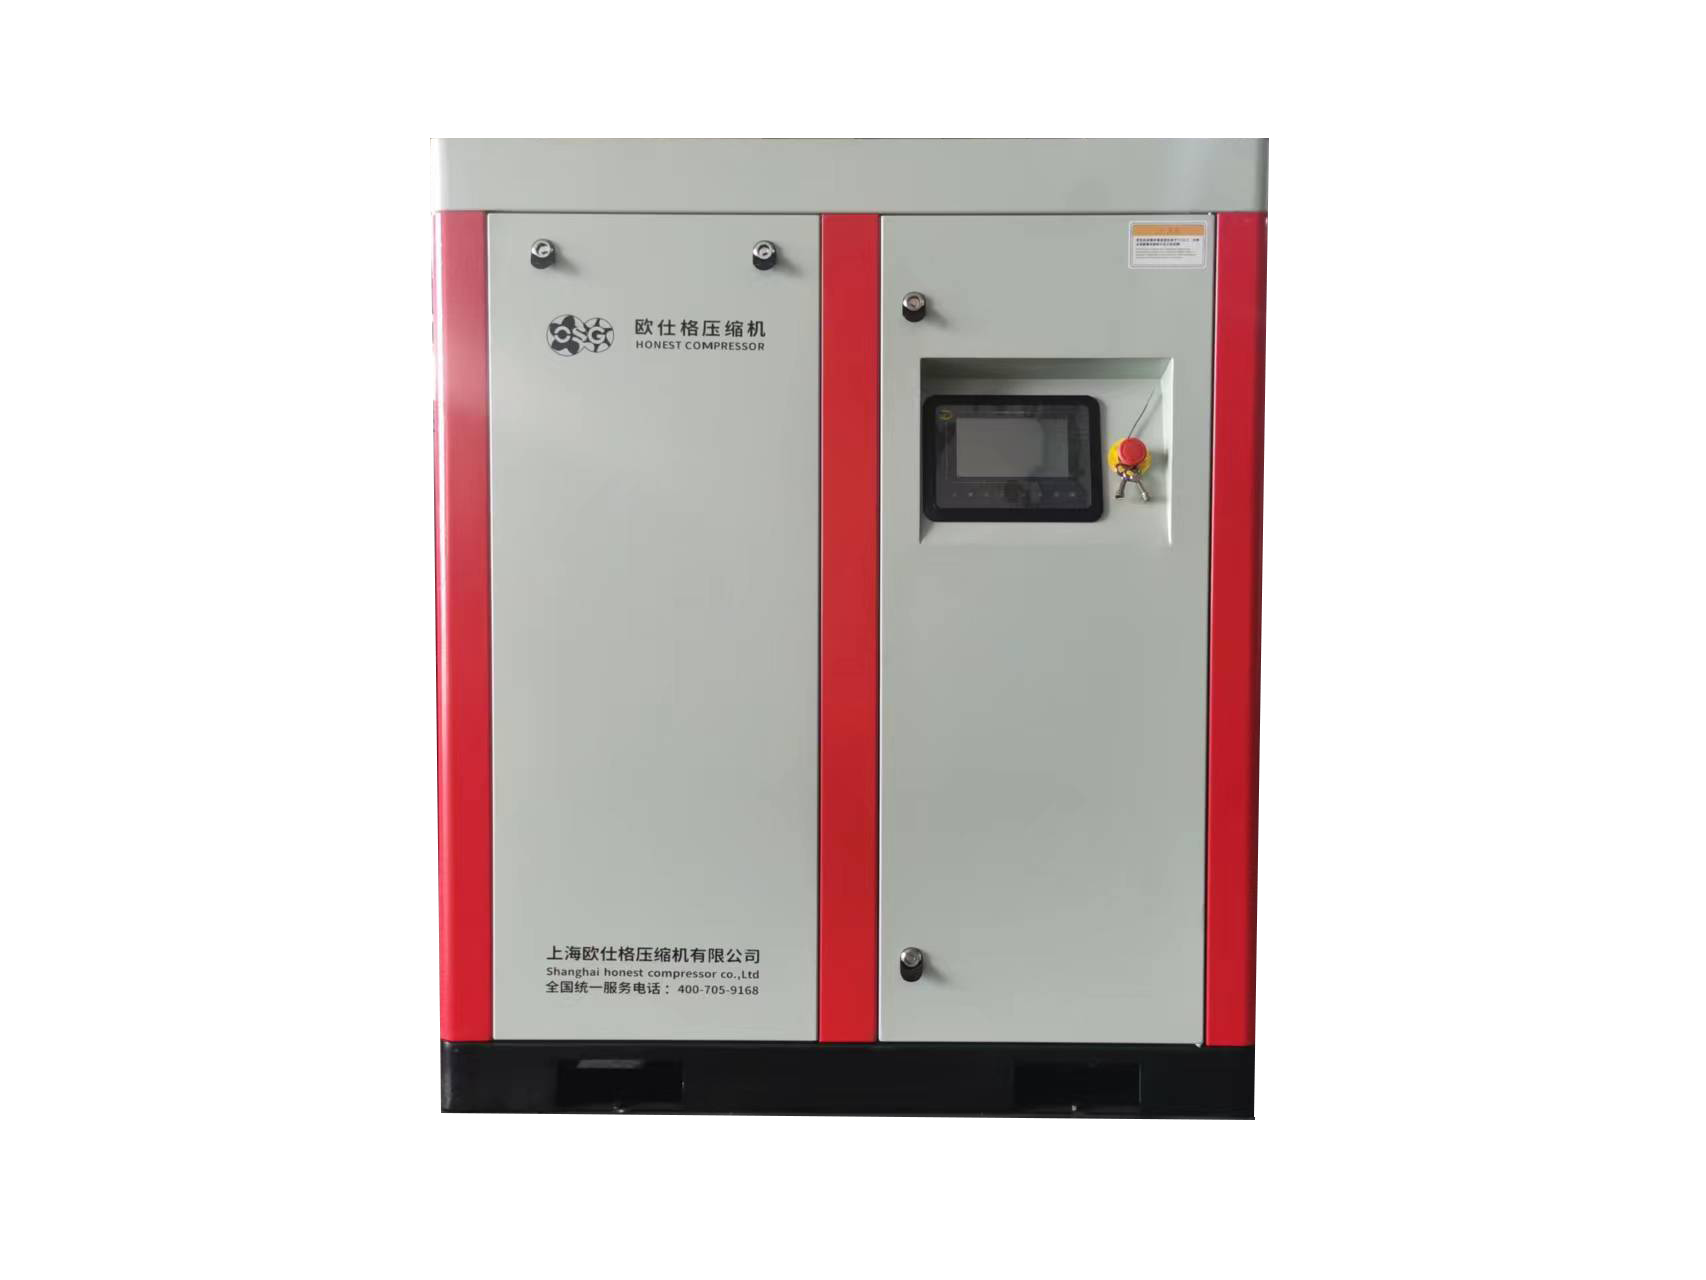
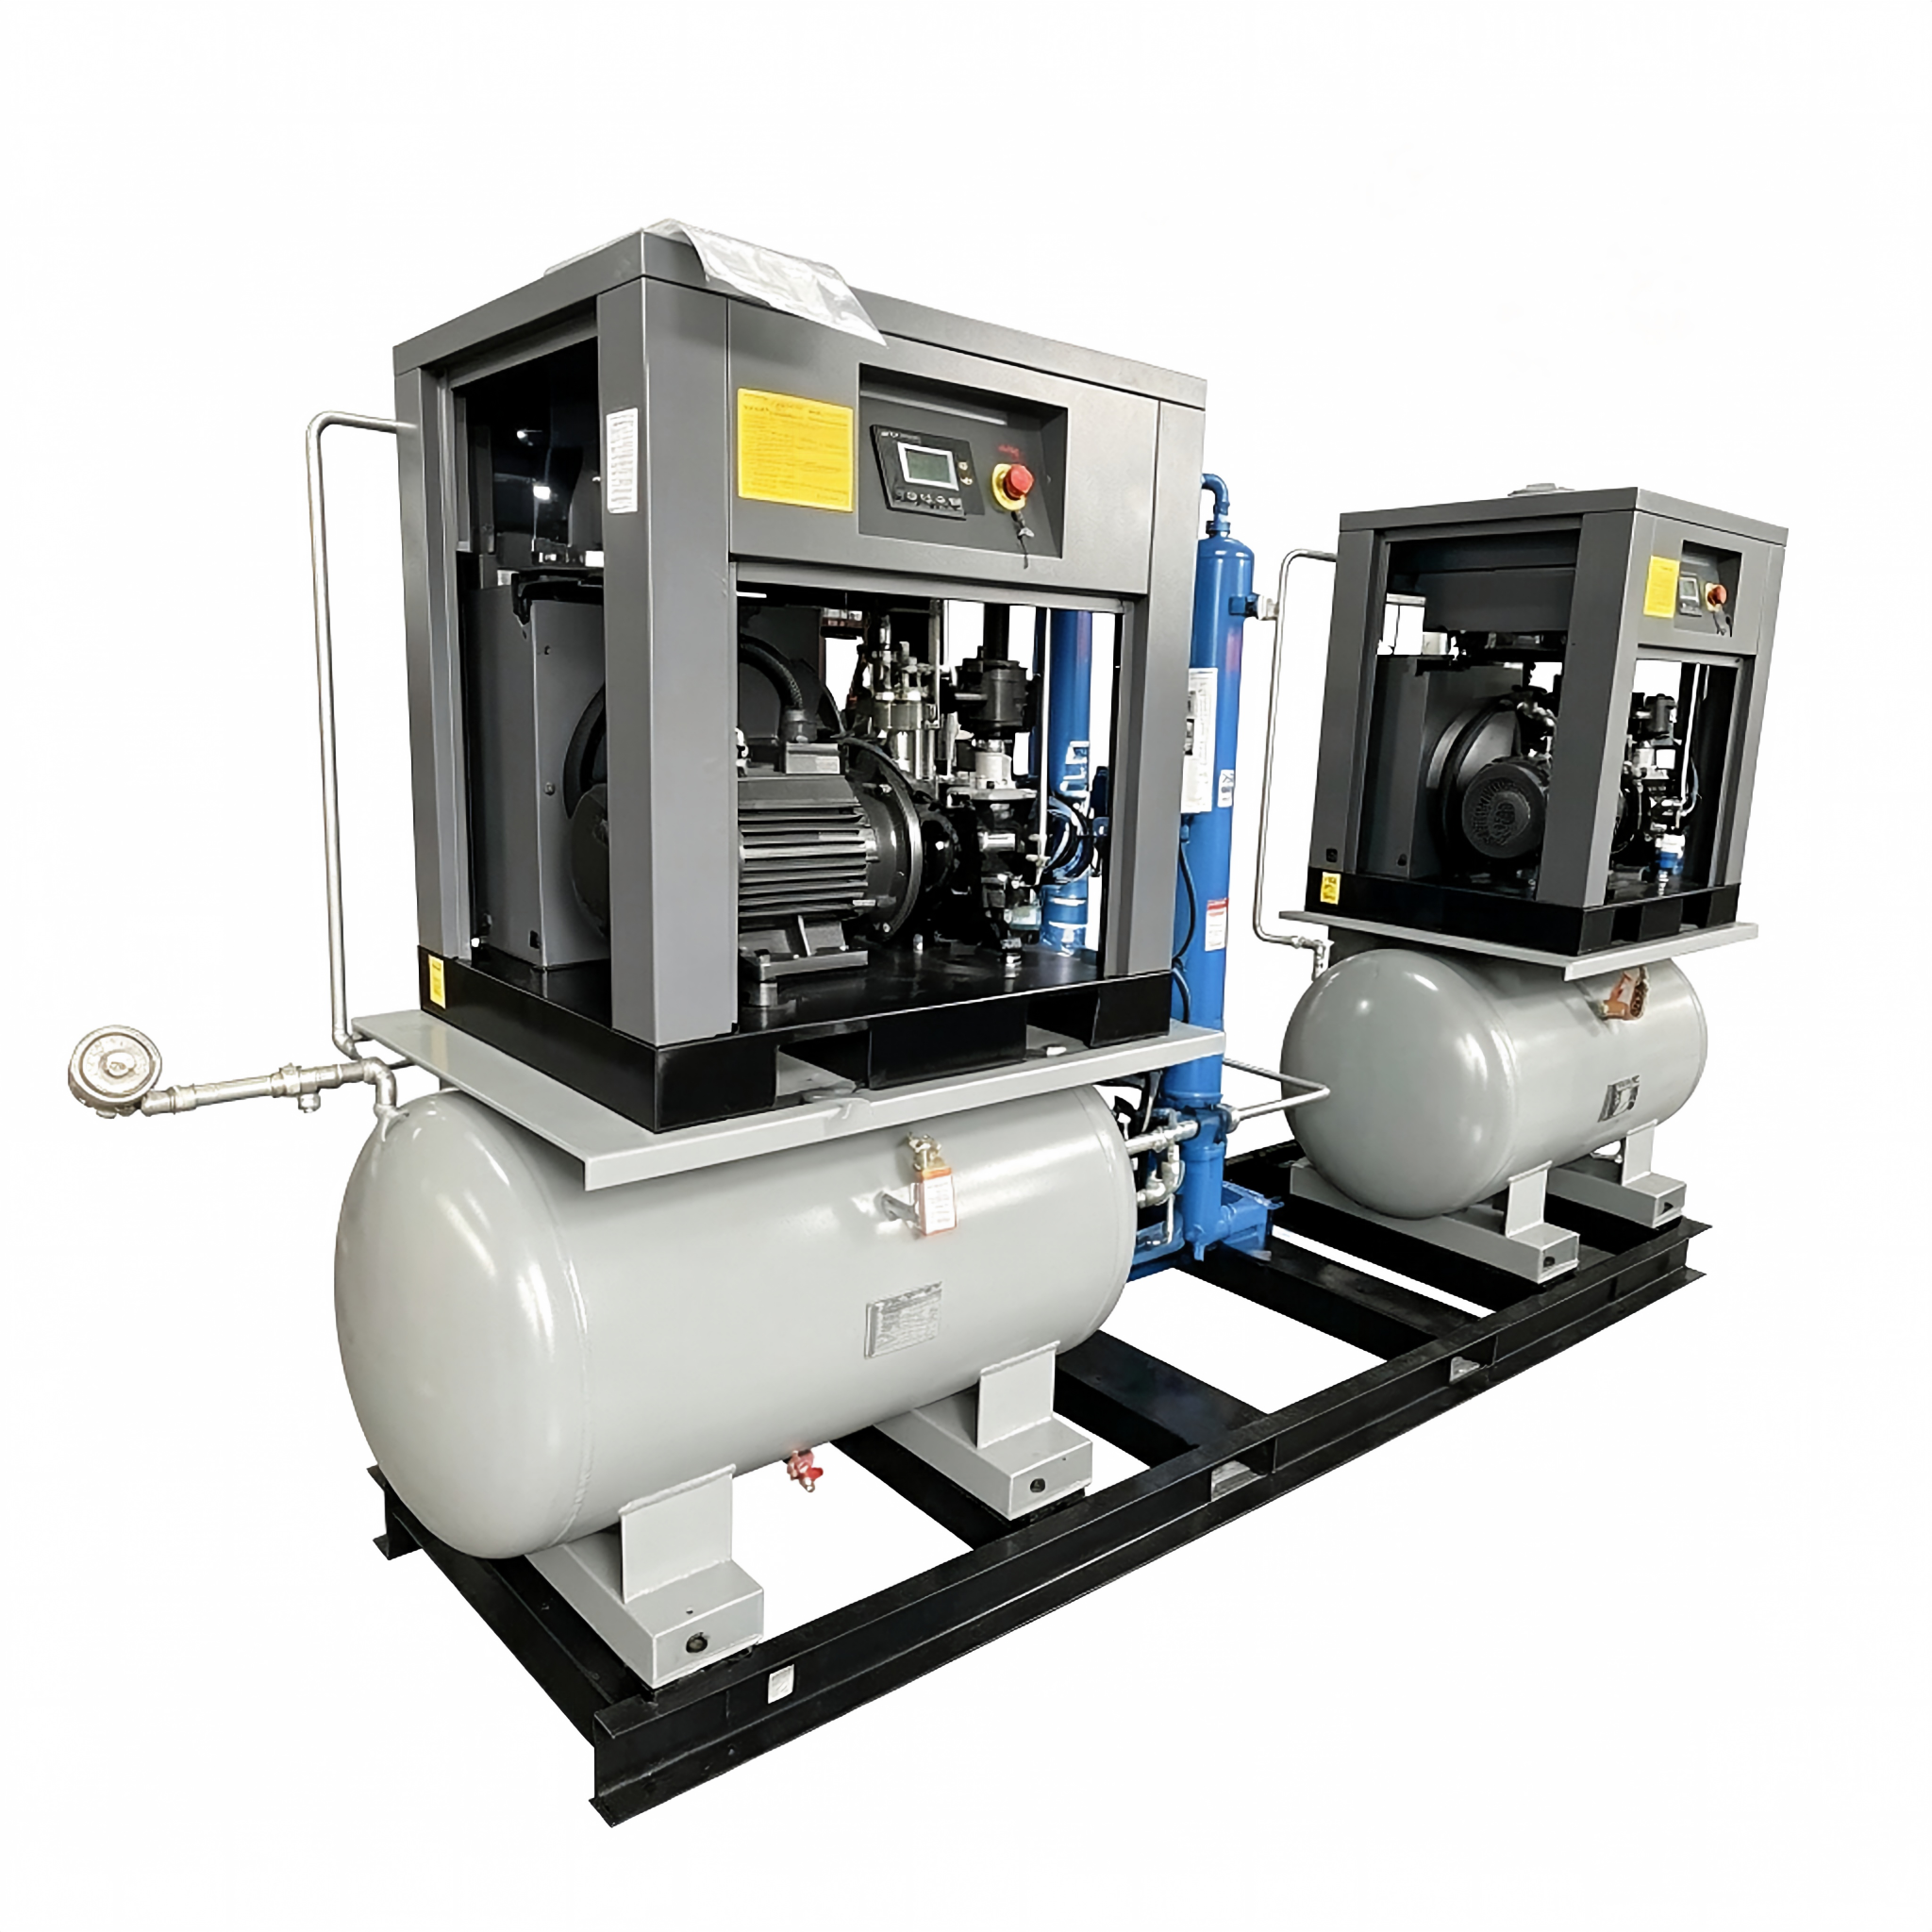
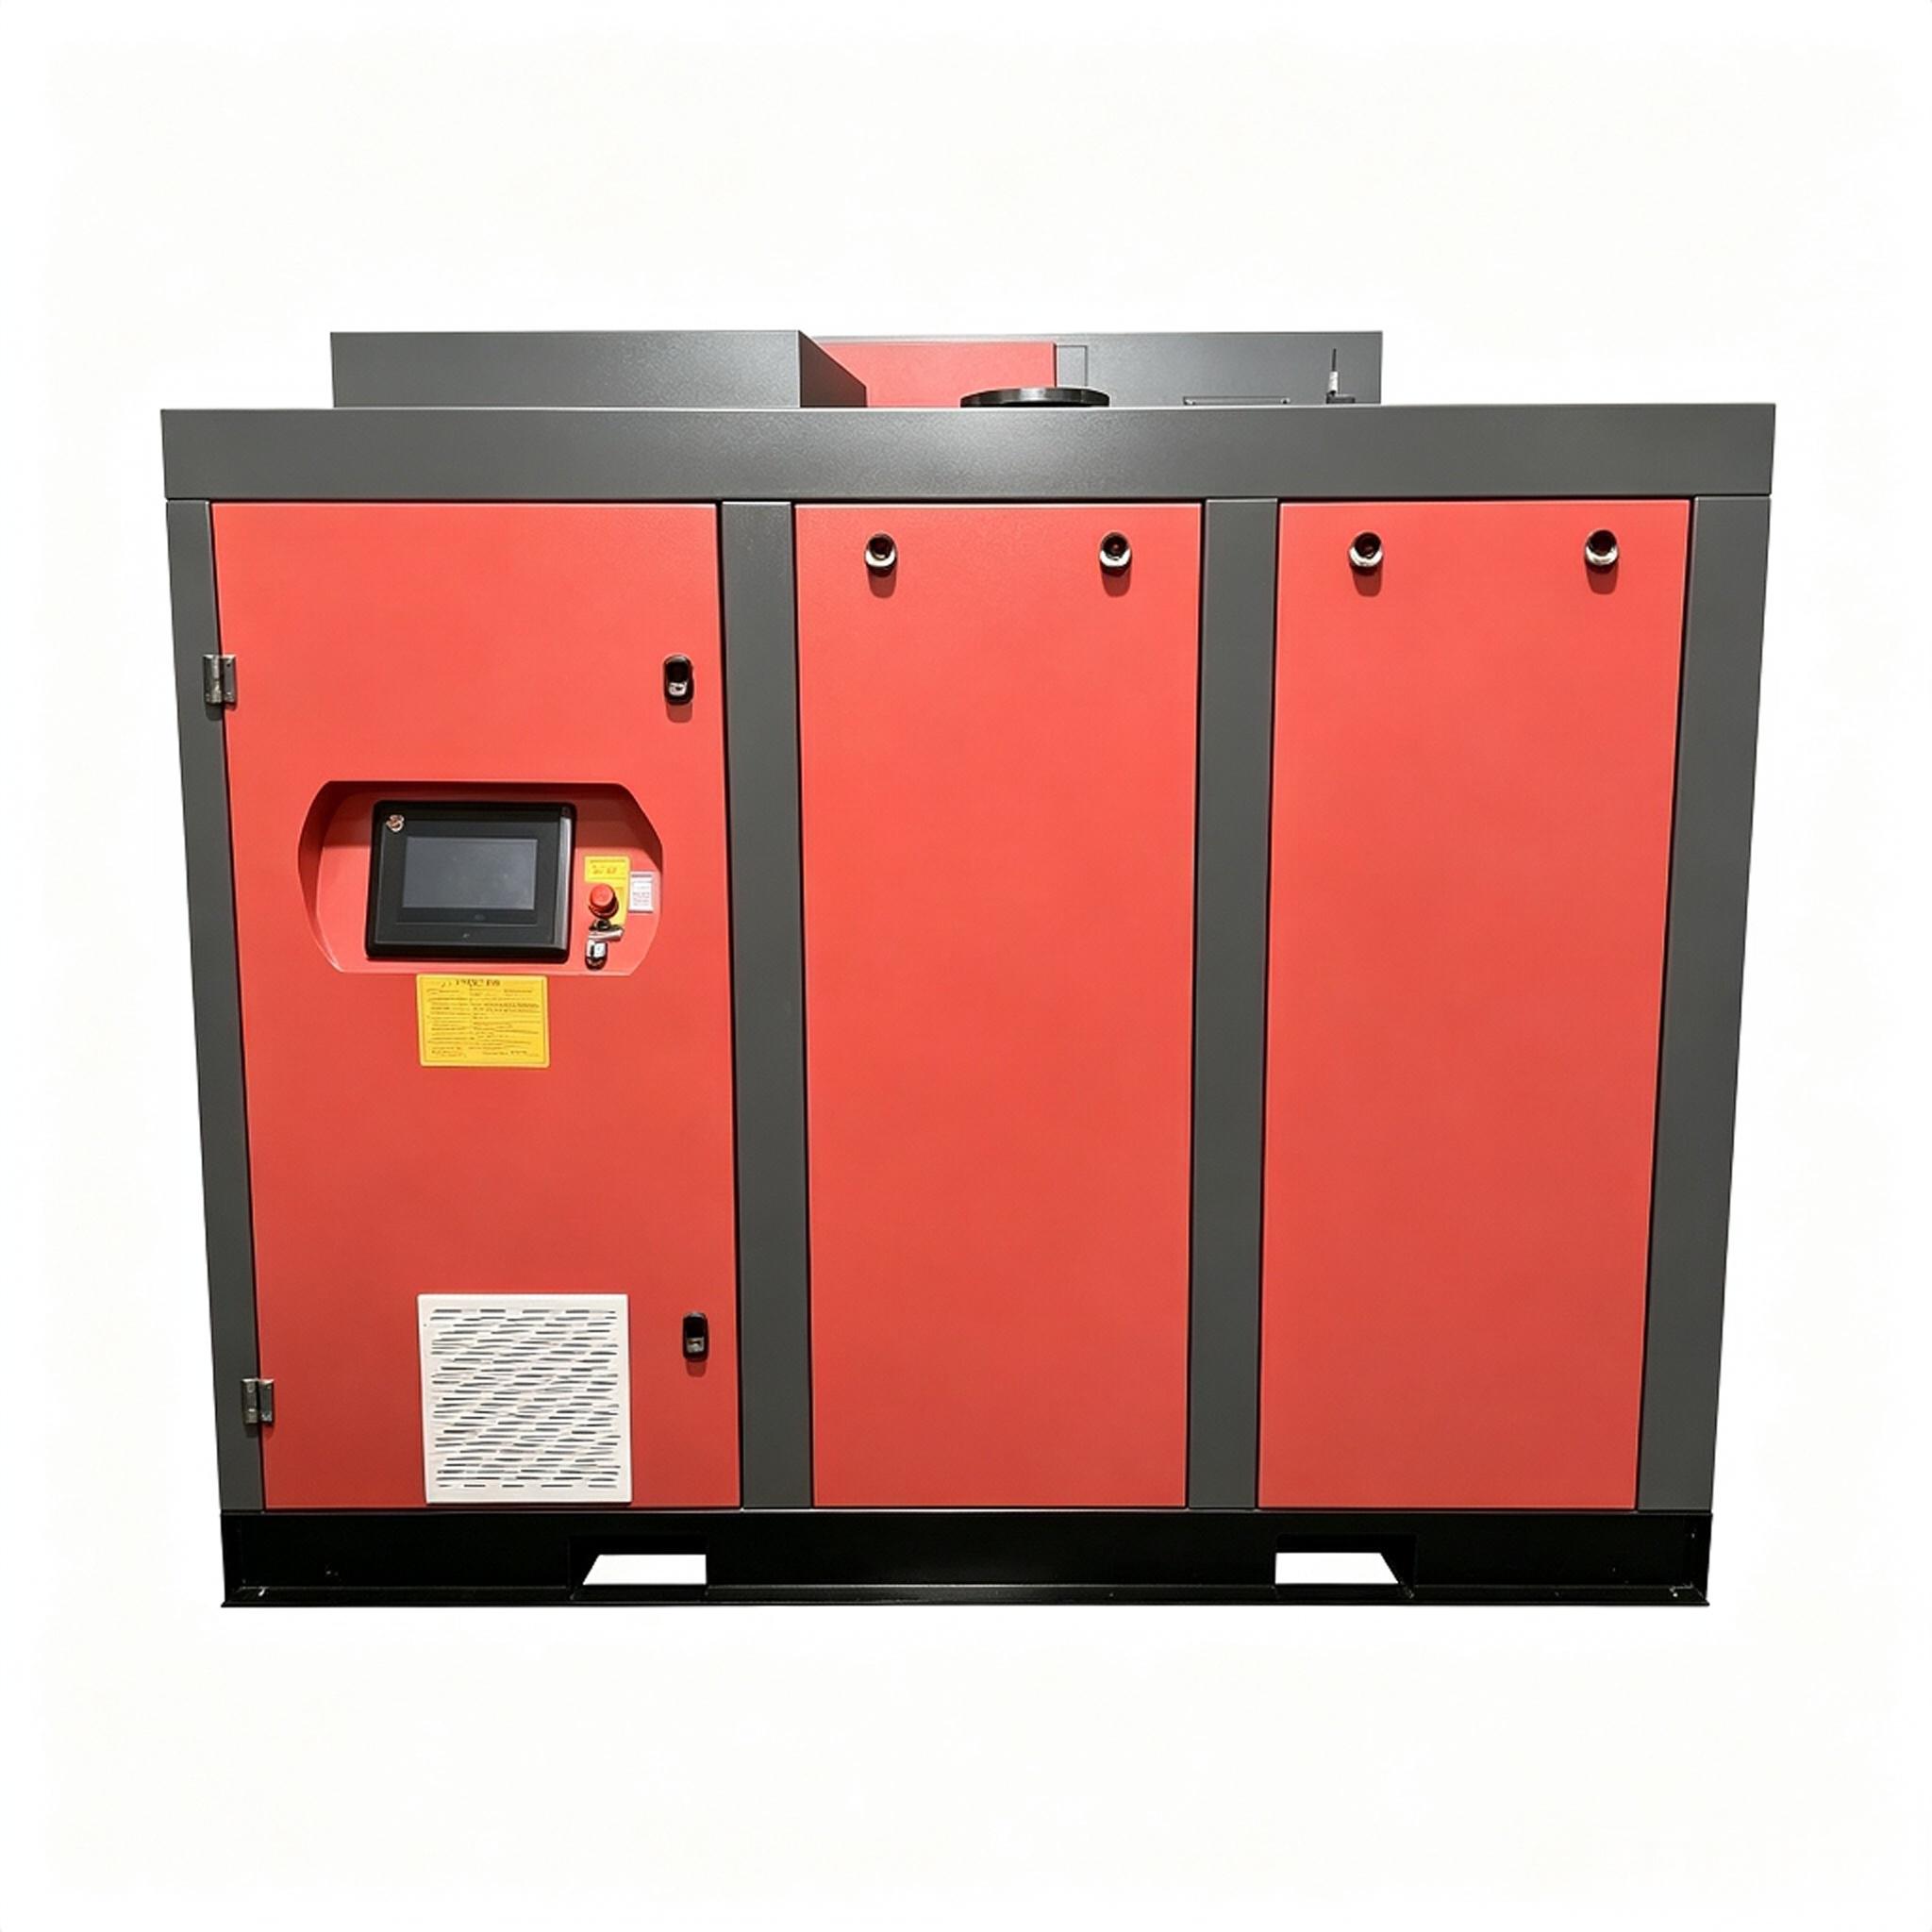
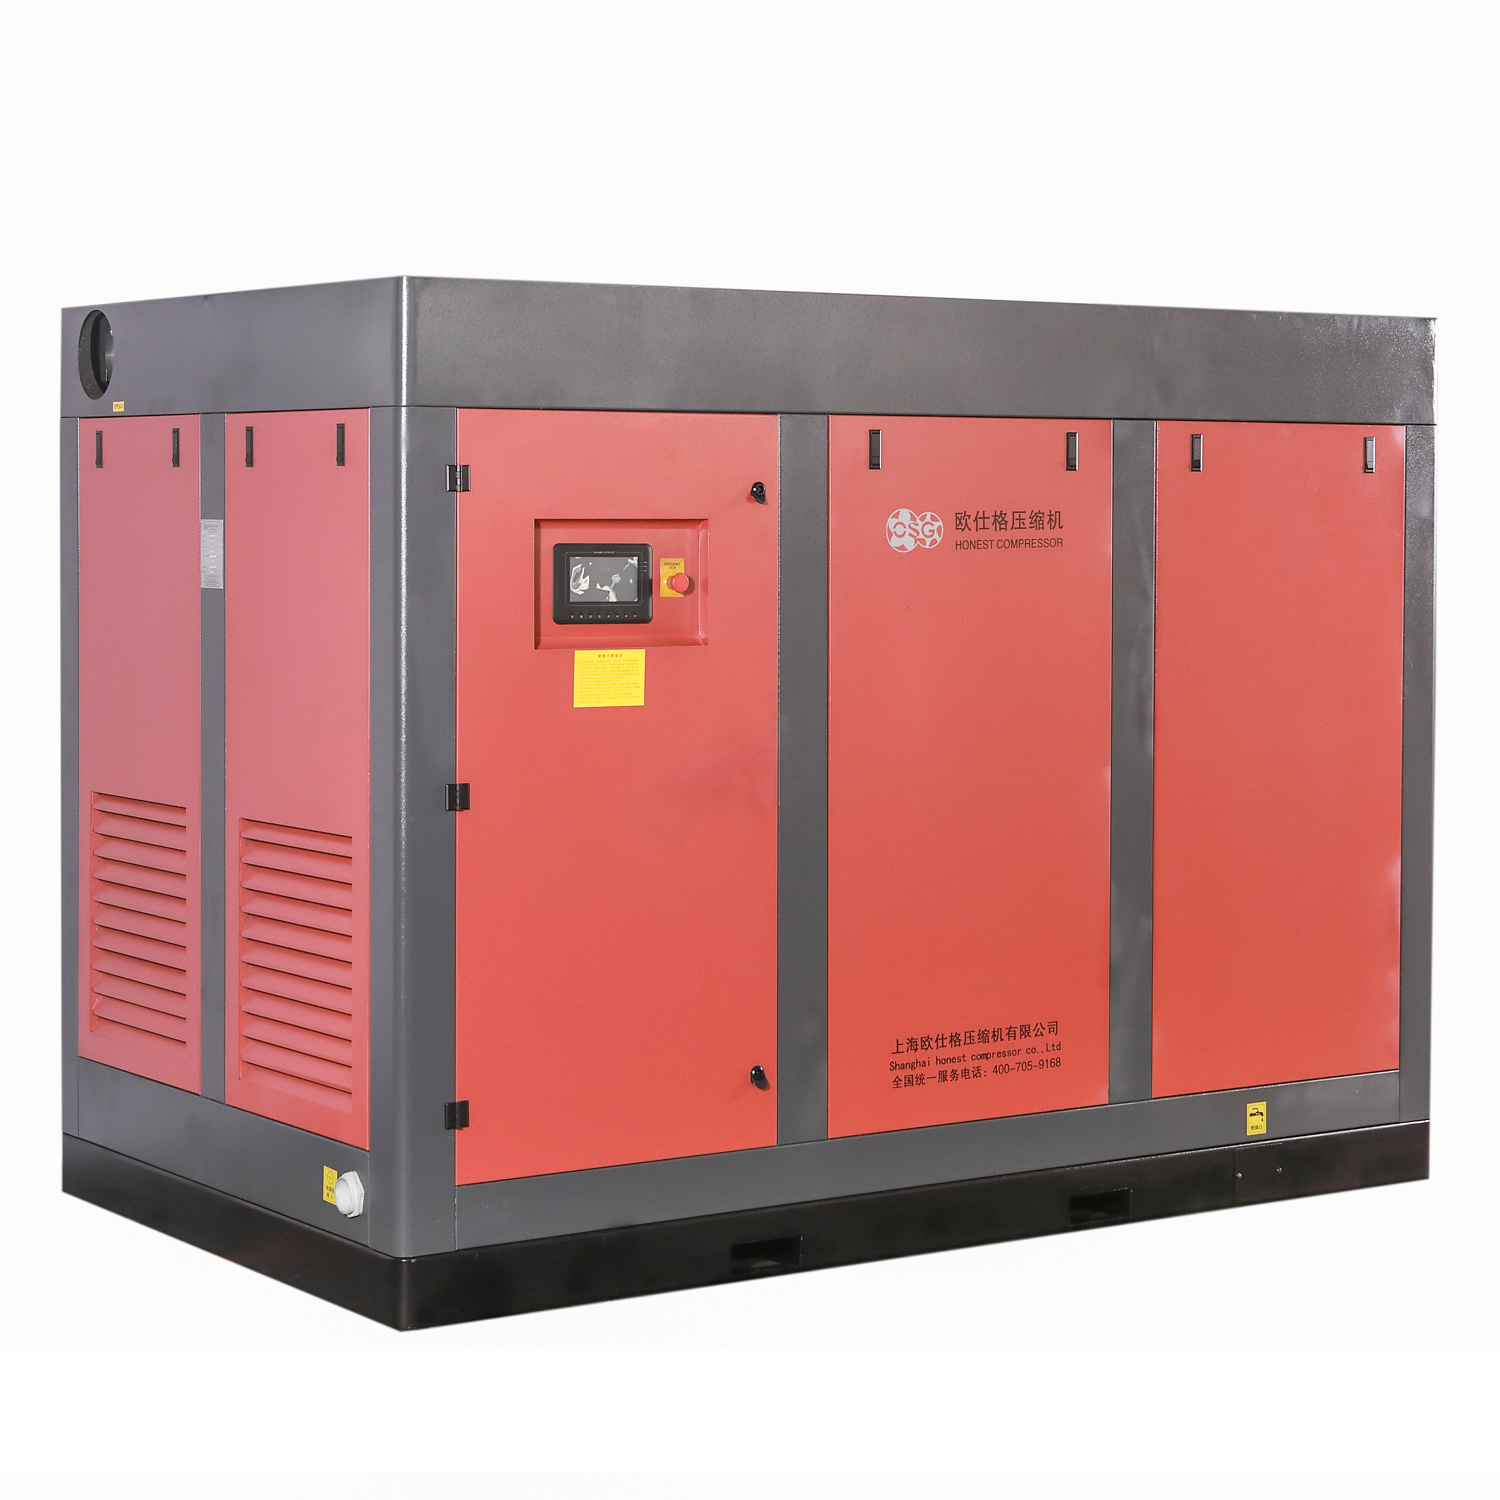
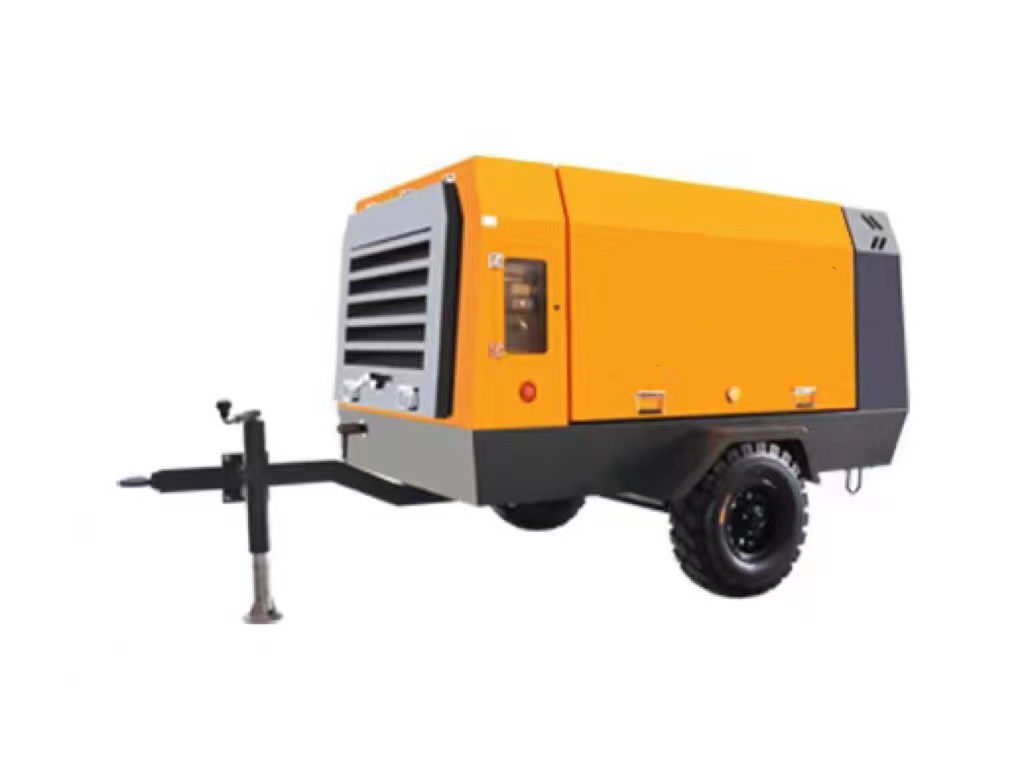
Select from our comprehensive lineup of stationary, VFD, oil-free, high-pressure, vacuum, and mobile diesel compressor units engineered to meet demanding factory environments.
Food & Beverage Compressed Air System Audit & Design Criteria
Implementing end-to-end quality assurance from air intake filtration to the point-of-use application nozzle.
1. Intake Air Quality Filtration
Food manufacturing facilities often generate ambient airborne starch, sugar, yeast, and dust. Installing multi-stage heavy-duty centrifugal pre-filters and nano-synthetic intake elements prevents micro-particles from entering the compression chamber, preserving internal air ends.
2. Condensate Drainage & Drying
Liquid water in air headers creates microbial breeding grounds. Utilizing zero-loss electronic level-sensing condensate drains paired with combination refrigerated/desiccant adsorption dryers ensures that moisture is ejected without releasing pressurized air waste.
3. Sanitary Piping Networks
Black iron and galvanized pipes corrode over time, flaking scale particles into sensitive packaging machinery. We advocate for modular anodized aluminum or 304/316L stainless steel air distribution loops with zero laminar flow dead-legs to prevent bacterial stagnation.
Whether retrofitting an existing food processing facility or designing an entirely new greenfield beverage plant from the ground up, Shanghai Honest Compressor Co., Ltd. provides complete customized system planning, energy audits, turnkey equipment integration, and lifecycle maintenance guarantees.