

Engineered Compressors for Laser Cutting Systems
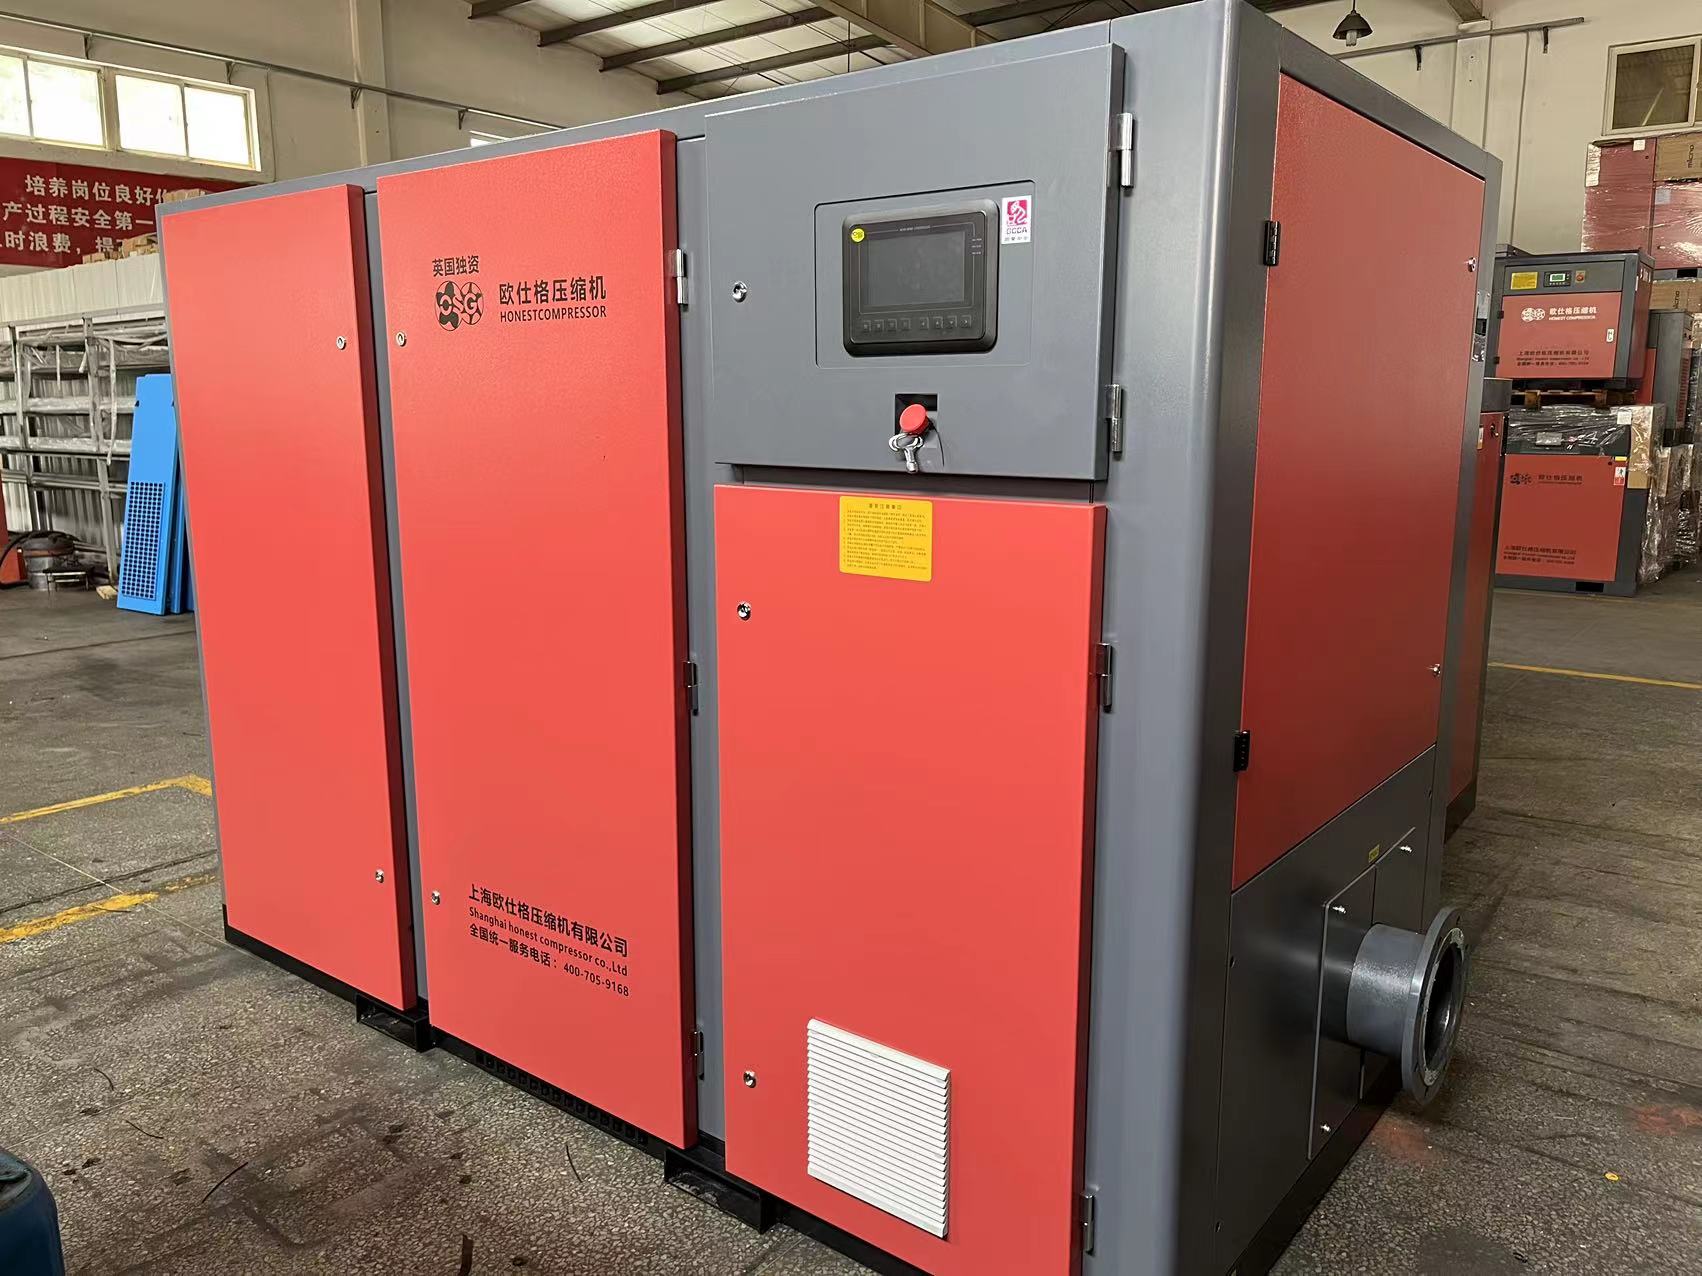
Premium energy-saving screw compressors integrated with high-efficiency refrigeration dryers and precision filtration designed specifically for fiber laser assist gas demands.
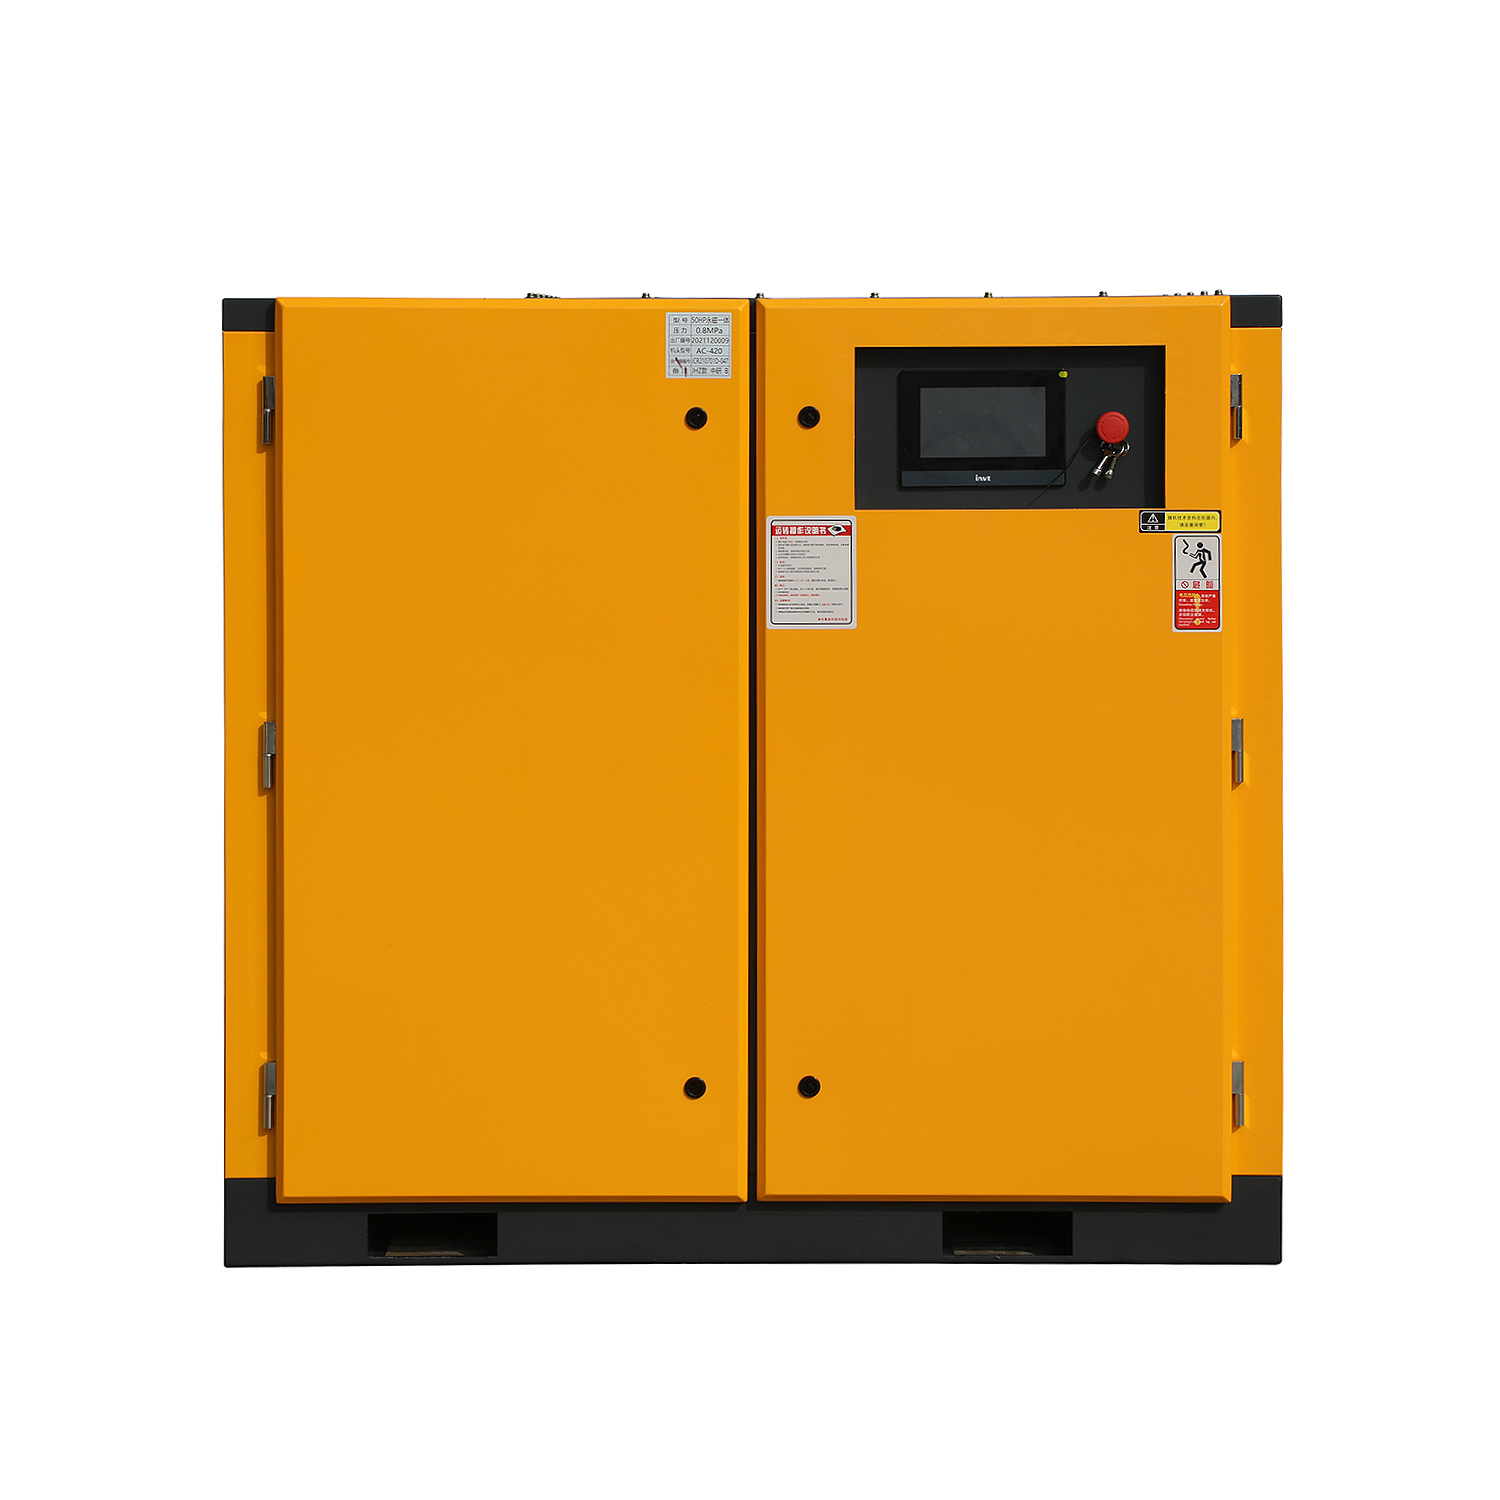
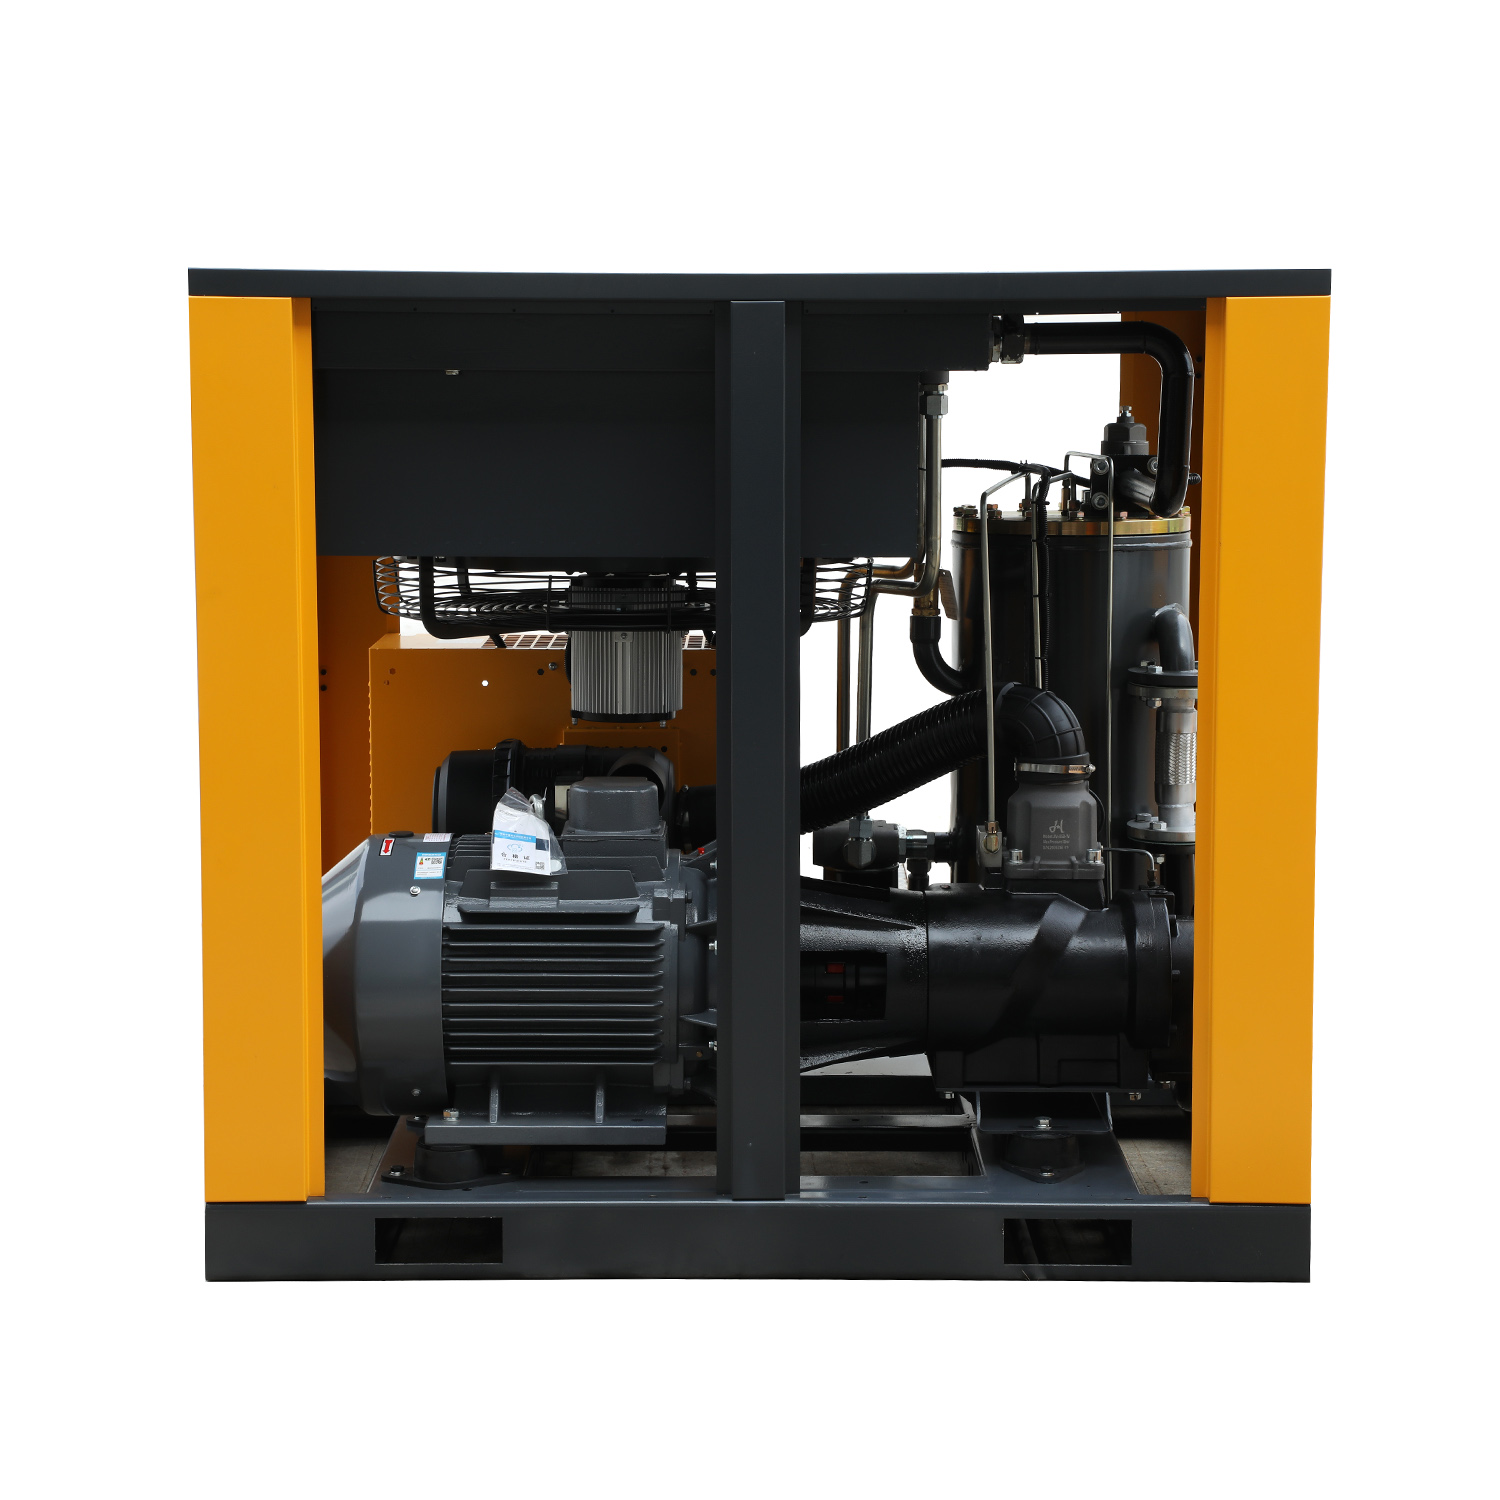
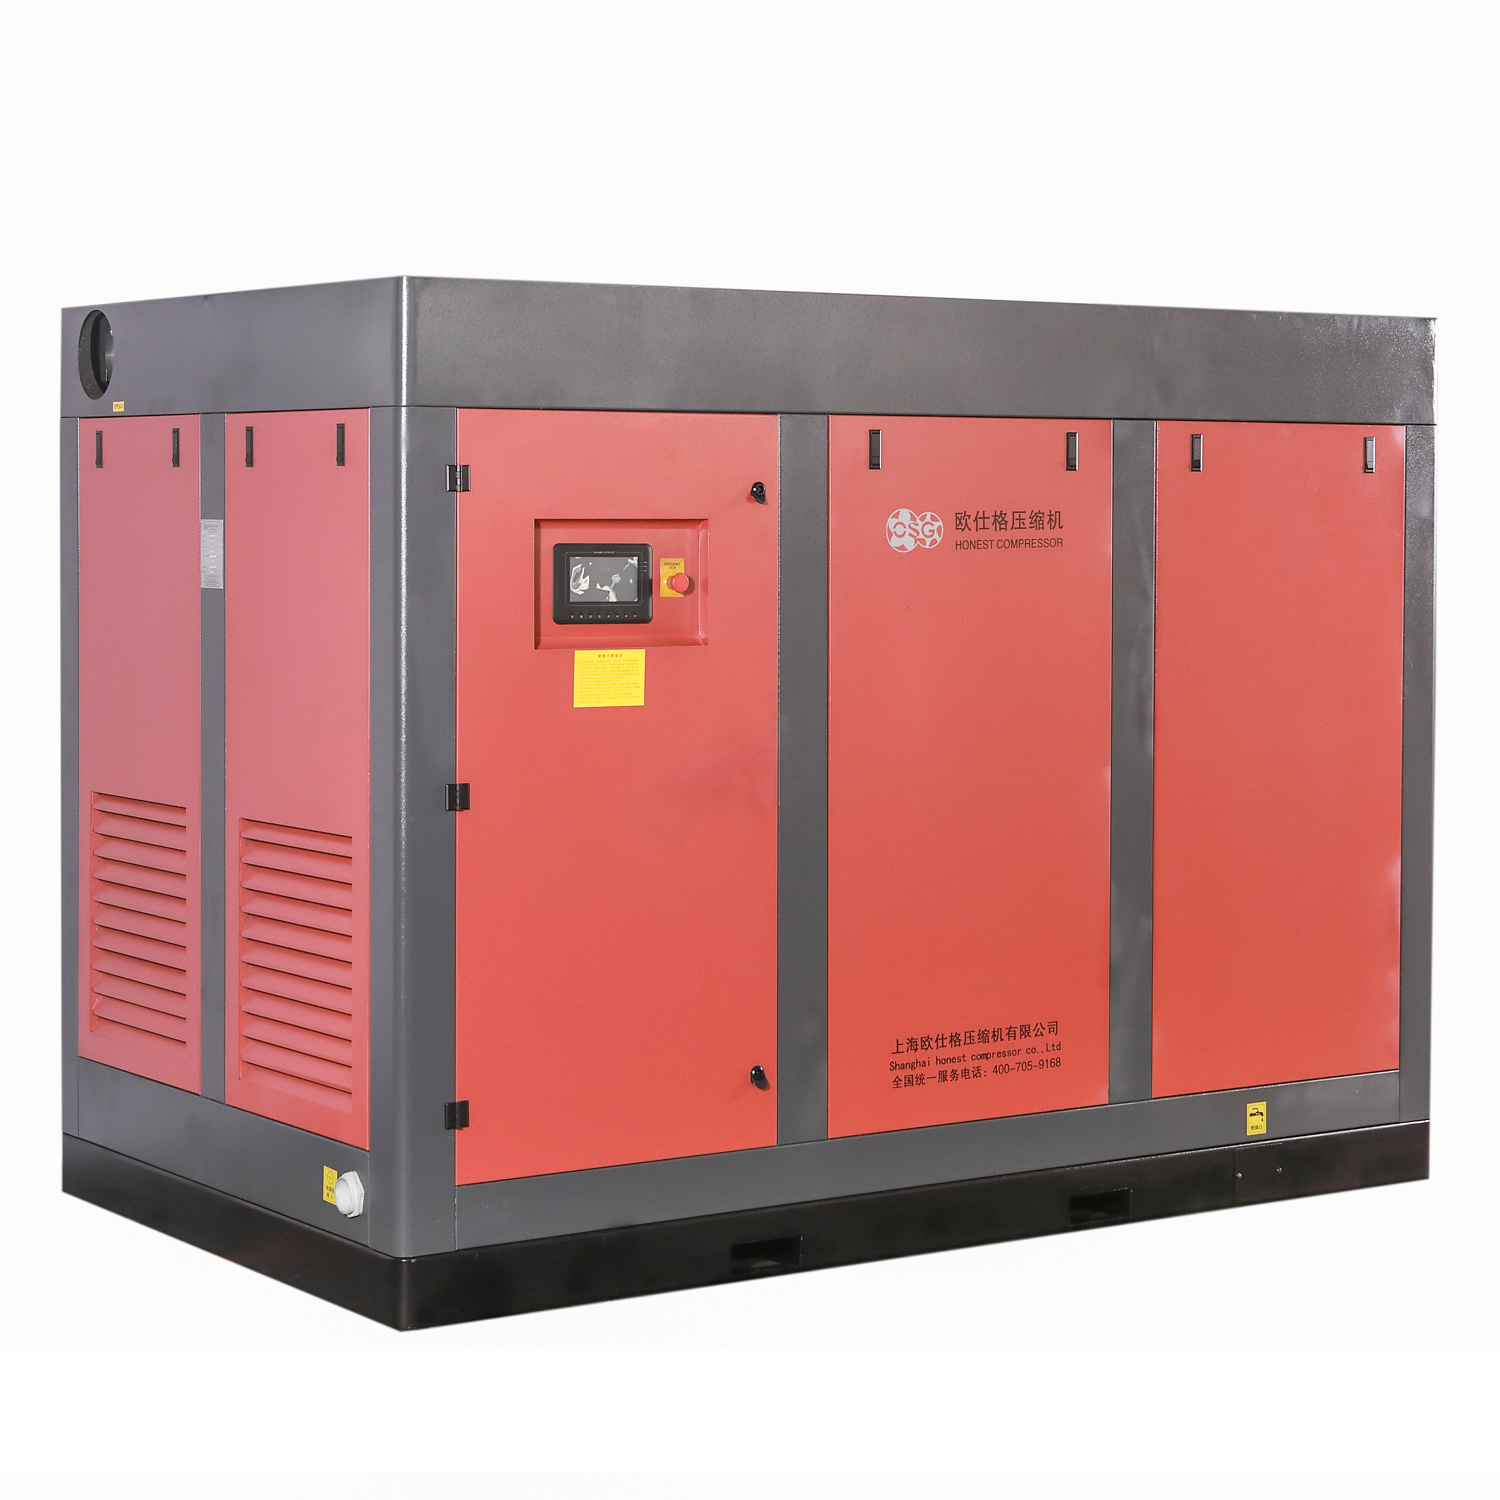
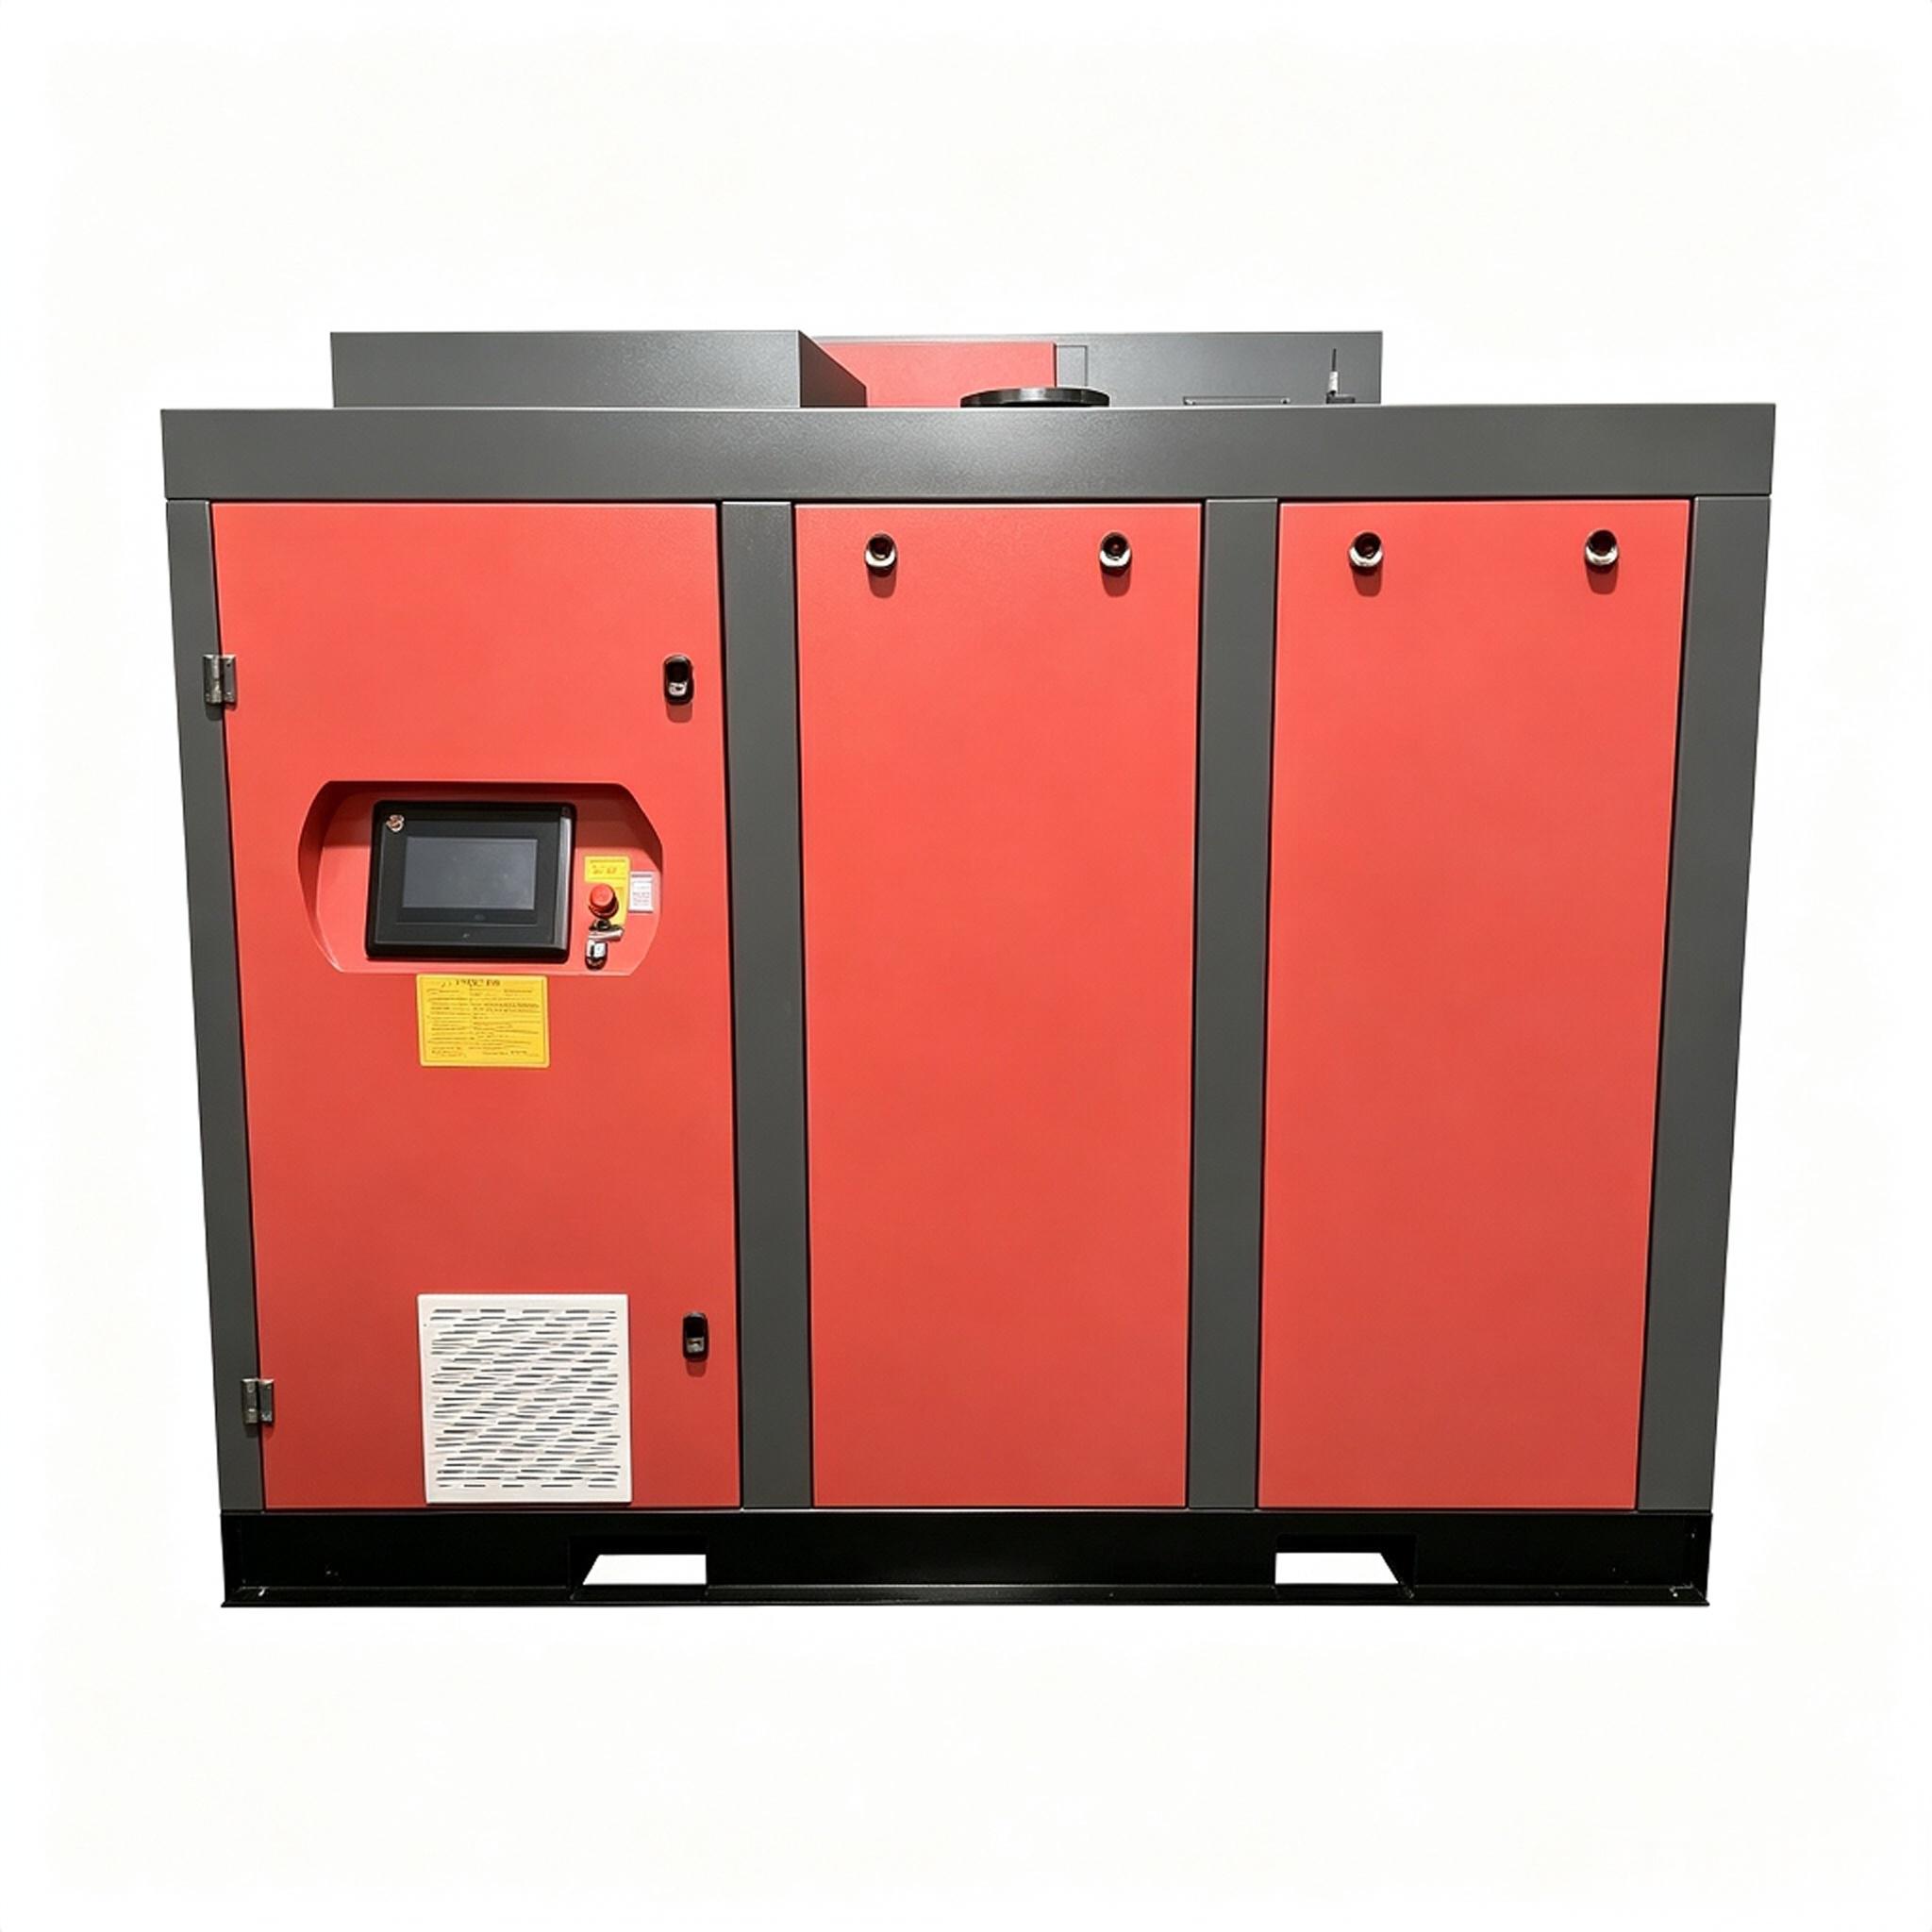
Industrial Transformation: The Rise of Compressed Air in Modern Laser Cutting
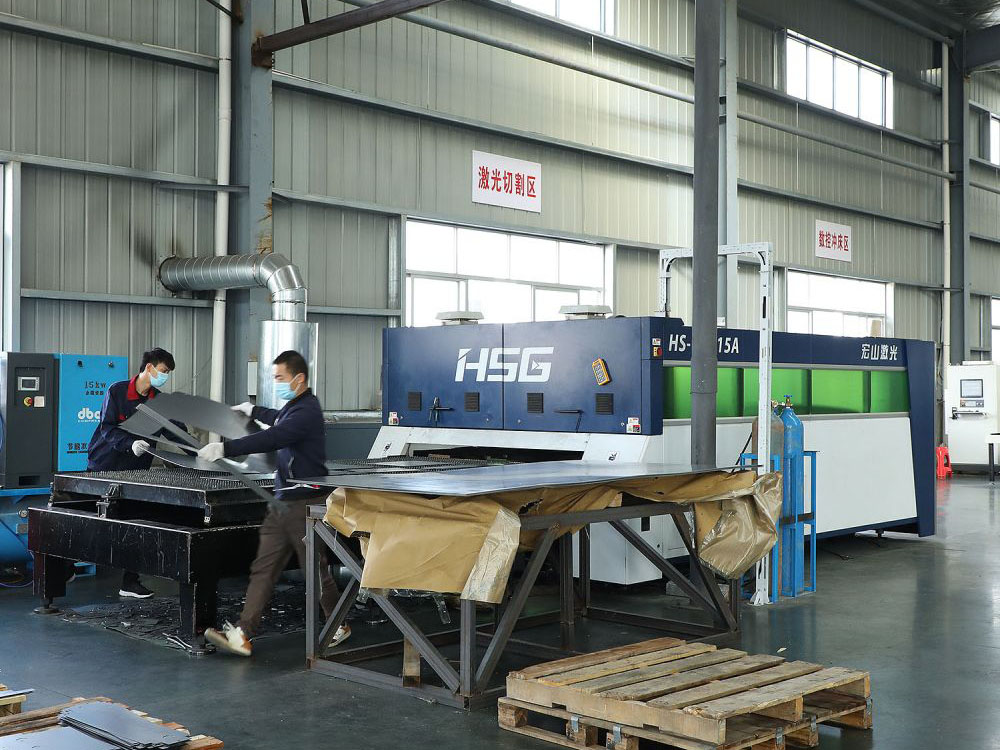
In modern industrial sheet metal fabrication, fiber laser cutting technology has evolved from low-power (1kW–4kW) to ultra-high-power systems ranging from 12kW, 20kW, 30kW up to 60kW. Historically, fabricators relied exclusively on bottled or liquid Nitrogen (N2) for clean oxide-free cutting and Oxygen (O2) for exothermic mild steel cutting. However, liquid nitrogen represents an enormous ongoing operational cost, often accounting for 50% to 70% of the entire laser processing overhead.
This economic challenge has driven the massive industrial transition toward High-Pressure Rotary Screw Compressors integrated with Air Dryers and Multi-Stage Filtration Systems. Compressed air contains approximately 78% Nitrogen and 21% Oxygen. When compressed to 16–30 bar and purified down to ISO 8573-1 Class 1.2.1 standards, shop-generated dry compressed air delivers cutting speeds up to 1.5–3 times faster than pure nitrogen on thin-to-medium gauge carbon steel and stainless steel, while reducing gas costs by an astounding 85% to 92%.
Drastic Cost Reduction
Eliminate expensive liquid cylinder refills, bulk tank vapor loss, and tank rental fees. Producing compressed air on-site typically costs less than $0.10–$0.25 per cutting hour, compared to $5.00–$15.00 per hour with liquid nitrogen.
Optic Protection & Purity
Integrated refrigerated dryers, dual desiccant columns, and 5-stage micro-coalescing filters ensure a pressure dew point of +2°C to -40°C and zero residual oil vapor, preventing lens contamination and optical thermal lensing.
Higher Cutting Speeds
The 21% oxygen content in dry compressed air provides a controlled exothermic boost during cutting. This reaction elevates processing velocity across mild steel, galvanized plate, and aluminum alloys without burrs.
Air Quality Requirements for Fiber Laser Systems: ISO 8573-1 Standards
Fiber laser cutting heads contain high-precision optical components, including quartz protective windows, collimating lenses, focusing lenses, and ceramic nozzles. A single droplet of oil or condensed moisture striking the laser protective lens under high-power (e.g., 20,000W) laser radiation will cause immediate beam absorption, resulting in cracked lenses, burned cutting heads, and downtime costing thousands of dollars.
Therefore, a standard workshop compressor cannot be directly connected to a laser machine. A specialized Screw Compressor with Integrated Air Dryer Package must deliver air quality compliant with ISO 8573-1:2010 quality classes:
| Contaminant Parameter | General Factory Air | Required for Laser Cutting (Class 1.2.1) | Honest Compressor Integrated Solution |
|---|---|---|---|
| Solid Particulates | Class 4 (≤ 5 μm) | Class 1 (≤ 0.01 μm) | 5-Stage Progressive Ceramic & Micro-Fiber Filters (≤ 0.01 μm) |
| Pressure Dew Point (Moisture) | +10°C (Class 6) | Class 2 (-40°C) to Class 4 (+3°C) | High-Performance Refrigerant Dryer (+2°C to +3°C) / Desiccant (-40°C) |
| Total Oil Content (Aerosol + Vapor) | ≥ 5.0 mg/m³ (Class 4) | Class 1 (≤ 0.01 mg/m³) / Class 0 | Dual Active Carbon Adsorber + Oil-Vapor Separator (≤ 0.003 mg/m³) |
| Operating Pressure Range | 6 – 8 bar | 16 – 30 bar (Stable) | Dedicated 16 bar / 20 bar / 30 bar Booster & Twin-Screw Systems |
Comprehensive Application Scenarios in Sheet Metal Fabrication
Our screw compressors with air dryers are optimized across broad manufacturing sectors requiring laser cutting assist gas:
- Stainless Steel Cutting (0.8mm to 6mm): Dry air cutting provides high-speed processing with minimal yellowing on edge profiles, suitable for kitchenware, elevator cabs, and architectural metalwork.
- Carbon Steel / Mild Steel (1mm to 12mm): High-pressure compressed air assist achieves up to 200% faster travel speed than oxygen-assisted cutting on medium-thin gauges without dross or slag adhering to the underside.
- Aluminum Alloy & Brass Fabrication: Prevents oxidation micro-cracking and maintains edge squareness in automotive chassis stamping, lighting components, and electrical enclosures.
- Precision Tube & Pipe Lasers: Provides uninterrupted high-volume purging to blow away spatter inside hollow profiles, ensuring flawless internal pipe cleanliness.
Company Profile – Shanghai Honest Compressor Co., Ltd.
Shanghai Honest Compressor Co., Ltd. is a British-owned enterprise founded in early 2004. The modern production address is located at NO. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, China. It is a premier large-scale manufacturing enterprise specializing in the production of twin-screw air compressors in China, while serving as a strategic supplier of complete industrial air system solutions.
We provide various types of piston air compressors (low pressure, medium pressure, high pressure, oil-free air compressors), screw air compressor systems (3kW–480kW various screw air compressors, gas separation equipment, refrigerant compressors, cold dryers, filters, ceramic membrane filtration systems) and comprehensive equipment accessories and consumables.
We fully implement strict management throughout the entire manufacturing process, strictly monitor product quality and environmental protection, and the company has passed ISO9001:2015 quality management system certification.
We pay attention to market trends in technology research and development, close to user requirements, actively absorbing the advantages of leading domestic and international brand performance structures while integrating our own features of convenient maintenance. Our air compressors feature superior structural integrity, unmatched reliability, and outstanding energy saving. Certified by the National Compressor Inspection Center, our energy consumption benchmarks surpass national energy-saving standards.
Nationwide & Global Service Infrastructure
In order to facilitate rapid communication, we operate a direct customer service hotline with factory-trained engineers across major cities.
Complete Compressed Air Equipment & System Portfolio
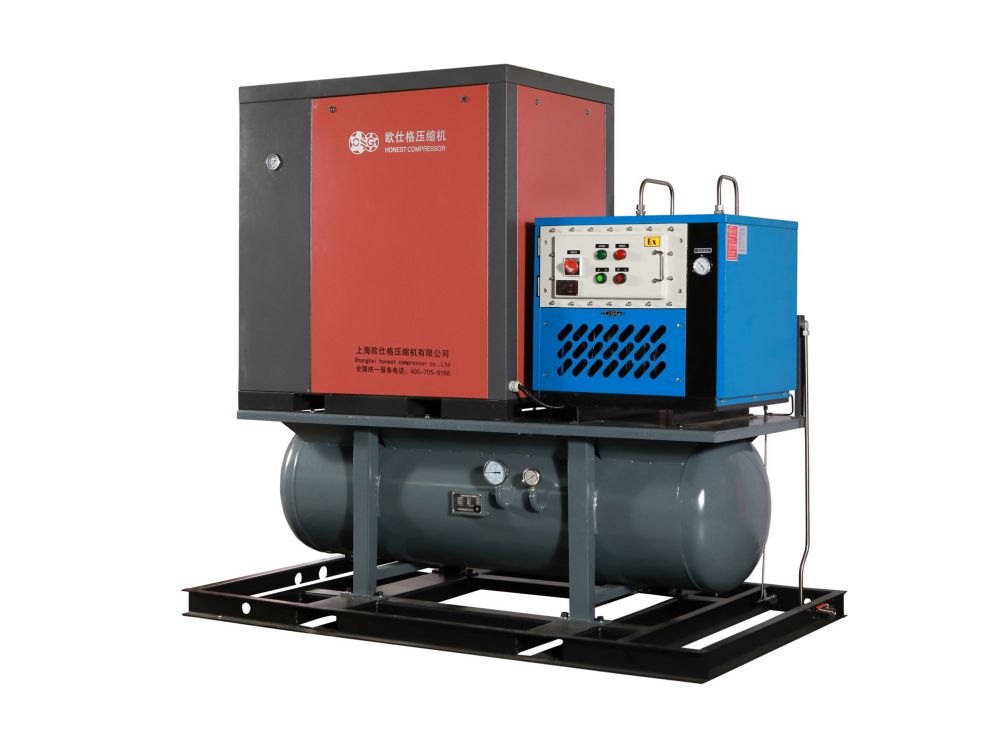
Explore our comprehensive lineup of energy-saving twin-screw compressors, variable speed drives, oil-free units, vacuum pumps, and integrated laser cutting air stations.
Engineering FAQ: Selecting the Ideal Screw Compressor & Air Dryer for Laser Cutters
1. What pressure rating should I select for my fiber laser machine?
For standard sheet metal fabrication up to 3mm thickness, a 16 bar system is typically sufficient. For thicker carbon steel and stainless steel plates (4mm to 16mm) processed on 6kW to 20kW lasers, a 20 bar to 25 bar screw compressor ensures sufficient kinetic purge velocity to evacuate heavy molten dross from the narrow cut kerf without leaving bottom slag.
2. Why is an integrated 4-in-1 laser cutting air compressor preferred over separated components?
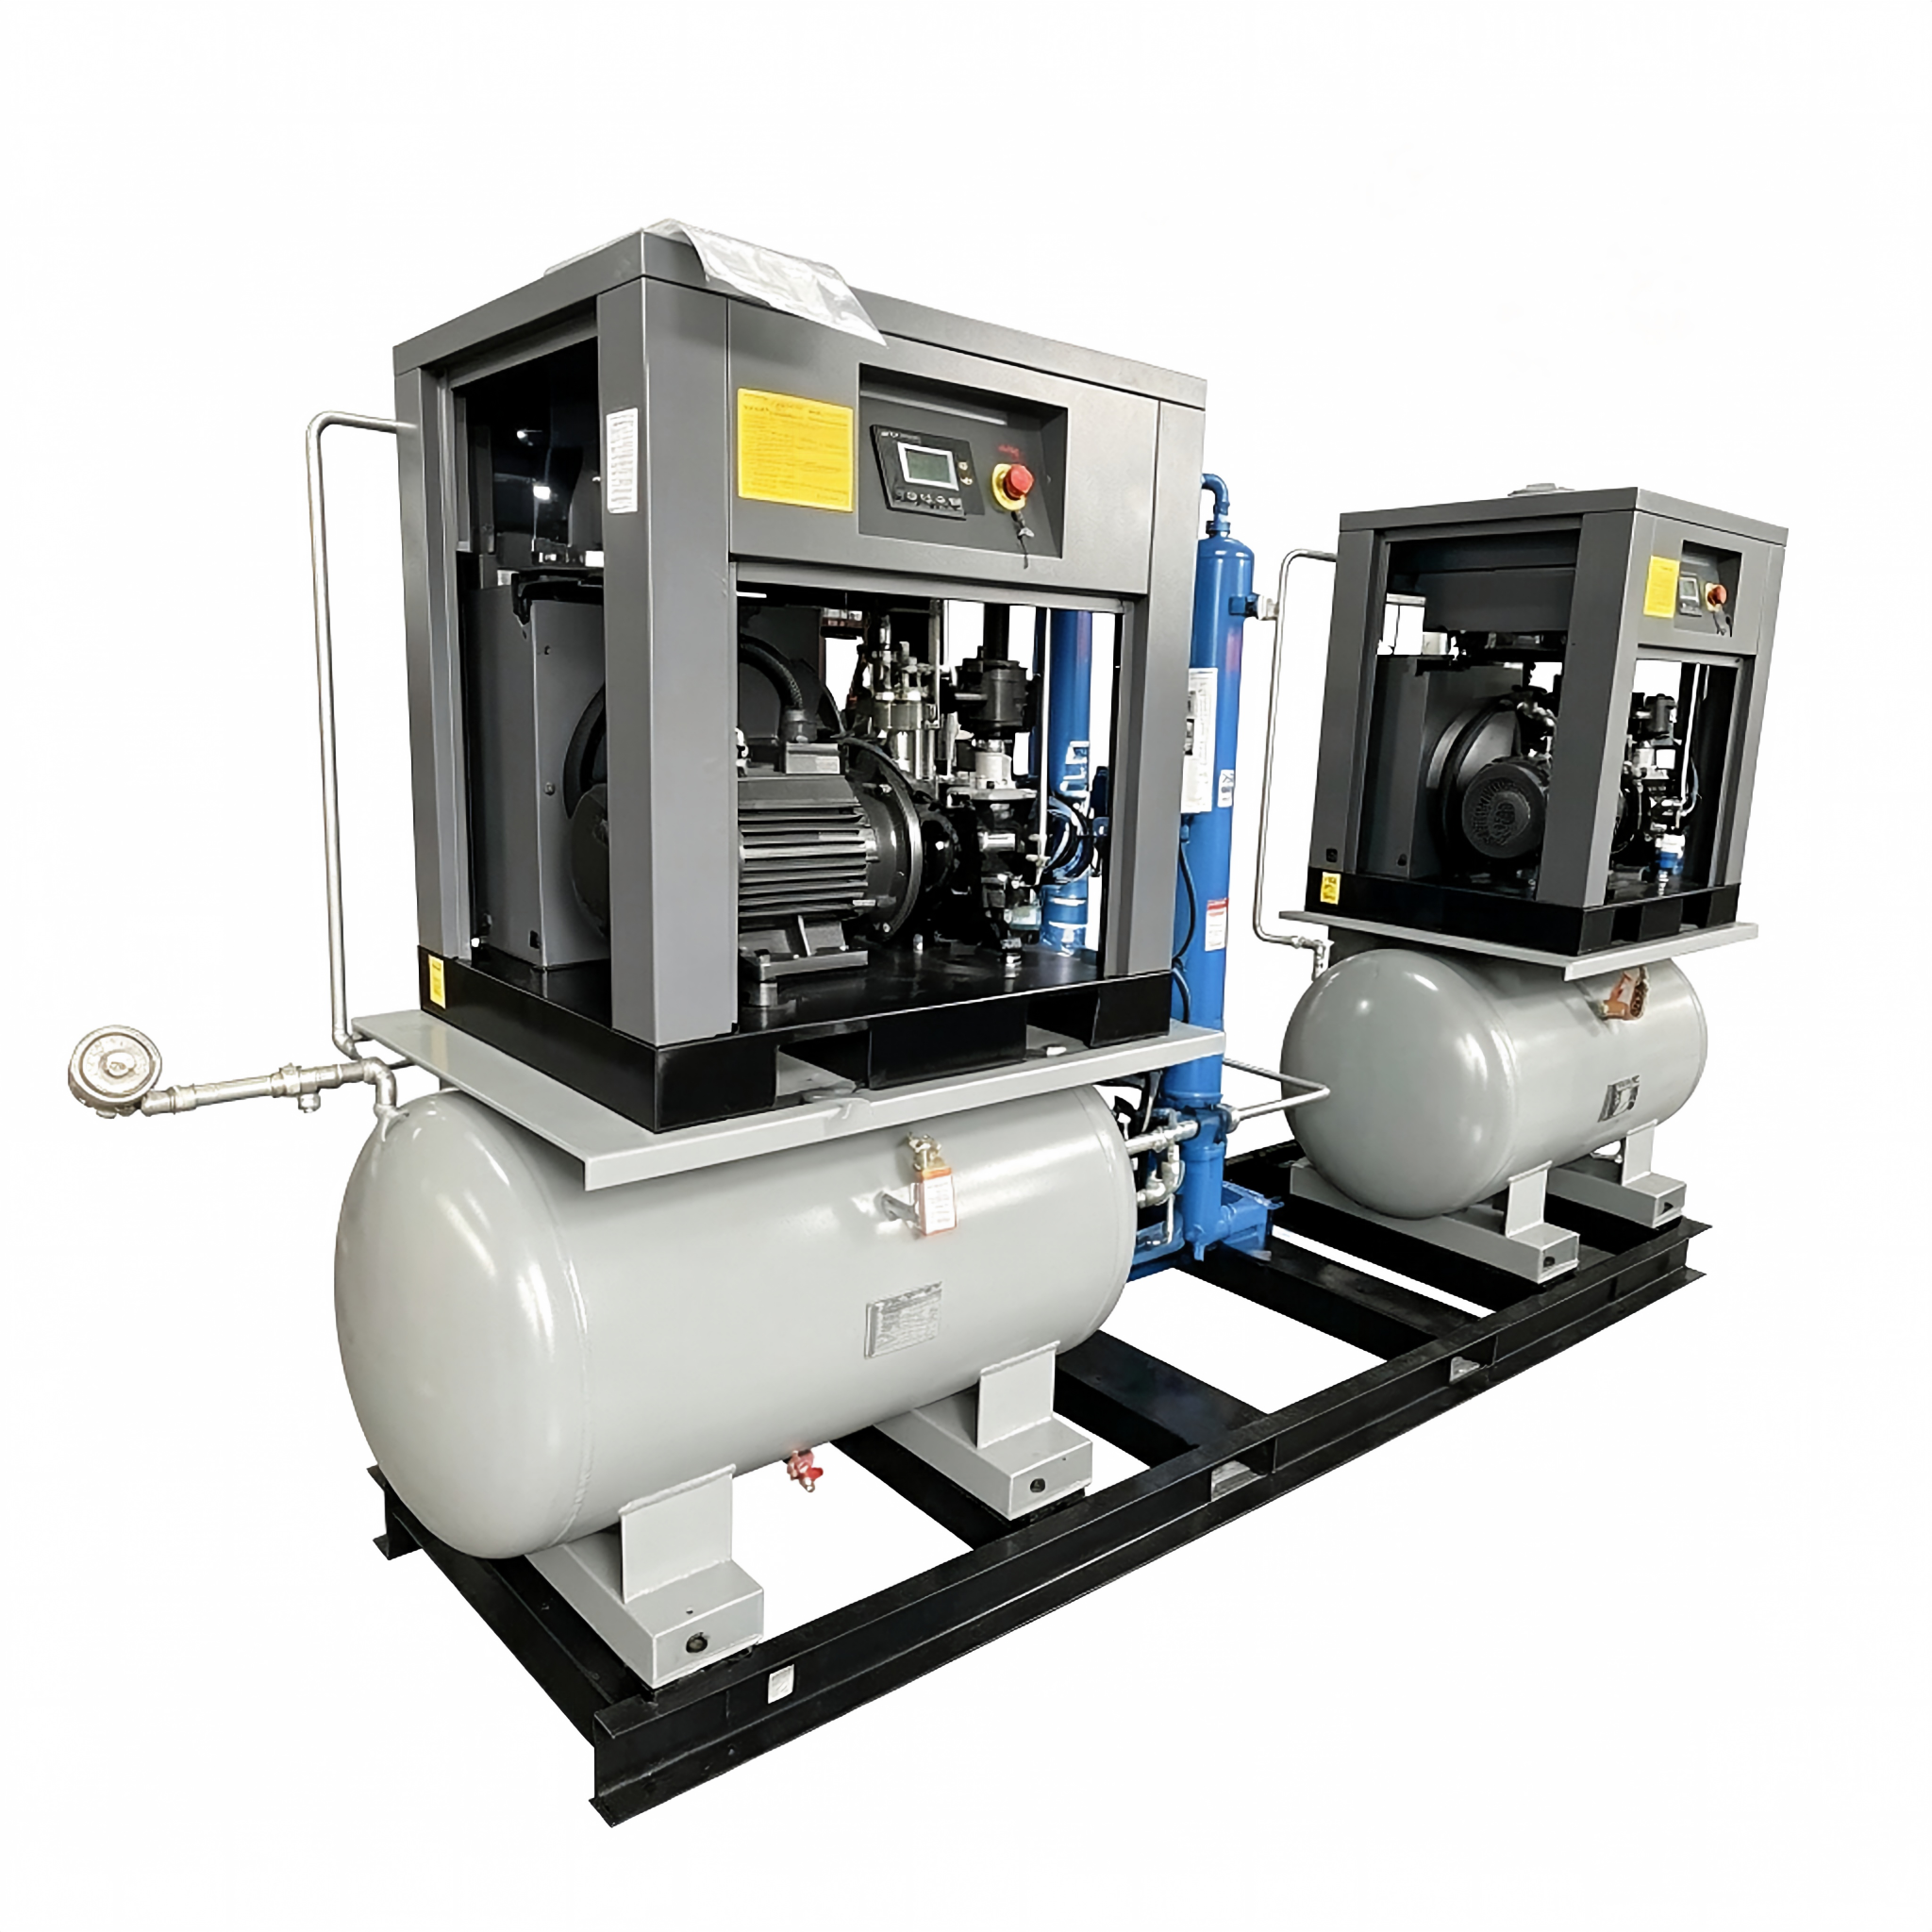
A 4-in-1 laser compressor integrates the twin-screw compressor, permanent magnet VFD motor, large-capacity storage tank, refrigerated air dryer, and 5-stage precision filtration into a single compact chassis. This eliminates complex field piping, minimizes pressure loss between components, reduces footprint by over 60%, and ensures pre-calibrated dew-point and purity monitoring right out of the box.
3. How does variable frequency drive (VFD) technology save energy during laser cutting operations?
Laser cutting involves continuous loading, unloading, rapid positioning, and sheet replacement cycles where gas consumption fluctuates dynamically. A Permanent Magnet Variable Frequency Drive (PM VFD) screw compressor adjusts rotational air-end speed in real-time to match instantaneous gas flow requirements, completely eliminating no-load idling energy waste and delivering 30% to 45% annual electrical power savings.