

Featured Compressors for CNC & Advanced Metal Fabrication
Deploying heavy-duty rotary screw compression to stabilize tool changers, pneumatics, and laser assist gas lines.
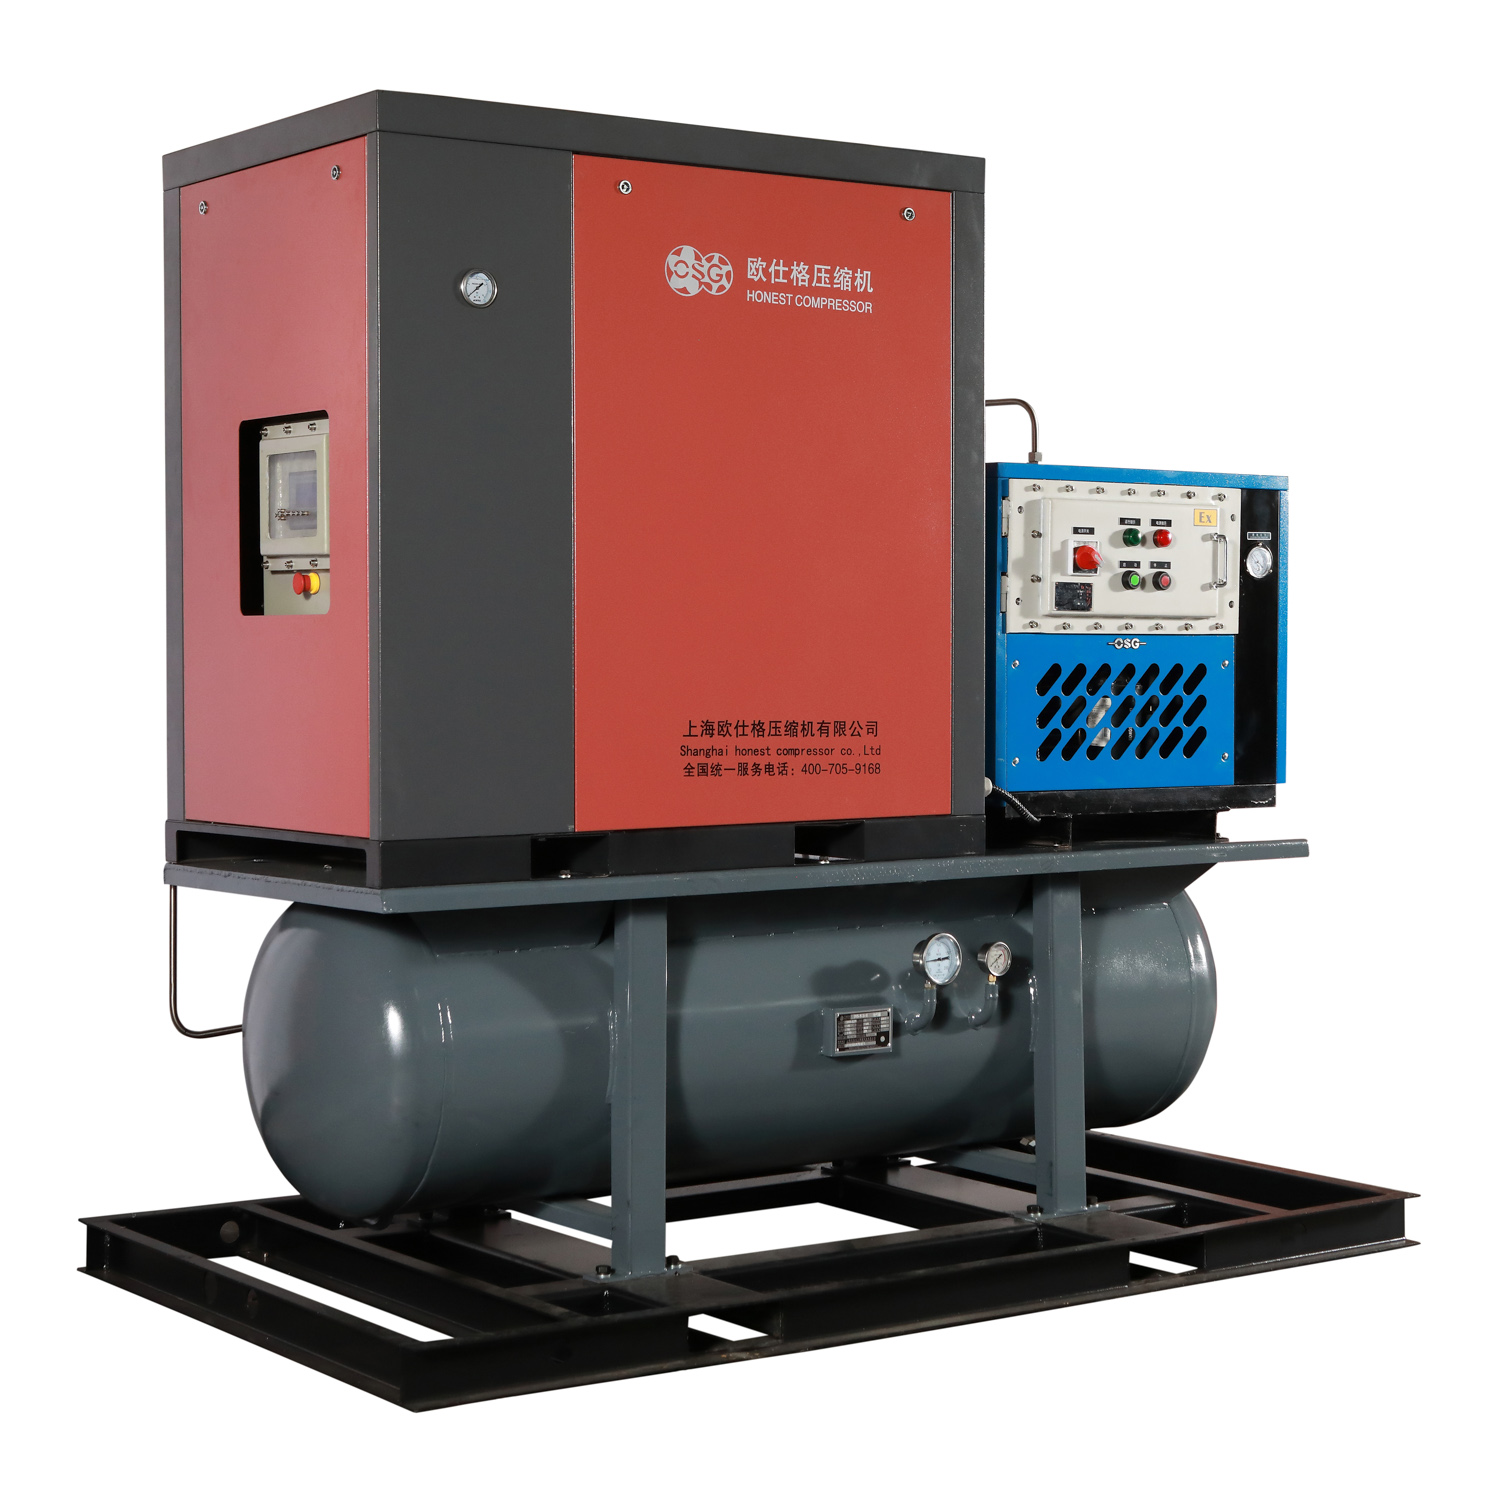
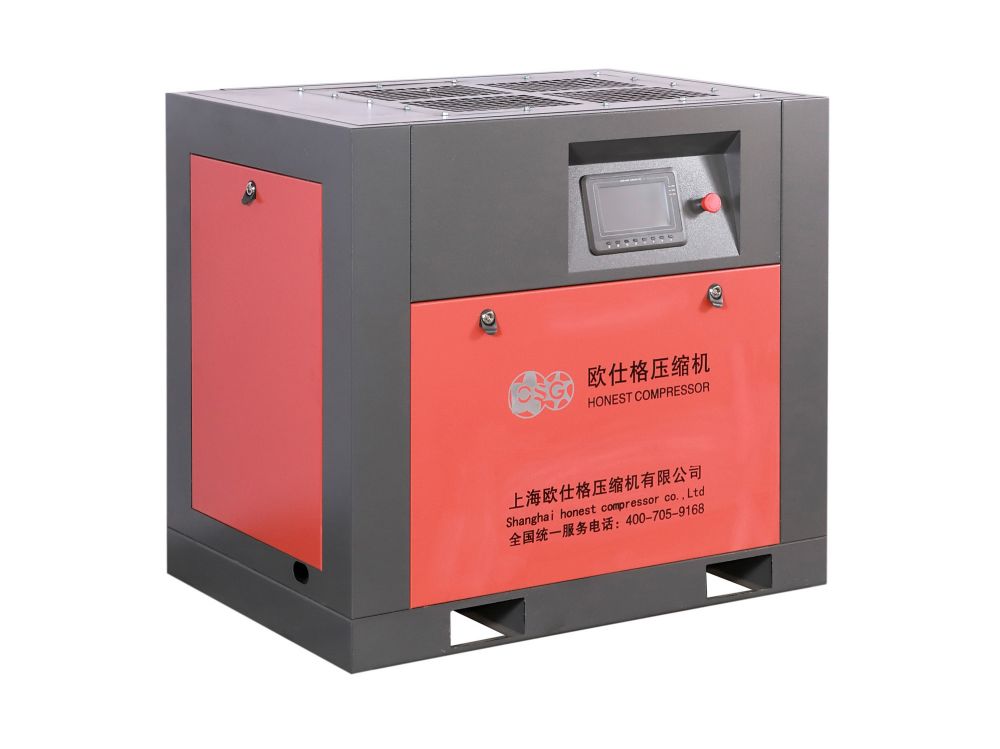
The Strategic Role of Single-Stage Screw Compressors in Modern CNC Ecosystems
Analyzing the paradigm shift toward smart factory integration, micro-tolerance automation, and energy-optimized pneumatics.
Compressed Air as the Fourth Utility in Precision Manufacturing
In the contemporary landscape of high-speed CNC machining centers, automated multi-axis milling, progressive sheet metal stamping, and fiber laser cutting, compressed air has evolved from an auxiliary utility into an indispensable kinetic and atmospheric element. Metalworking facilities operate in hostile thermal and acoustic environments where continuous cycle reliability directly dictates production yields, tool life, and surface finish tolerances.
A single-stage screw air compressor delivers continuous volumetric flow at consistent working pressures (typically ranging from 0.7 to 1.3 MPa / 7 to 13 bar) without the cyclic pressure pulsations characteristic of reciprocating piston compressors. This steady delivery eliminates pressure-drop-induced stalling in automated pneumatic chucks, indexers, and rapid Automatic Tool Changers (ATC), effectively neutralizing the threat of catastrophic tool collisions during high-RPM operations.
Key Manufacturing Demands
100% Continuous Duty Cycle: Unlike piston units that require cool-down intervals, single-stage screw air-ends sustain 24/7 non-stop operations under full load.
Clean, Dry Air Delivery: Integrated refrigeration dryers and dual coalescing filters eliminate moisture condensation within optical paths, high-speed spindles, and pneumatic solenoids.
Variable Speed Energy Optimization: PM VFD drives modulate rotational rotor speed to precisely match instantaneous air consumption from fluctuating CNC work shifts.
Technical Superiority of Single-Stage Screw Compression in CNC Operations
Designed for thermal resilience, volumetric efficiency, and harmonic stability across demanding machining shifts.
Asymmetric 5:6 Rotor Profile
Precision-ground male and female helical rotors mesh smoothly with minimal blow-hole clearance. The optimized 5:6 tooth ratio balances radial loads, lowers specific power consumption (kW/m³/min), and yields ultra-low mechanical vibration below 65 dB(A), protecting sensitive CNC probing instruments.
Permanent Magnet Oil-Cooled VFD
IE4/IE5 ultra-high-efficiency permanent magnet motors maintain 96%+ motor efficiency even under partial load profiles (25%-100% capacity). The integrated liquid-oil cooling architecture protects stator windings against the harsh ambient thermal spikes typical in heavy metalworking shops.
Intelligent PLC & IoT Monitoring
Integrated microcomputer controllers continuously monitor discharge temperature, pressure differentials, oil separation performance, and motor thermal health. RS-485 Modbus and cloud IoT connectivity interface seamlessly with centralized CNC plant SCADA and MES systems.
How Single-Stage Screw Compressors Drive Critical Metal Processing Workflows
From high-speed spindle positive air sealing to high-pressure fiber laser cutting assist systems.
1. CNC High-Speed Spindle Air Purge & Bearing Labyrinth Sealing
High-frequency electro-spindles rotating between 15,000 RPM and 60,000 RPM are exceptionally vulnerable to coolant mist, fine metallic dust, and graphite particles. Single-stage screw air compressors supply a constant, pulsation-free air barrier (labyrinth positive pressure purge at 0.15–0.3 MPa). If line pressure fluctuates by even 0.05 MPa, coolant vapor can penetrate the ultra-precision hybrid ceramic bearings, causing thermal seizure and tens of thousands of dollars in spindle replacement costs.
2. Automatic Tool Changer (ATC) Drawbars & Taper Cleaning Air Blasts
During automated tool exchanges on vertical (VMC) and horizontal (HMC) machining centers, pneumatic drawbars actuate tool clamping mechanisms under 0.6–0.8 MPa of force. Simultaneously, a high-velocity localized air blast sweeps through the spindle spindle taper (BT30, BT40, BT50, or HSK-A63) to evacuate microscopic chips before the new toolholder seats. Clean, moisture-free compressed air prevents runout errors, tool misalignment, and surface chatter on machined workpieces.
3. Minimum Quantity Lubrication (MQL) & Continuous Chip Evacuation
Near-dry machining (MQL) utilizes aerosolized micro-droplets of biodegradable cutting oil suspended in a high-velocity compressed air stream. The single-stage screw compressor provides stable, dry carrier air to aerosol nozzles positioned directly at the cutting edge. This accelerates thermal dissipation, prolongs carbide insert life, and clears heavy swarf out of deep pockets during titanium, stainless steel, and aerospace alloy milling.
4. Assist Gas Supply for High-Precision Fiber Laser Cutting
In sheet metal fabrication, high-pressure compressed air (1.6–2.0 MPa using integrated booster systems or high-pressure screw packages) serves as a cost-effective assist gas alternative to liquid nitrogen or oxygen for cutting stainless steel, aluminum alloys, and mild steel up to 6mm thickness. Single-stage screw units deliver continuous high volumetric flow rates, cooling the focal zone, blowing molten slag downward, and producing clean, dross-free edges ready for immediate robotic welding.
5. Automated Pneumatic Clamping, Indexers & Robotic Loading Gantries
Lights-out manufacturing facilities rely on compressed air to drive zero-point clamping systems, pneumatic vises, rotary indexing tables, and vacuum/pneumatic grippers on 6-axis loading robots. A steady, uninterrupted air supply guarantees uniform clamping tonnage, eliminating workpiece slippage during heavy roughing cuts and ensuring positional repeatability within ±2 micrometers.
| Operational Metric | Single-Stage Screw Compressor (Honest PM VSD) | Traditional Piston / Reciprocating Compressor | Multi-Stage Heavy Industrial Compressor |
|---|---|---|---|
| Duty Cycle Capability | 100% Continuous (Non-Stop 24/7 CNC Shifts) | 50% - 60% Intermittent (Prone to Thermal Derating) | 100% Continuous (Designed for >132kW Base Loads) |
| Pressure Stability | ±0.01 MPa Dynamic Modulation | ±0.15 - 0.25 MPa Wide Cyclic Oscillation | ±0.02 MPa Base-Load Staged Control |
| Noise & Vibration | 62 – 68 dB(A) Smooth Rotary Motion | 80 – 92 dB(A) High Mechanical Shock Waves | 70 – 78 dB(A) Acoustic Enclosure Required |
| Oil Carryover Rate | < 3 ppm (Triple Separator Stage) | > 25 - 50 ppm (Severe Contamination Risk) | < 2 - 3 ppm High-Efficiency Separation |
| Capital & Lifecycle ROI | Lowest TCO for 7.5kW - 75kW Machining Cells | Low Initial Cost, High Maintenance & Downtime | High Initial Capital; Ideal for massive foundry plants |
Achieving ISO 8573-1:2010 Air Purity in Modern Metal Workshops
Preventing water condensation, oil varnishing, and particulate wear across high-value CNC control hardware.
The Critical Impact of Air Contaminants on Machine Tools
Untreated compressed air contains three catastrophic contaminants: water vapor, atmospheric particulates, and residual lubricating aerosols. When compressed air expands inside CNC directional control valves, solenoid manifolds, and linear glass scales, ambient cooling triggers moisture precipitation.
Moisture leads to internal corrosion of pneumatic cylinders, emulsification of spindle grease, and clouding of optical encoders on CMM (Coordinate Measuring Machines). By integrating a single-stage screw air compressor with dedicated refrigerated dryers (providing a pressure dew point of +3°C) and multi-stage 0.01-micron coalescing filtration, manufacturing plants achieve ISO 8573-1:2010 Class [1:4:1] air quality, extending the operational lifespan of machine tool sub-components by over 300%.
Recommended CNC Air Quality Setup
Particulate Filtration: Dual pre-filter (1.0 μm) and high-efficiency sub-micron filter (0.01 μm) to safeguard precision pneumatic orifices.
Moisture Elimination: Integrated cold dryer with automatic zero-loss timed condensate drain valves.
Residual Oil Content: Oil separator element rated for ≤ 2 mg/m³ carryover to prevent varnish build-up on optical glass scales.
Company Profile: Shanghai Honest Compressor Co., Ltd.
Delivering world-class rotary screw engineering and comprehensive industrial compressed air systems since 2004.
British-Owned Engineering Heritage & Global Standard
Shanghai Honest Compressor Co., Ltd. is a British-owned enterprise founded in early 2004. The modern manufacturing facility is strategically located at NO. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, China. As a premier large-scale manufacturing enterprise specializing in the production of twin-screw air compressors in China, we stand as an authoritative turnkey supplier of end-to-end industrial air system solutions.
We engineer and manufacture an extensive portfolio including piston air compressors (low pressure, medium pressure, high pressure, oil-free air compressors), complete screw air compressor systems ranging from 3kW to 480kW, gas separation equipment, refrigerant compressors, cold dryers, precision filters, ceramic membrane filtration systems, and genuine OEM consumables.
We fully implement strict management throughout the entire manufacturing process, strictly monitor product quality and environmental protection, and the company has successfully passed the ISO9001:2015 international quality management system certification.
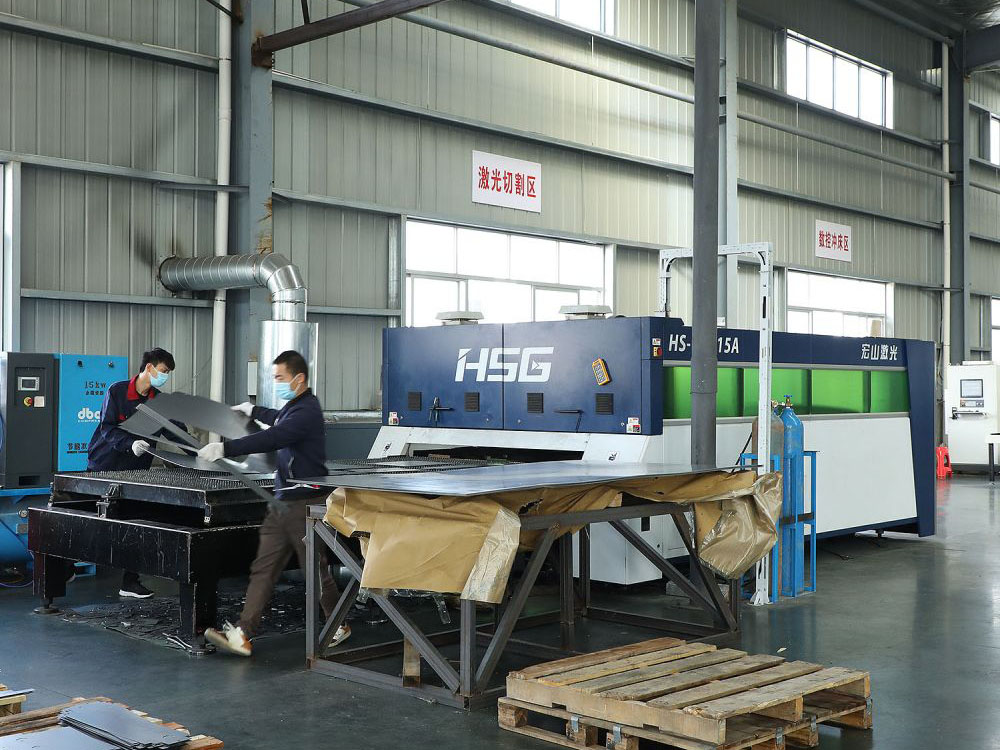
We pay close attention to global market trends in technology research and development, maintaining proximity to the practical needs of industrial users. By actively absorbing the core mechanical advantages of leading domestic and international brand performance structures and integrating our own proprietary design features for effortless maintenance, our compressors achieve superior structural integrity, exceptional performance stability, and remarkable energy savings. After rigorous testing by the National Compressor Inspection Center, our energy consumption metrics consistently outperform national energy-saving benchmarks.
We provide users with comprehensive series spanning 3kW to 480kW in both air-cooled and water-cooled configurations, with flow capacities ranging from 0.5 m³/min to 75 m³/min. Our portfolio encompasses permanent magnet variable frequency (PM VFD) air compressors, 100% oil-free compressors, mobile diesel/electric compressors, and specialized blower systems. Furthermore, we deliver complete turnkey construction plans for air compressor stations, encompassing system design, precision manufacturing, user technical training, preventative maintenance support, and full overhaul management.
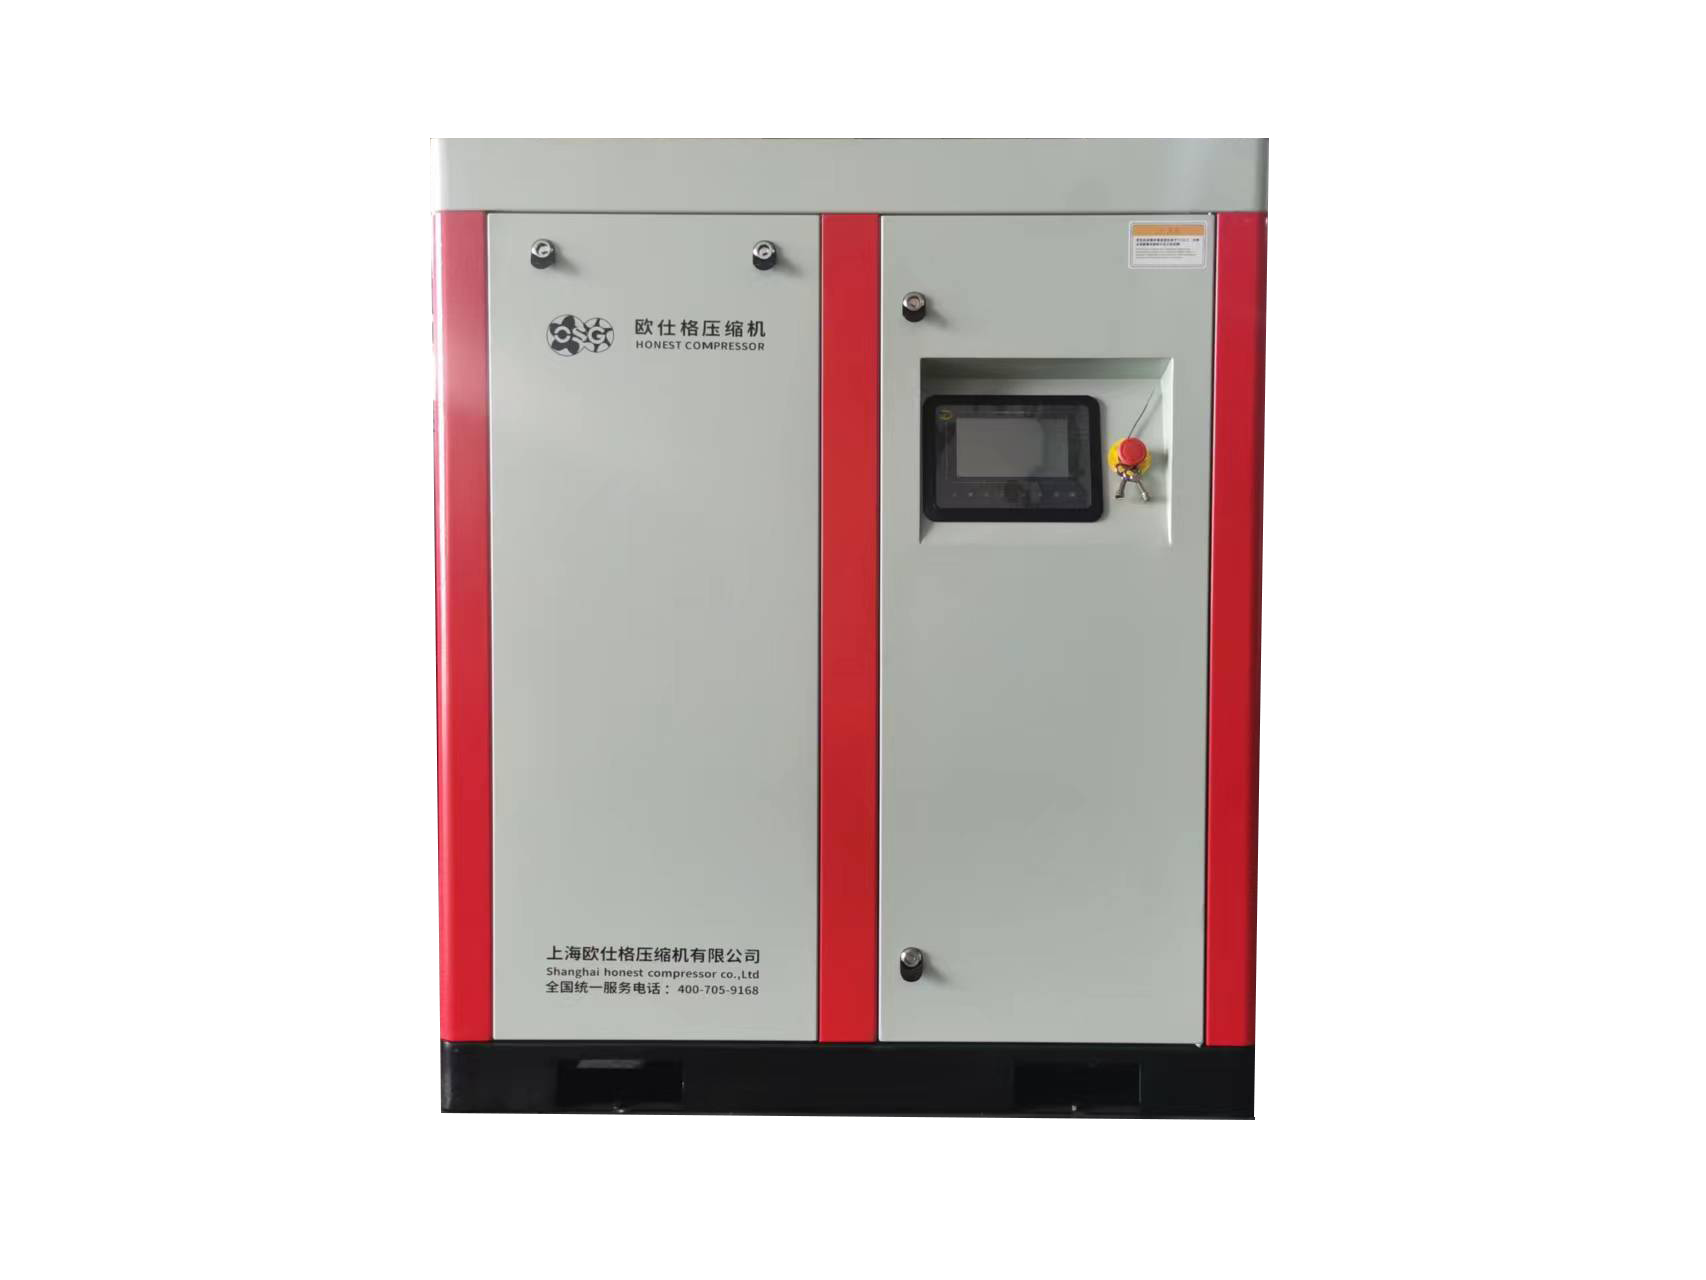
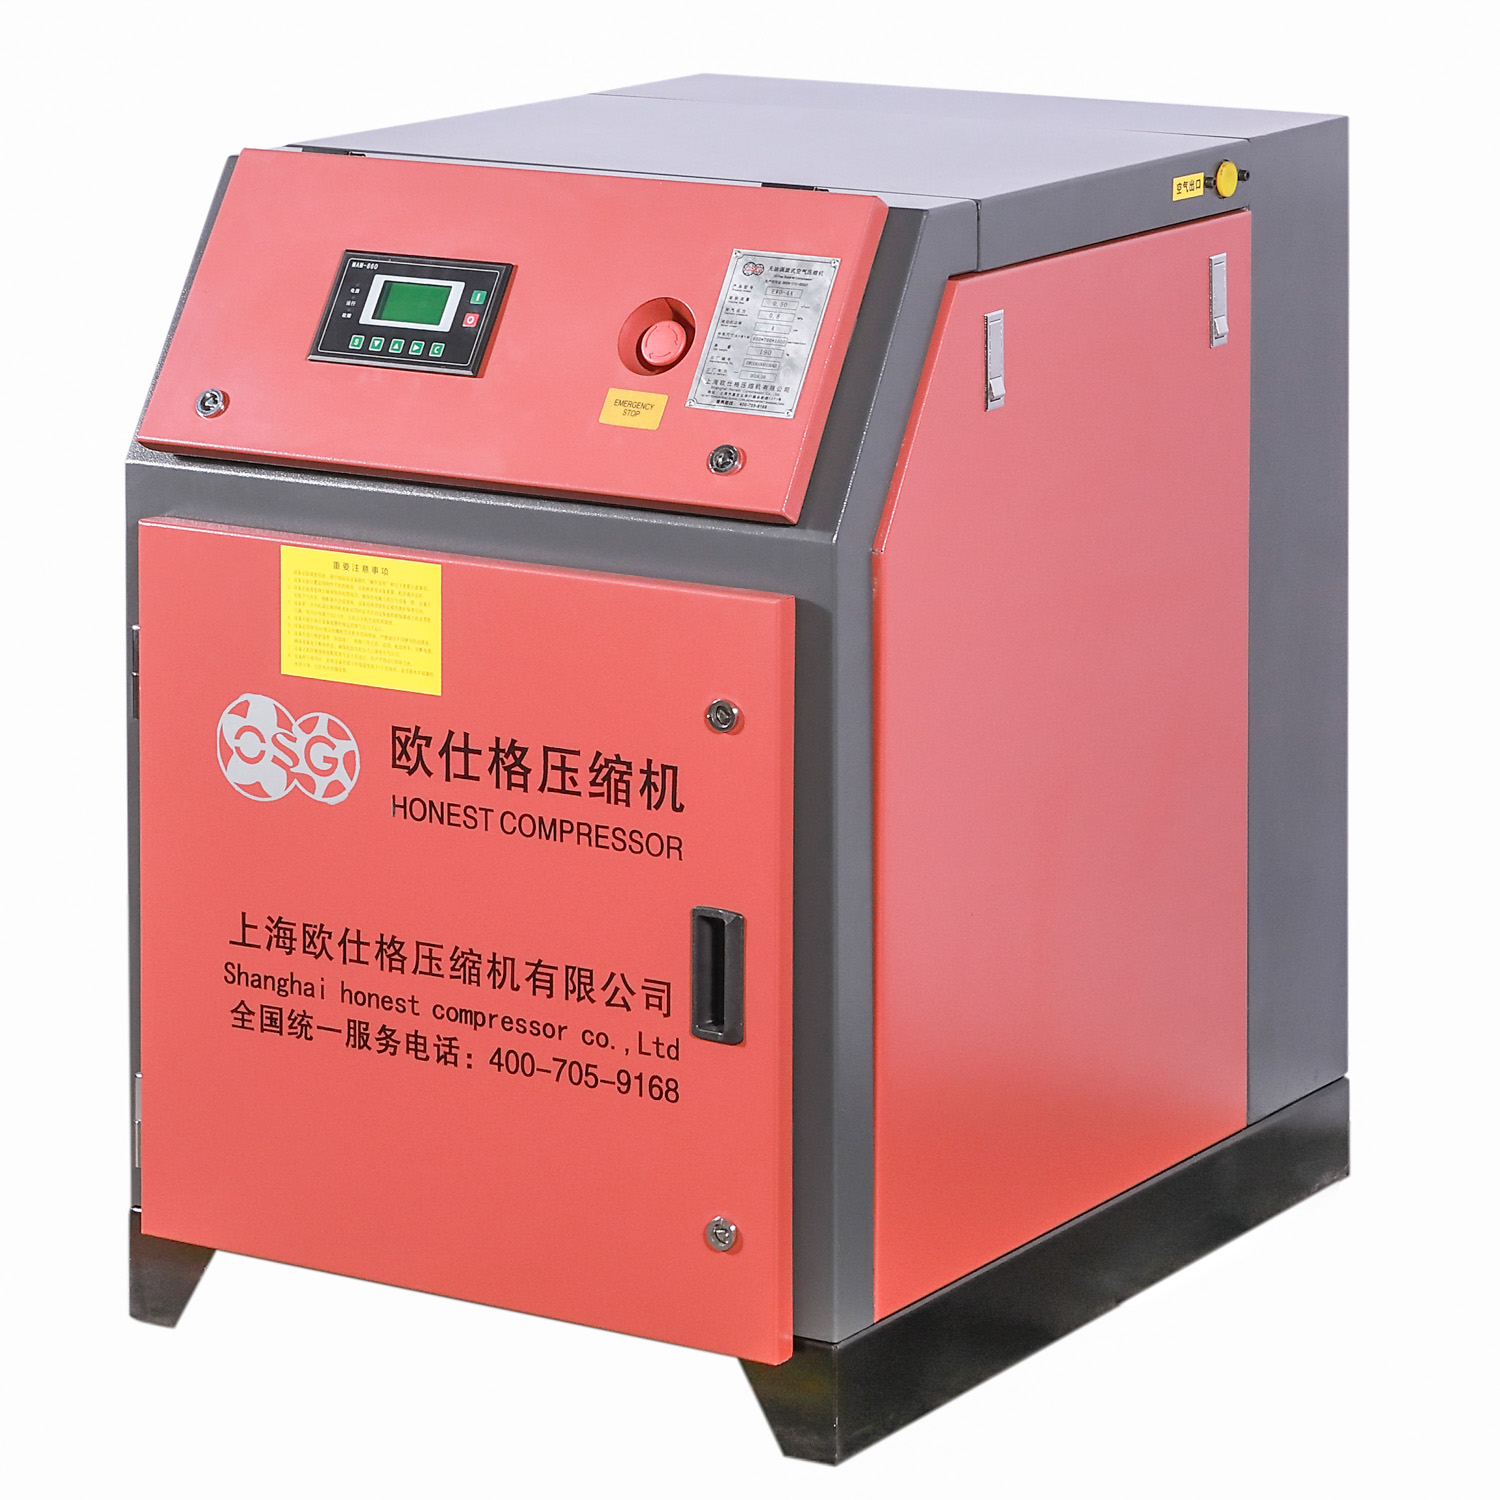
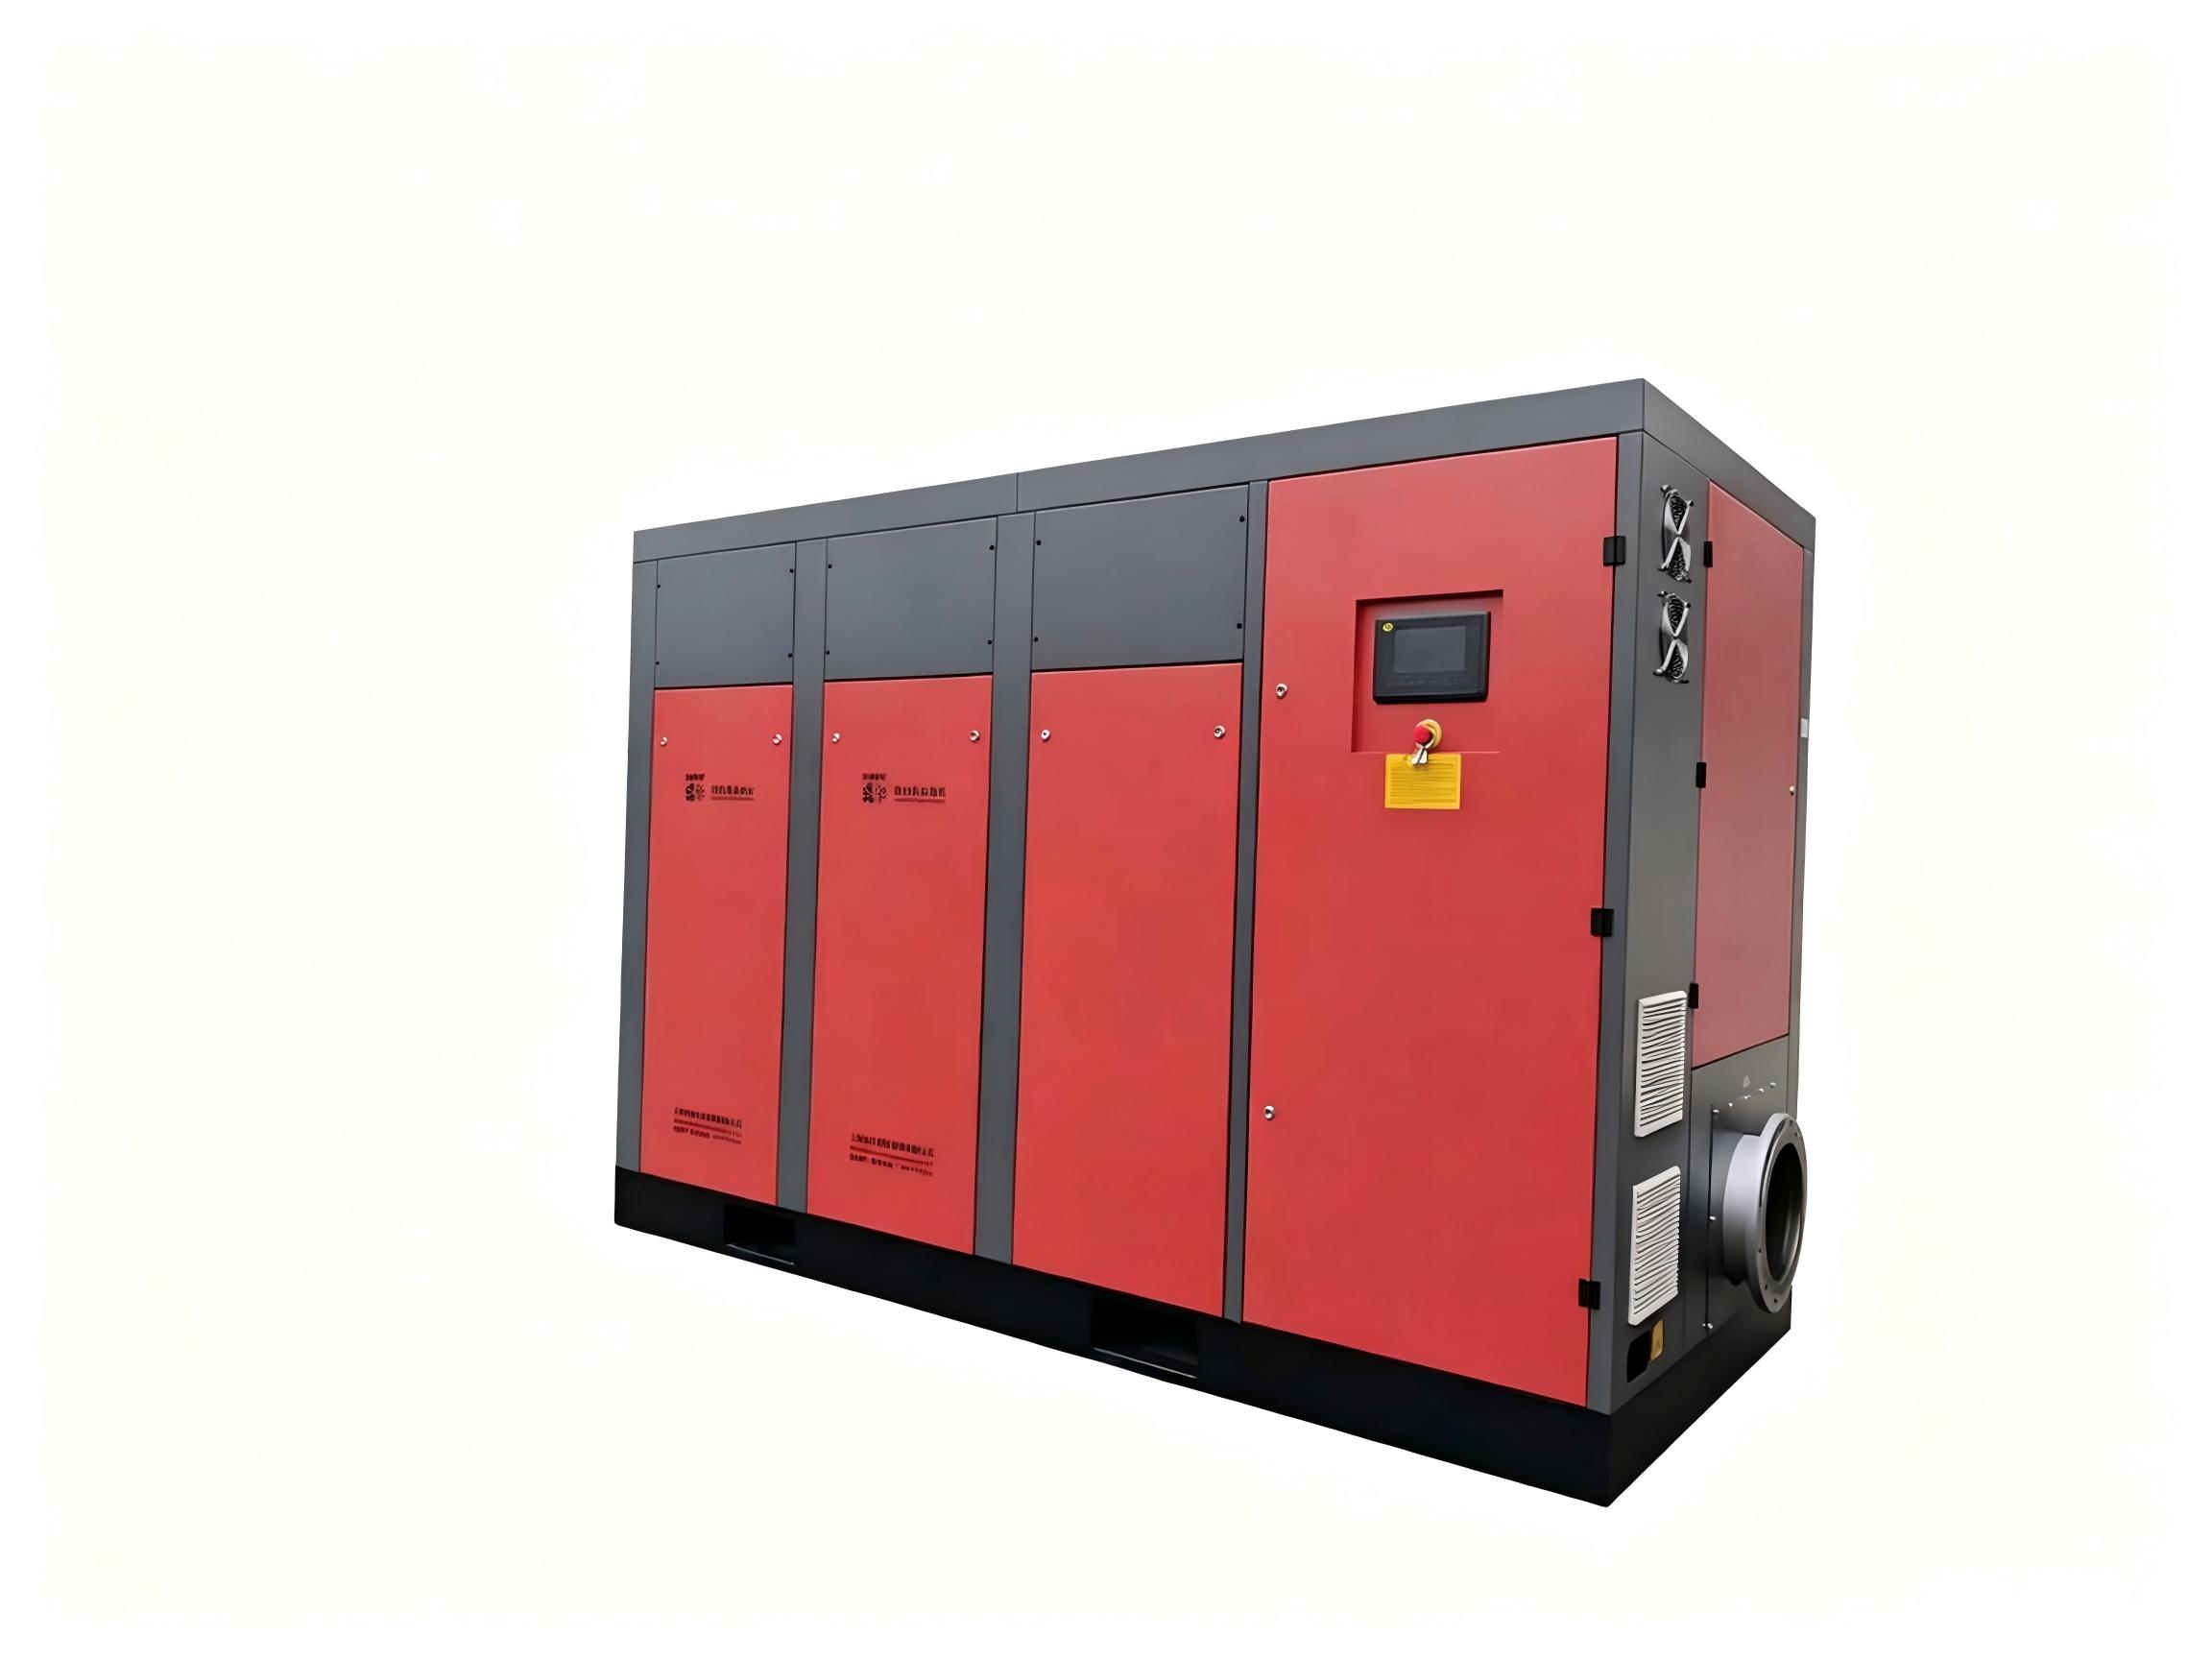
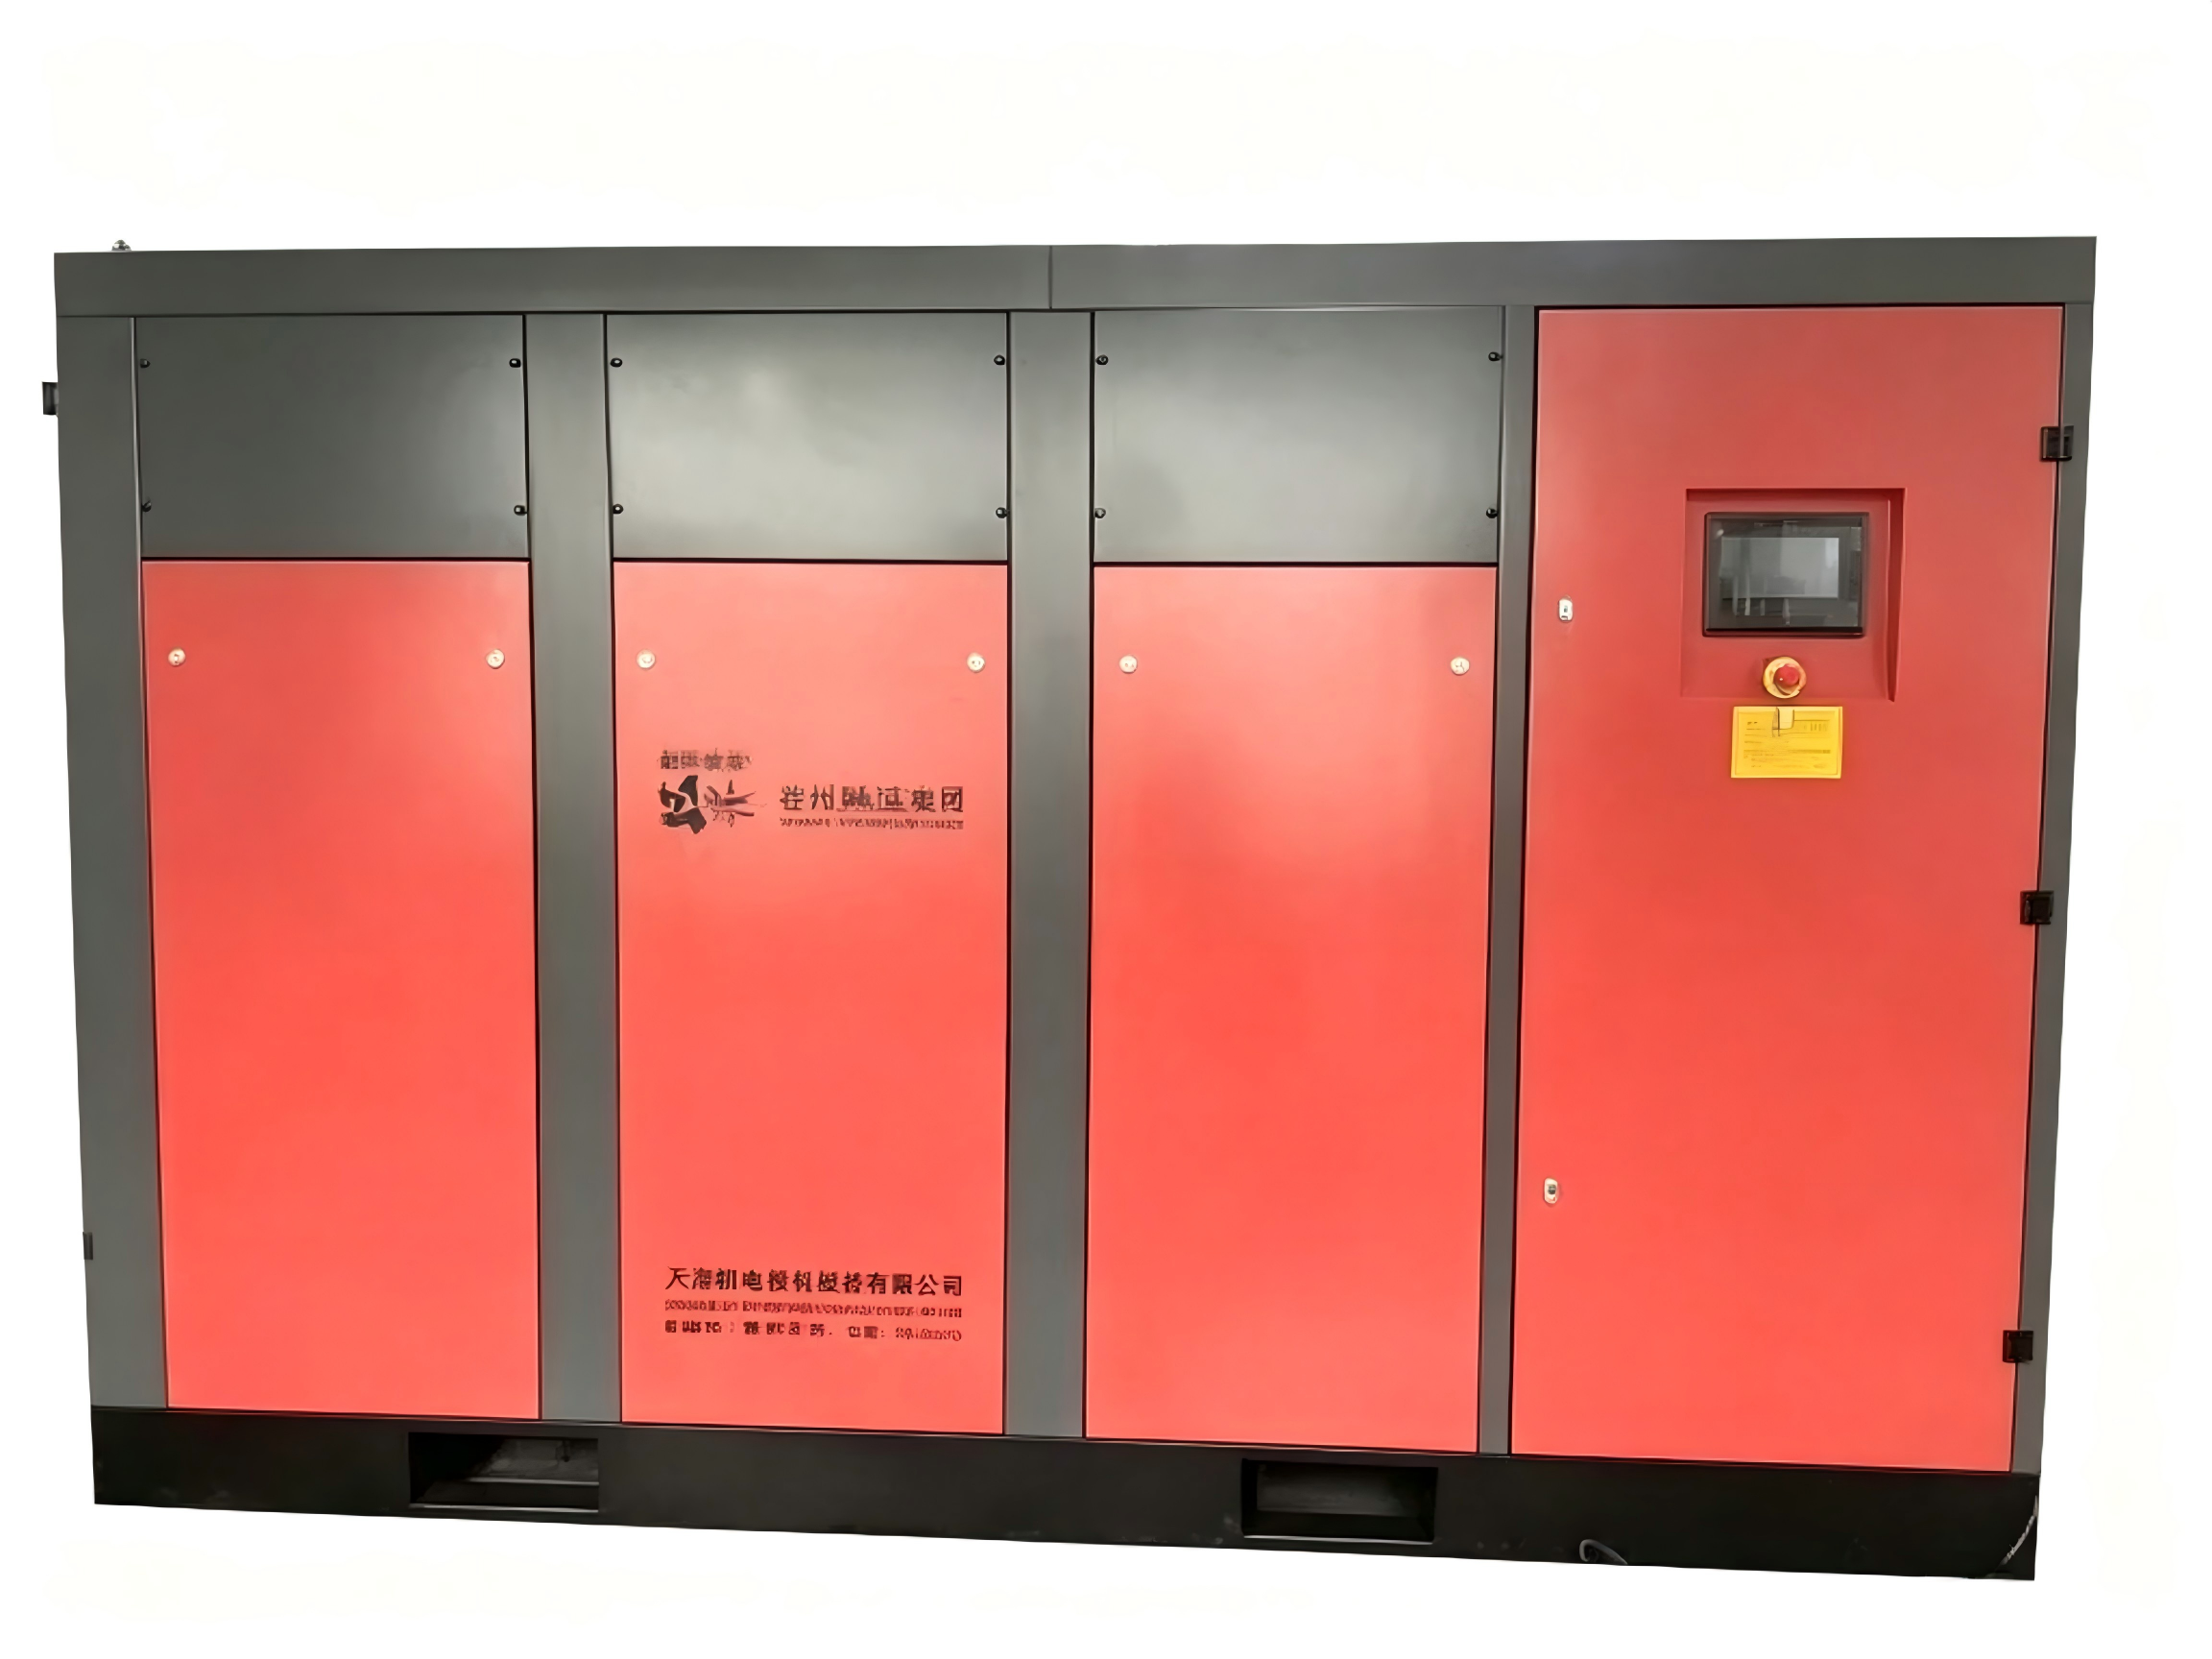
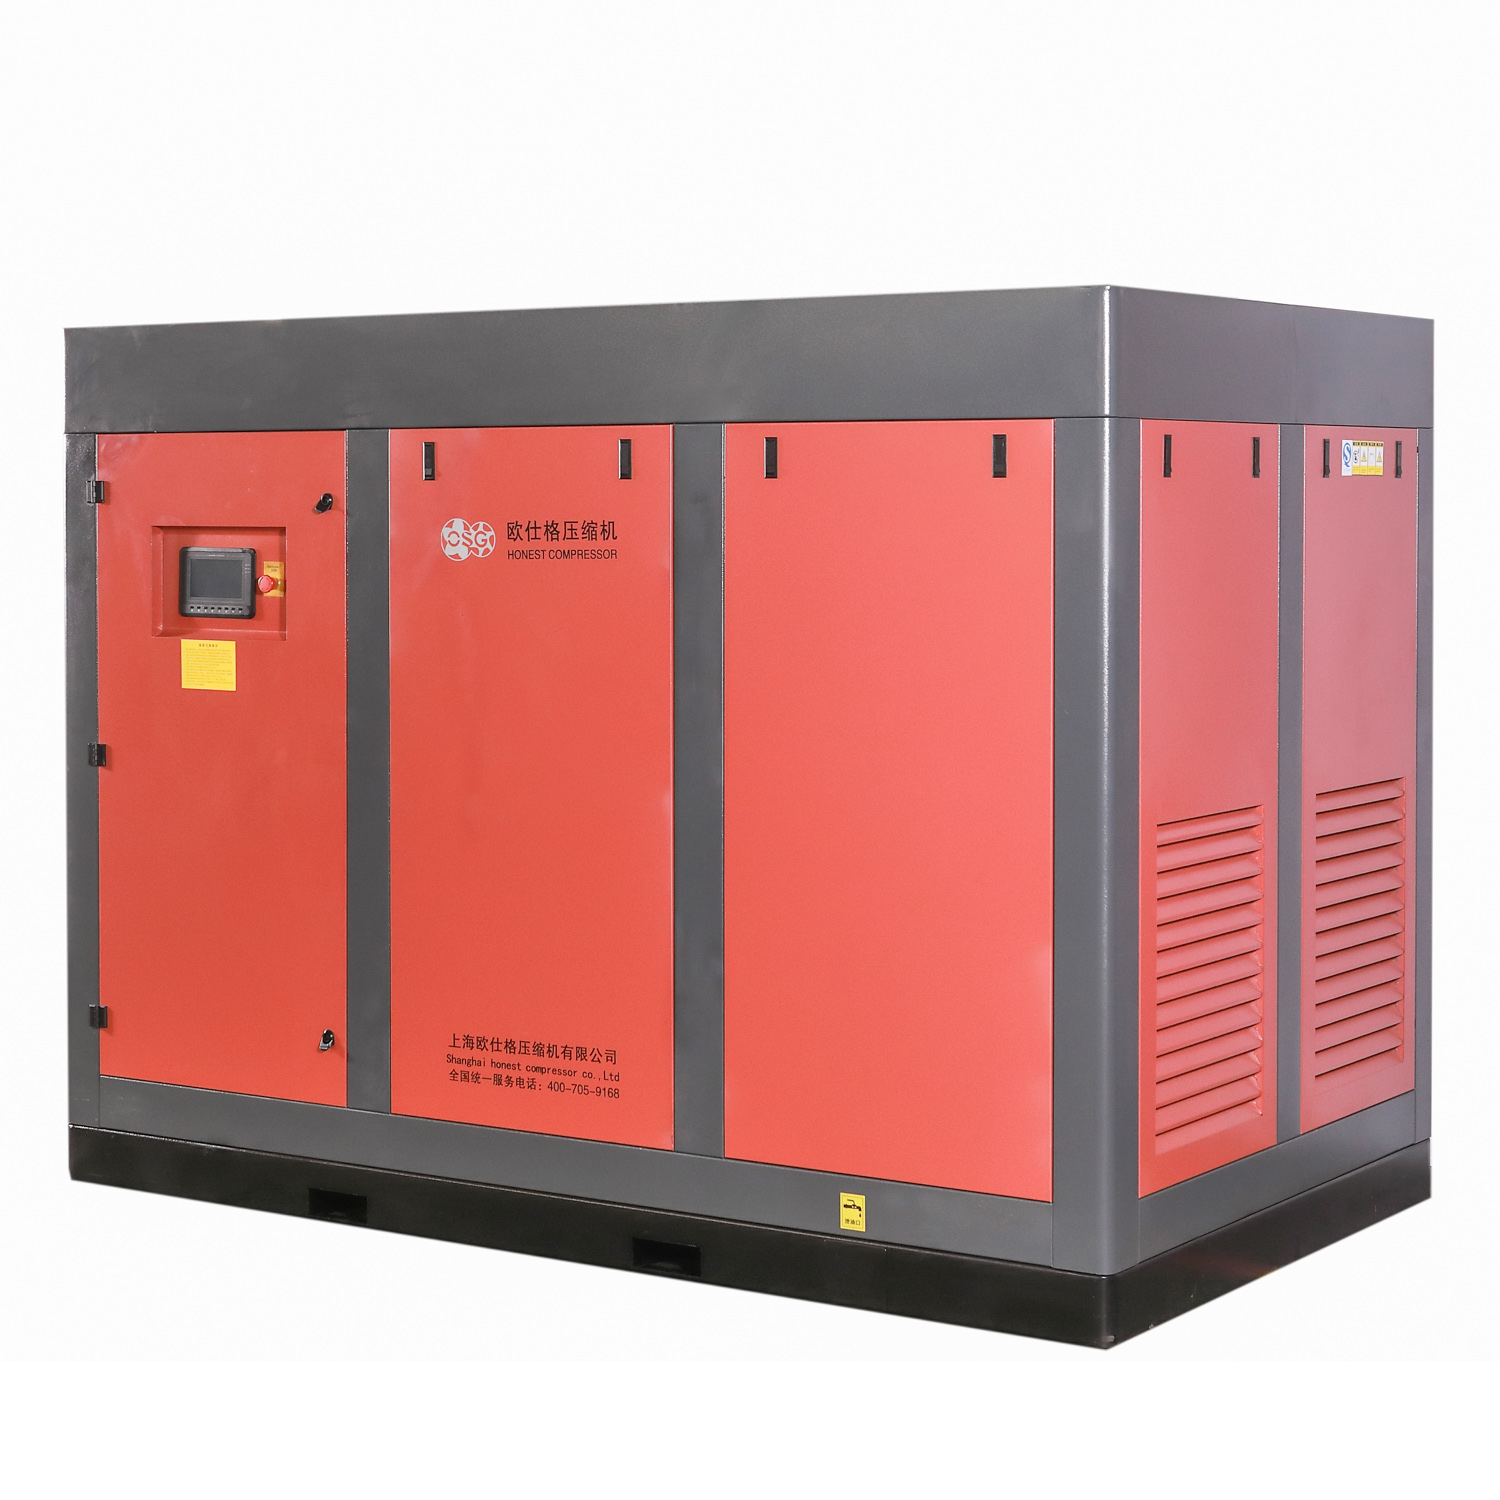
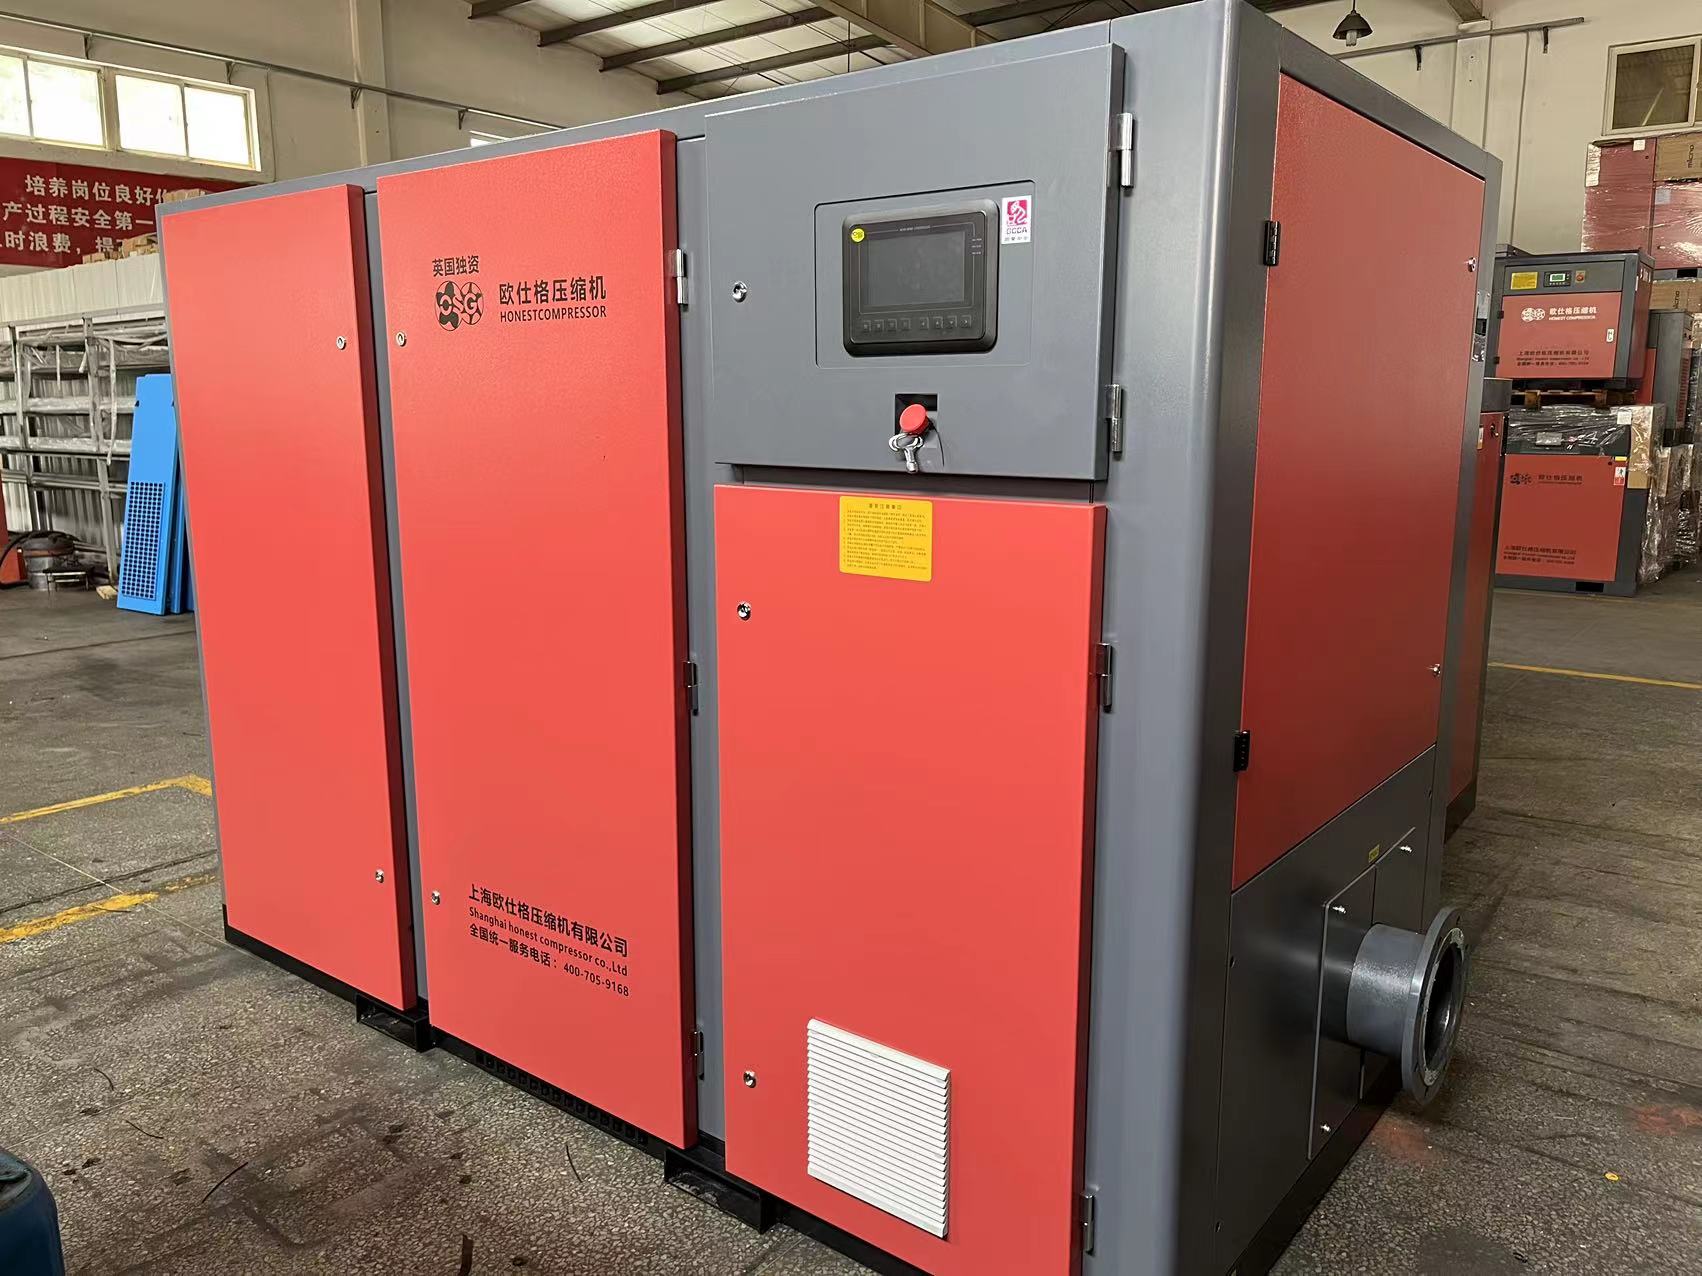
Heavy-Duty Rotary Screw Compressors, Blowers & Vacuum Systems
Engineered for high reliability, ISO certified performance, and long lifecycle efficiency across global metalworking and process industries.
Total Cost of Ownership (TCO) & Compressor Sizing for CNC Facilities
A systematic framework for calculating volumetric demand, mitigating electrical loss, and maximizing operating margins.
Calculating CFM / Flow Rate
Sum the maximum instantaneous air consumption of all connected machine tools: ATC tool changes (approx. 15–25 CFM per burst), continuous spindle air purge (2–4 CFM per spindle), chip clearing air blast (5–10 CFM), and pneumatic fixtures. Multiply by a 1.25 safety/expansion factor to ensure the screw compressor operates comfortably in its optimal 70–85% load zone.
Lifecycle Energy Analysis
Over a standard 10-year operating horizon, electricity accounts for approximately 76% of a compressor's total lifecycle cost, while initial equipment purchase represents only 12%, and maintenance 12%. Upgrading to a permanent magnet variable frequency (PM VFD) single-stage screw compressor cuts off-load idling power losses by up to 35%, generating complete capital payback within 12 to 18 months.
Preventative Maintenance Intervals
Maintain peak adiabatic efficiency through structured service intervals: replace air intake filters every 2,000 operational hours, spin-on oil filter cartridges at 2,000–3,000 hours, and high-efficiency spin-on air/oil separator elements at 4,000 hours. Utilizing genuine synthetic rotary screw lubricant protects precision rotor surfaces against oxidation and thermal varnish buildup.